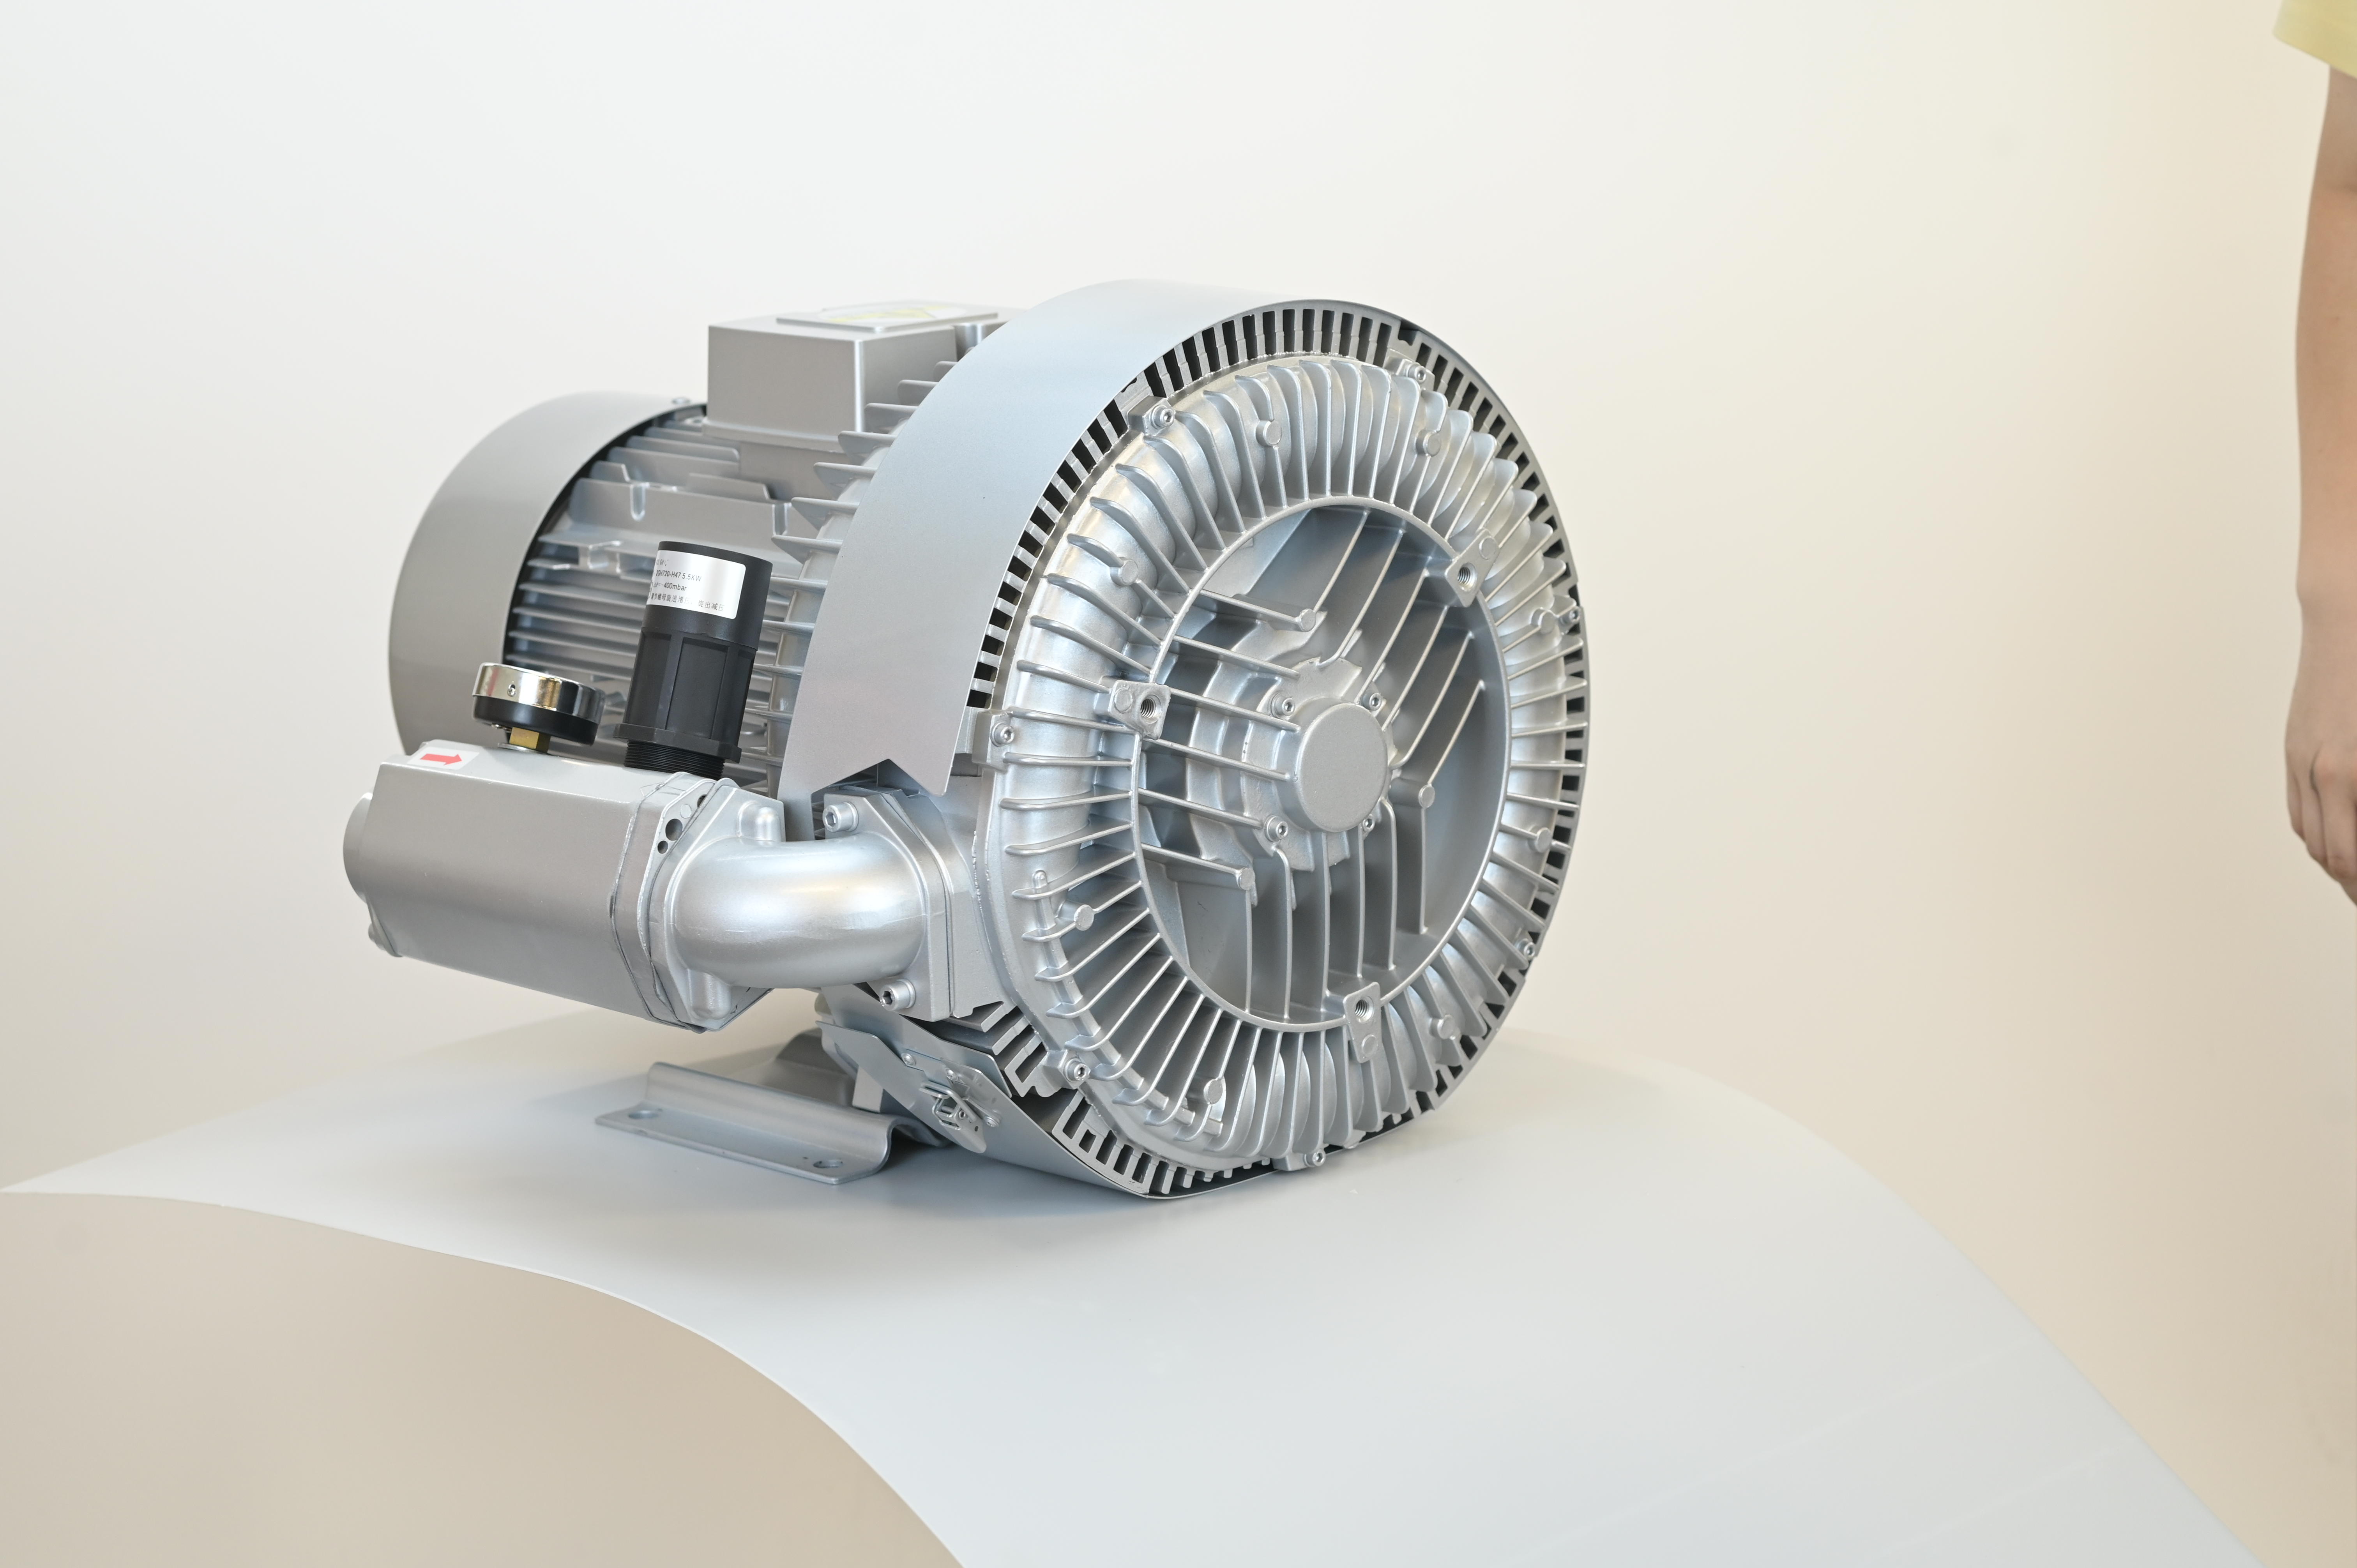
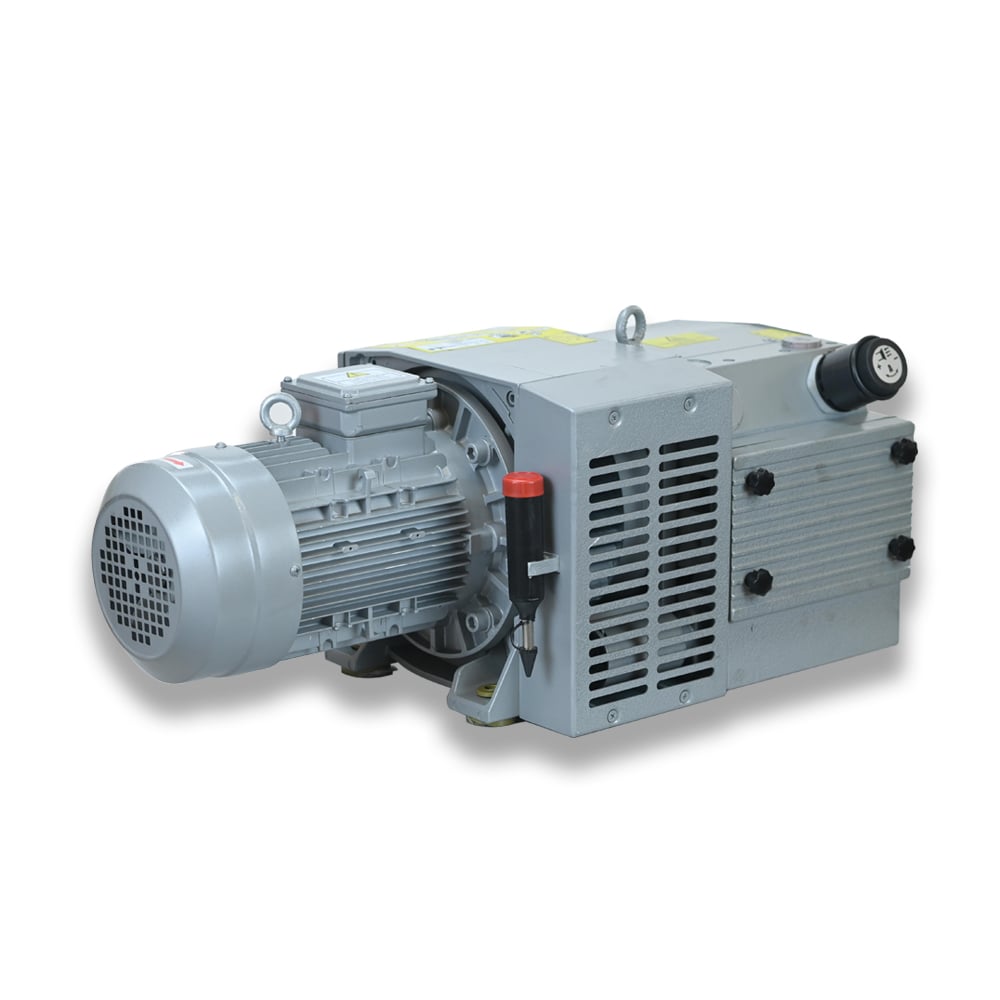
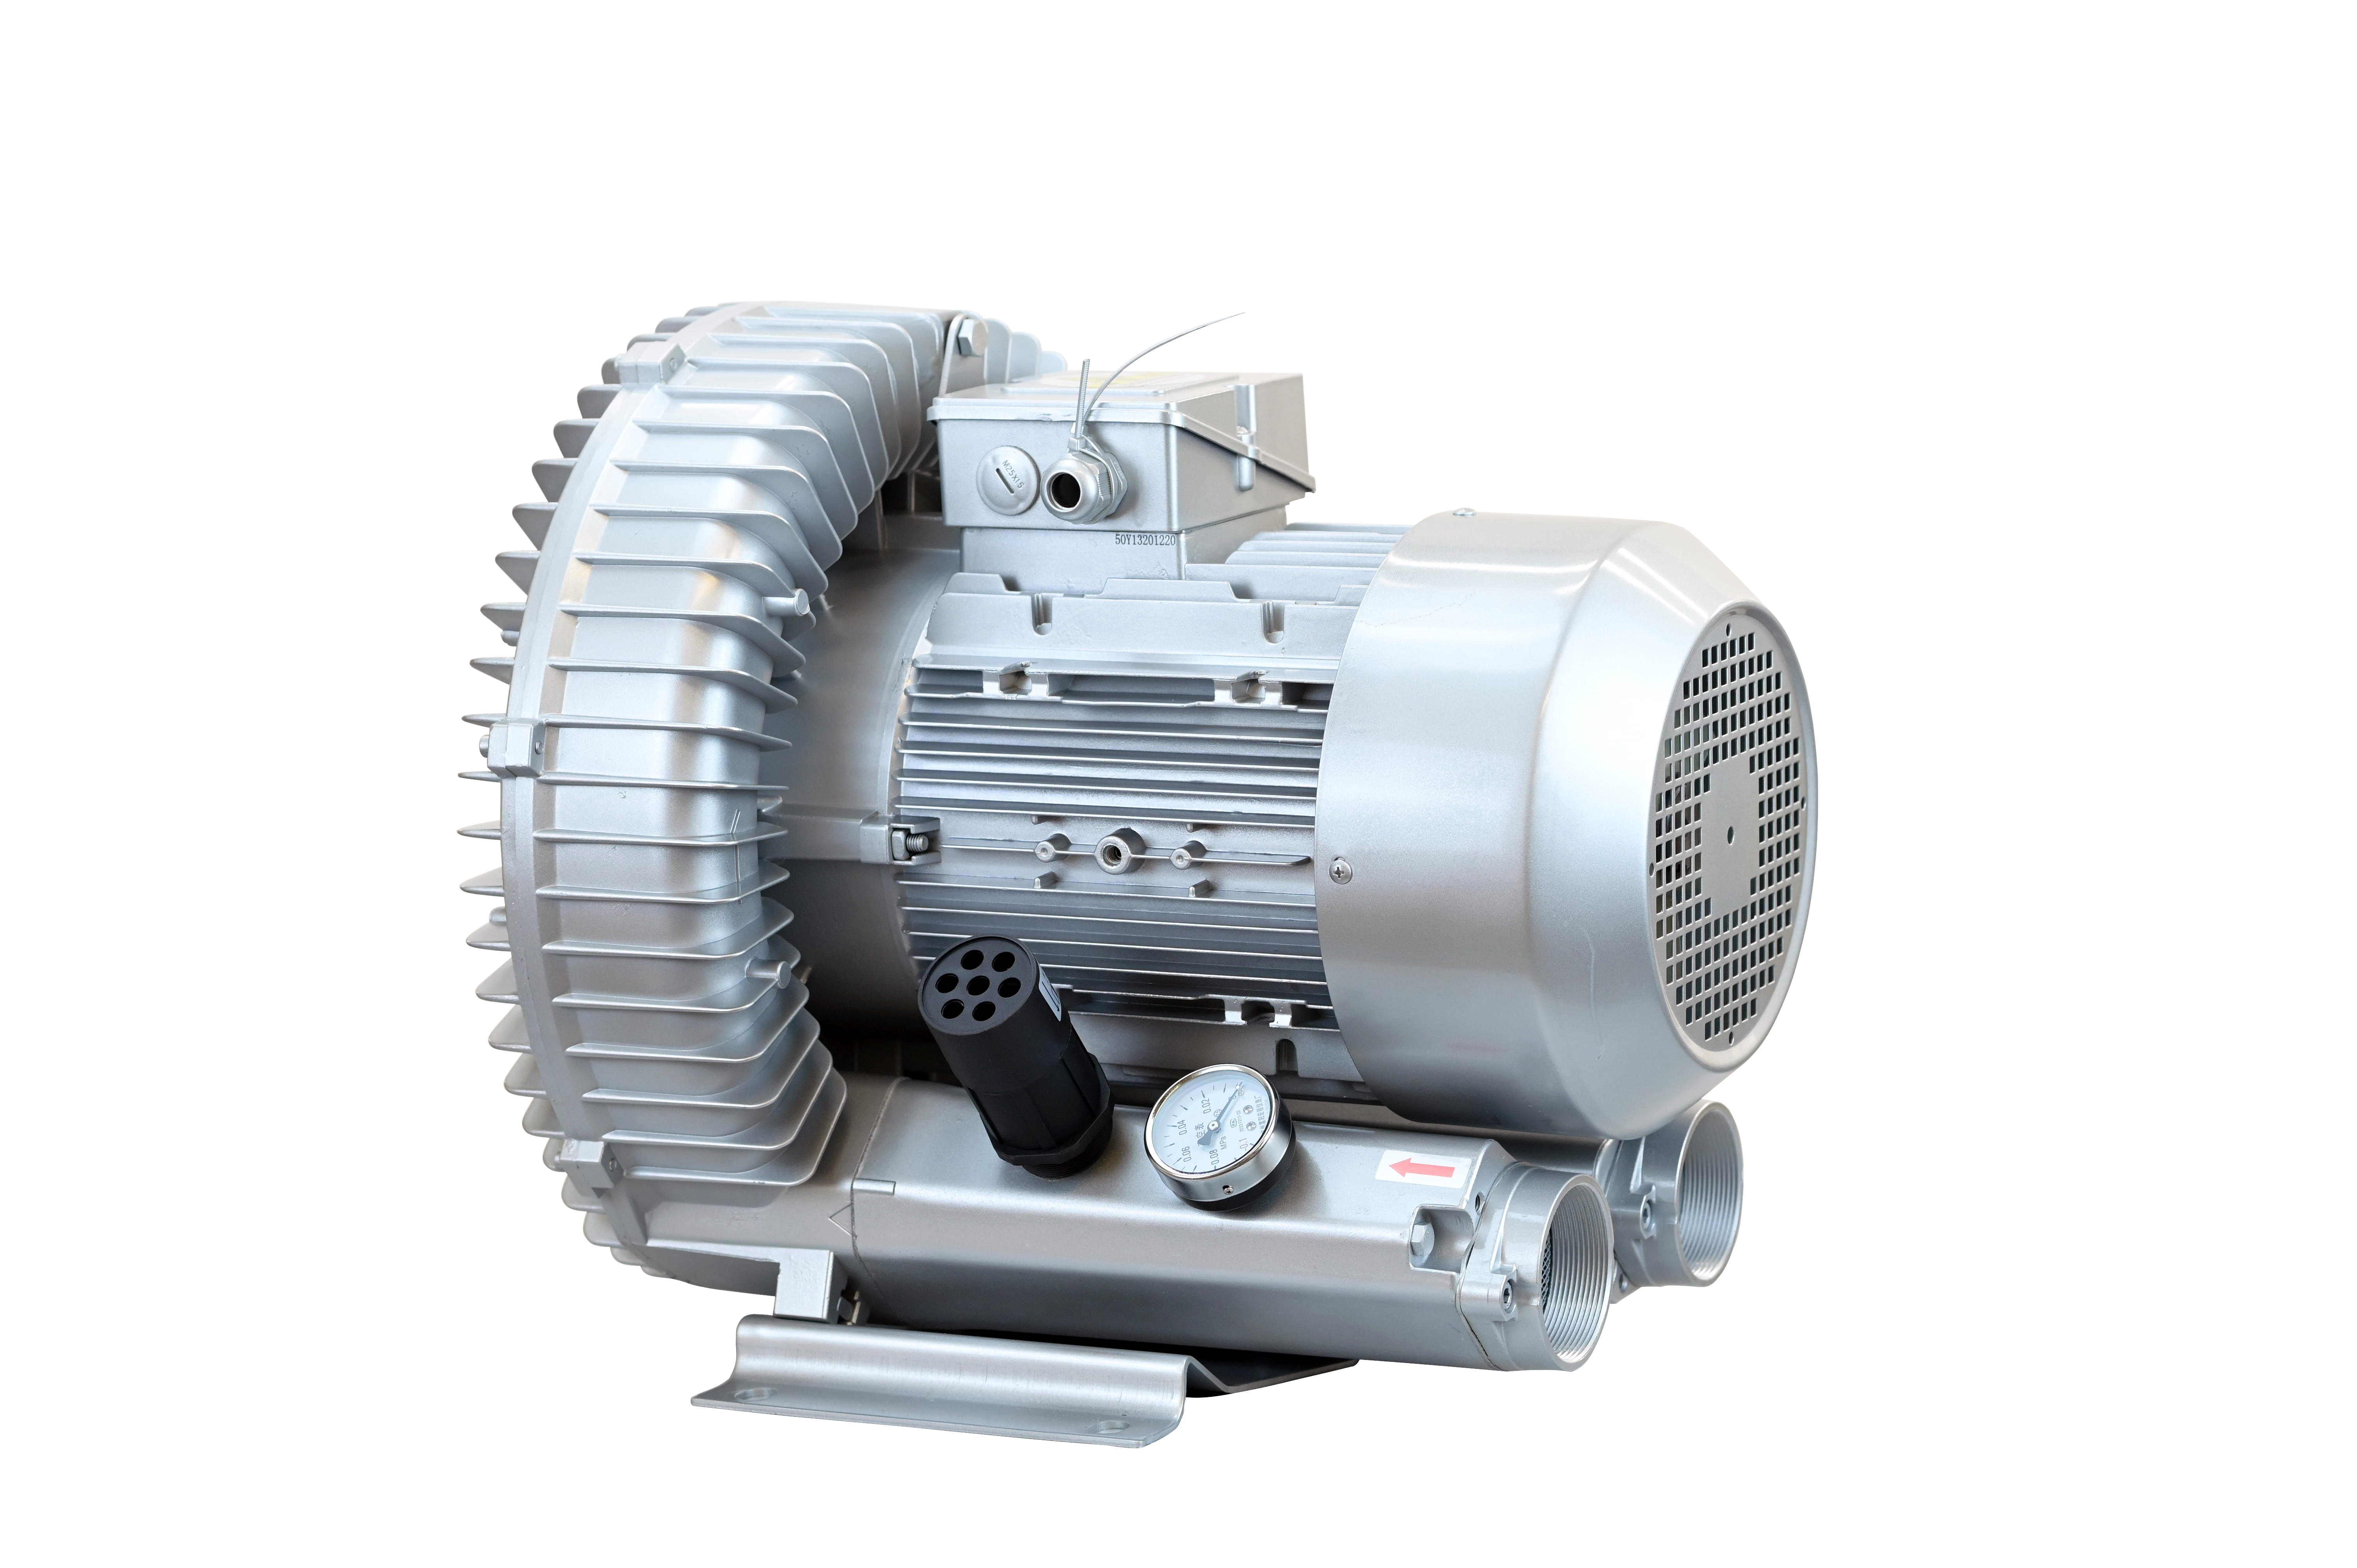
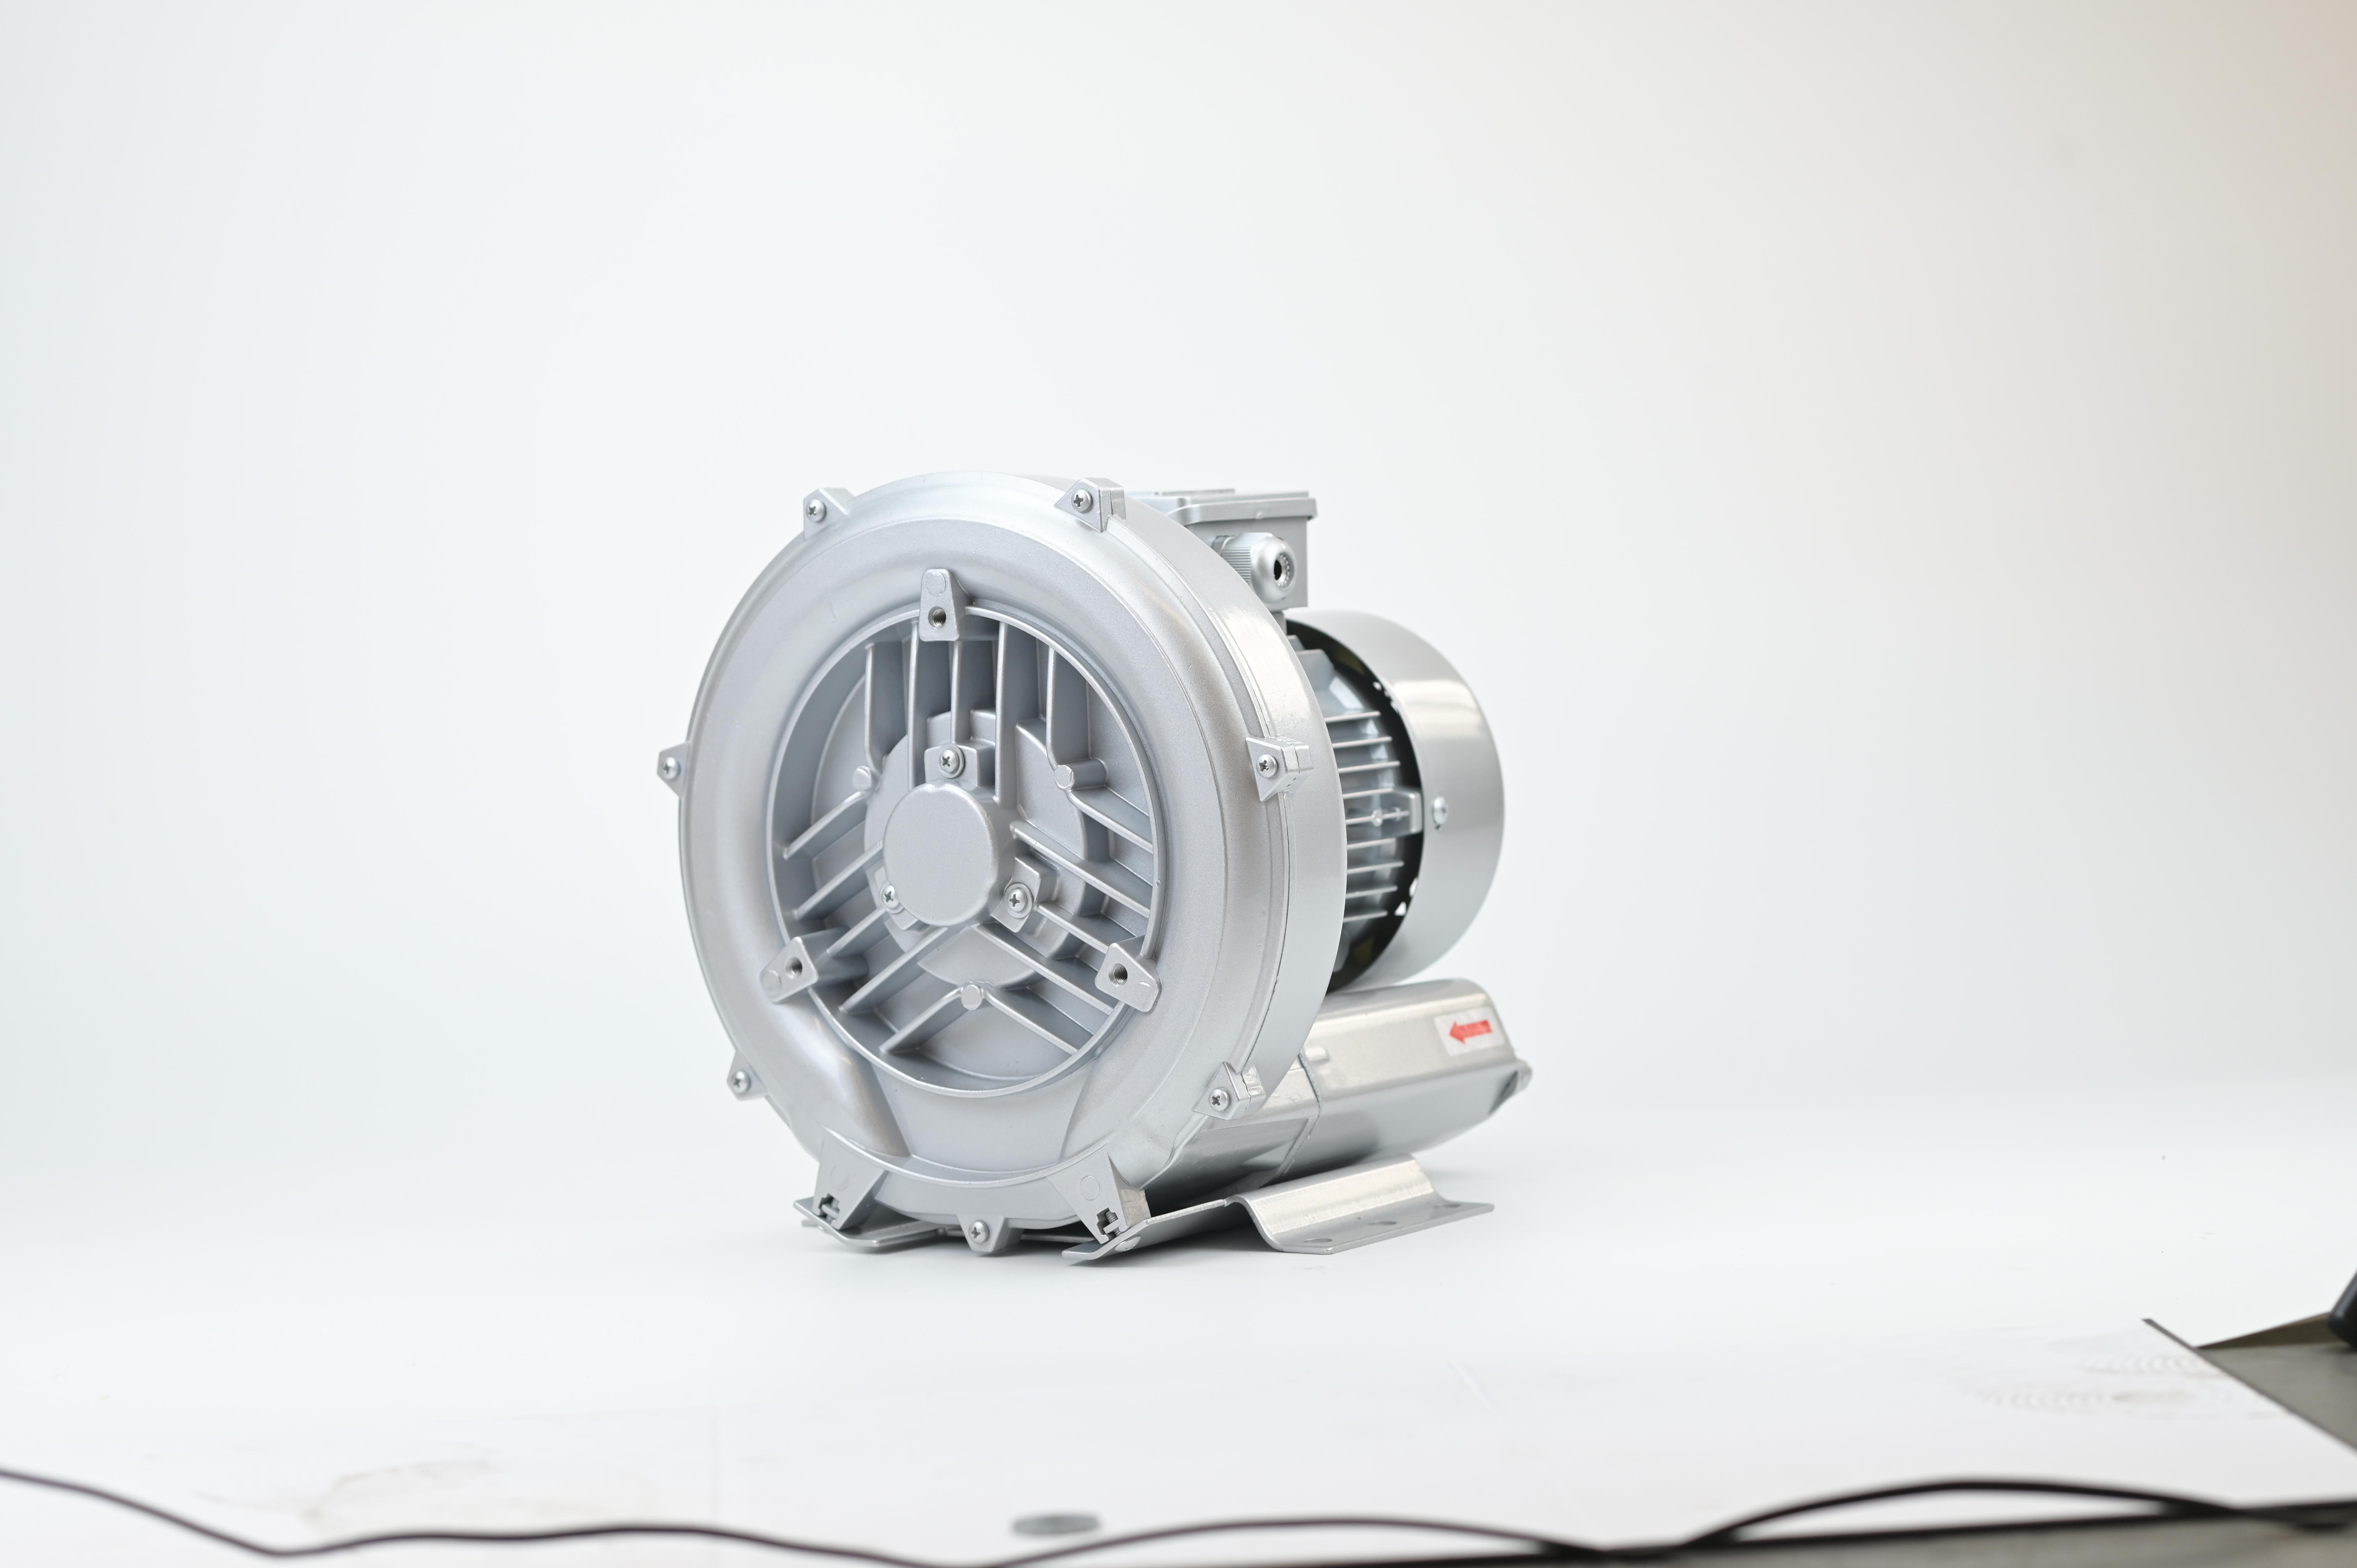
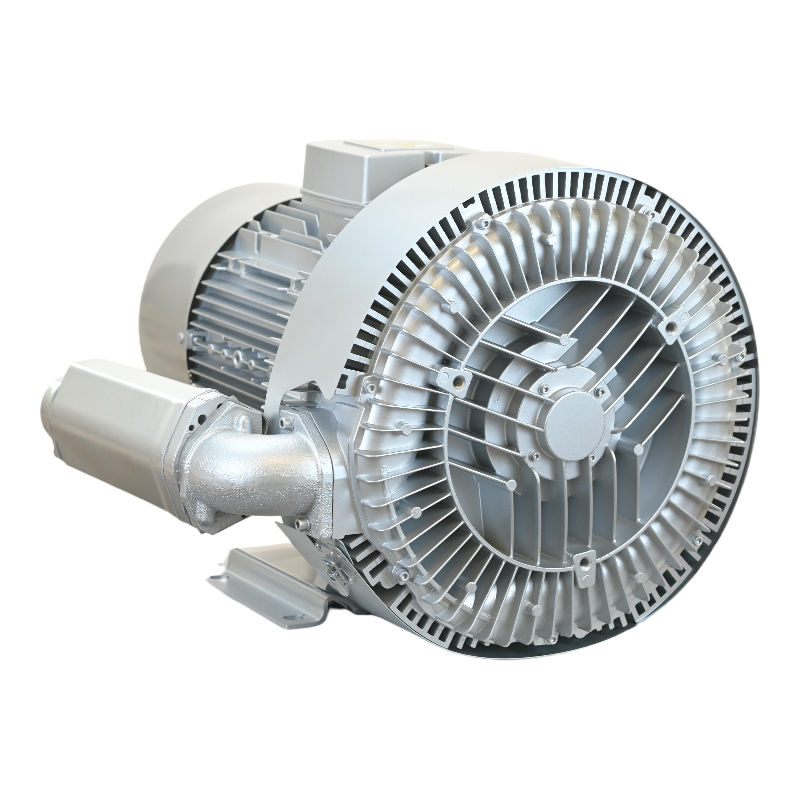
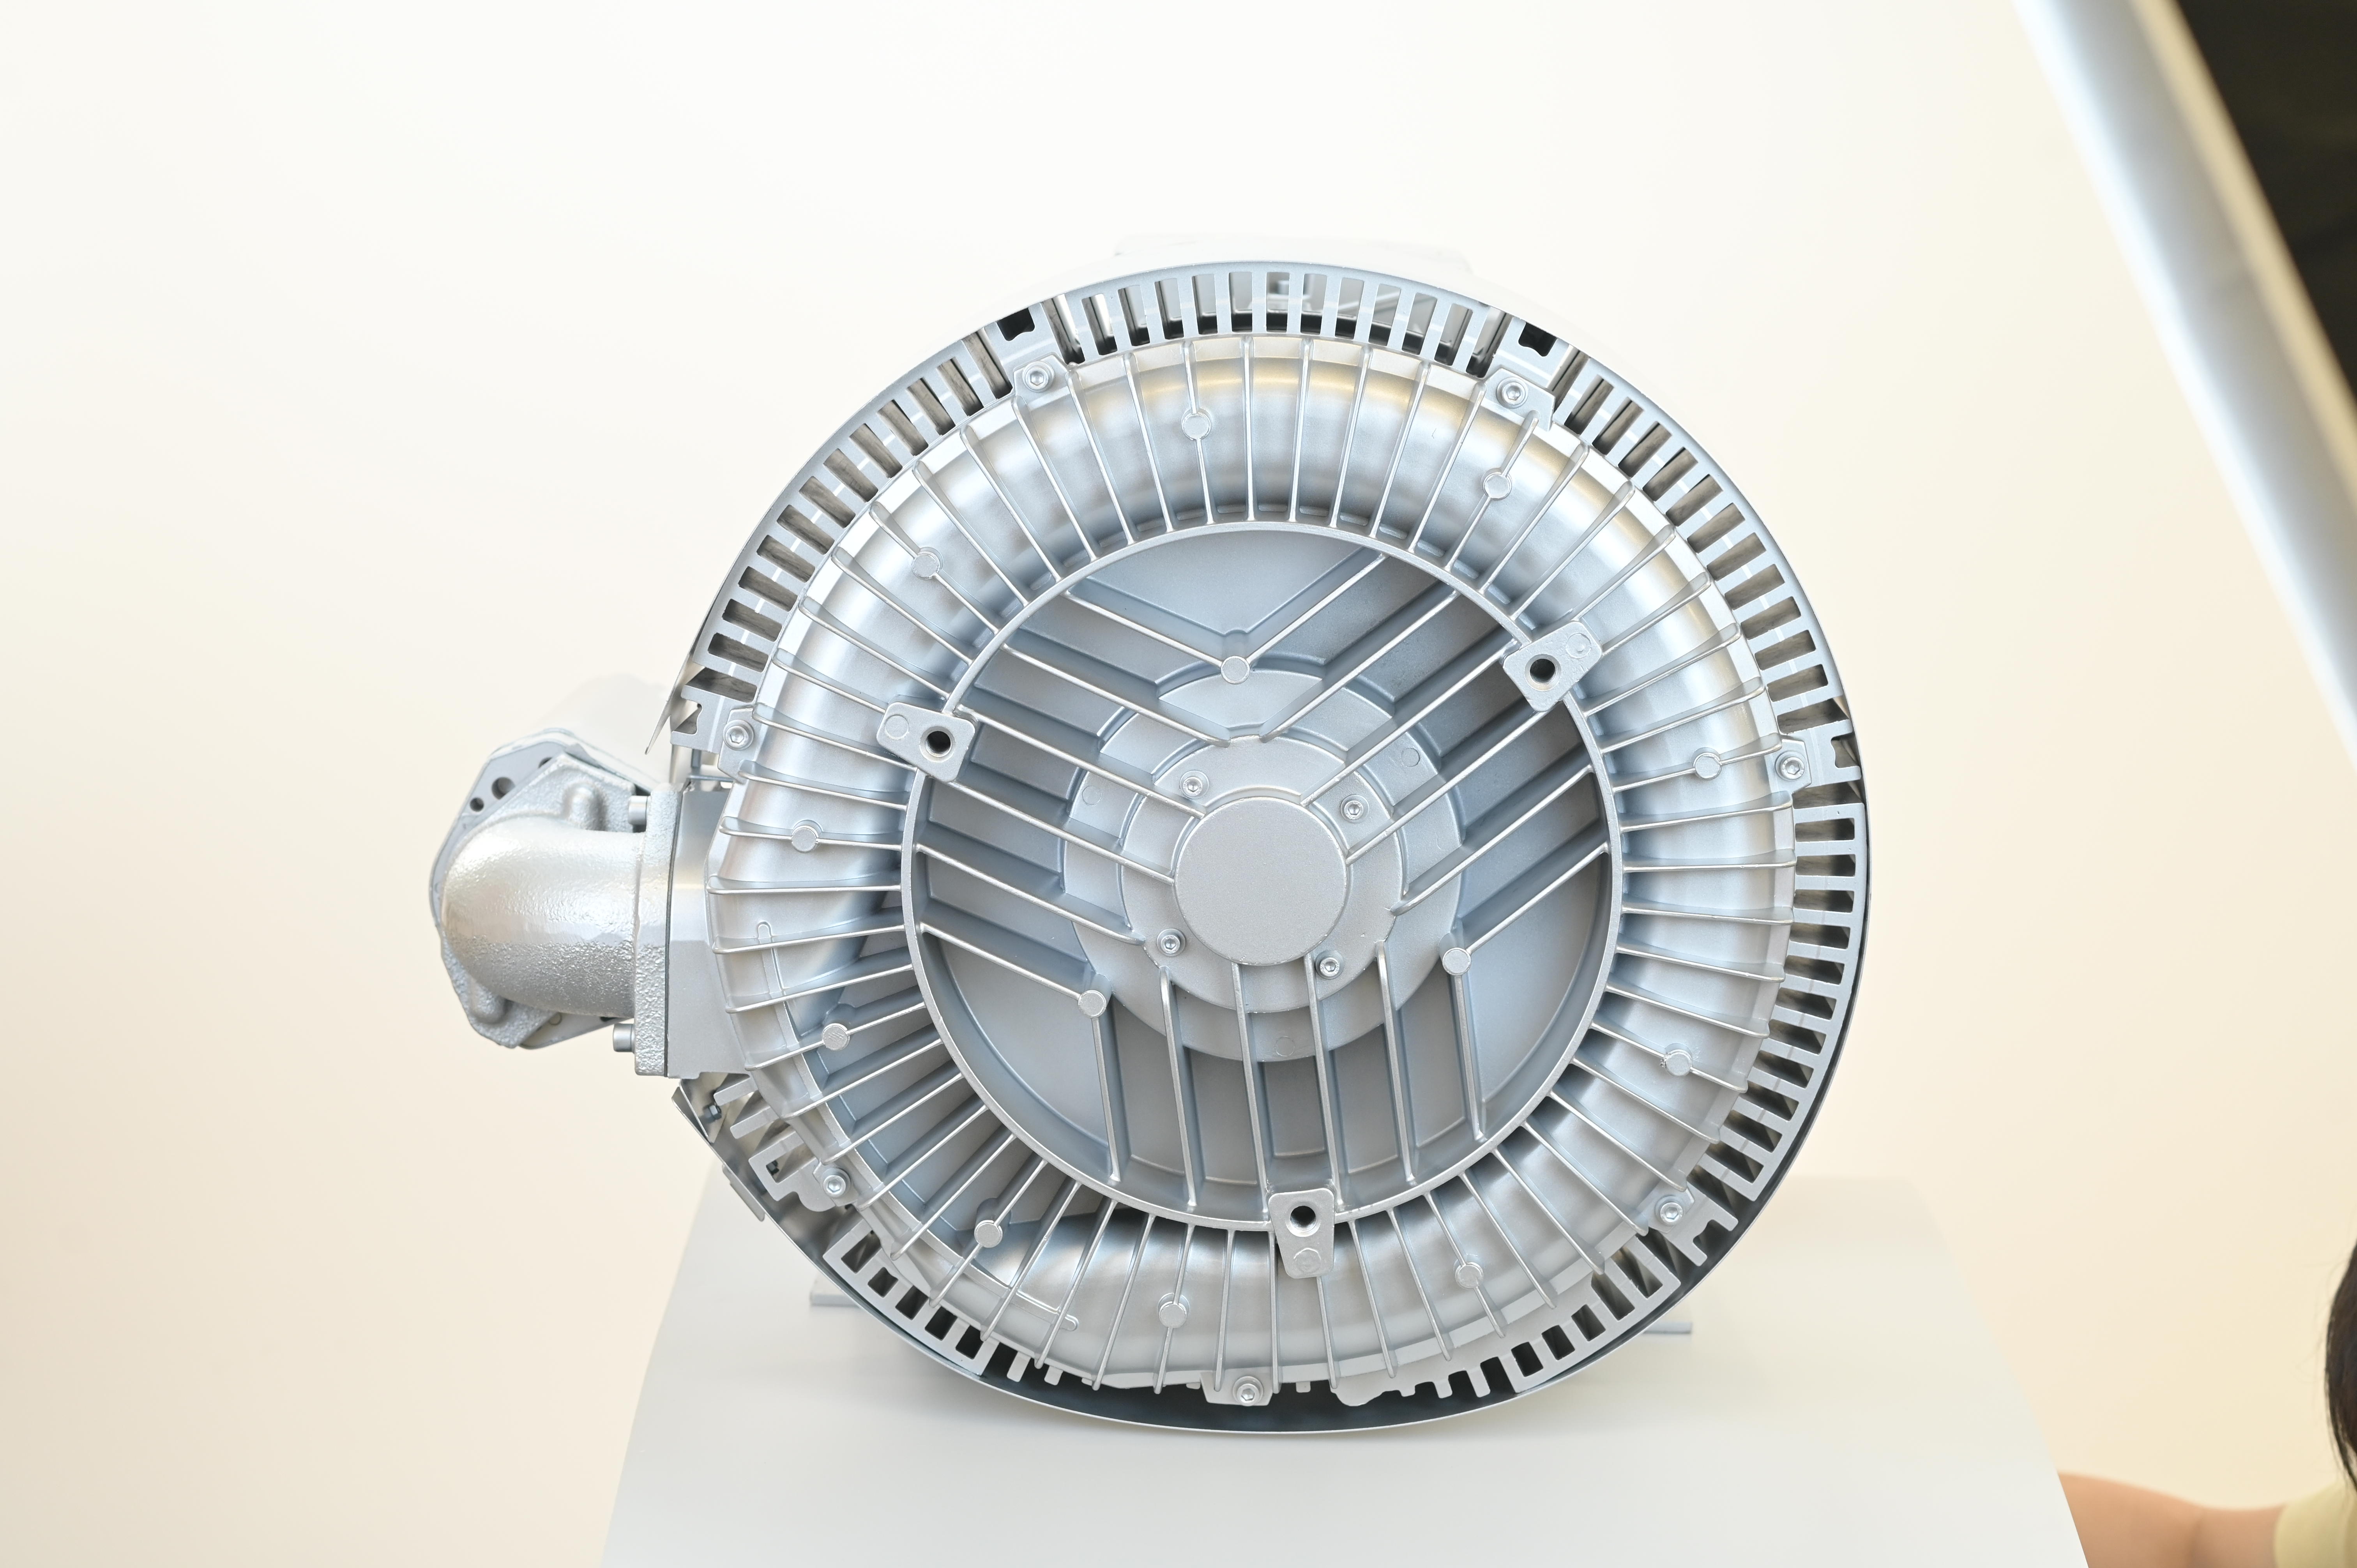
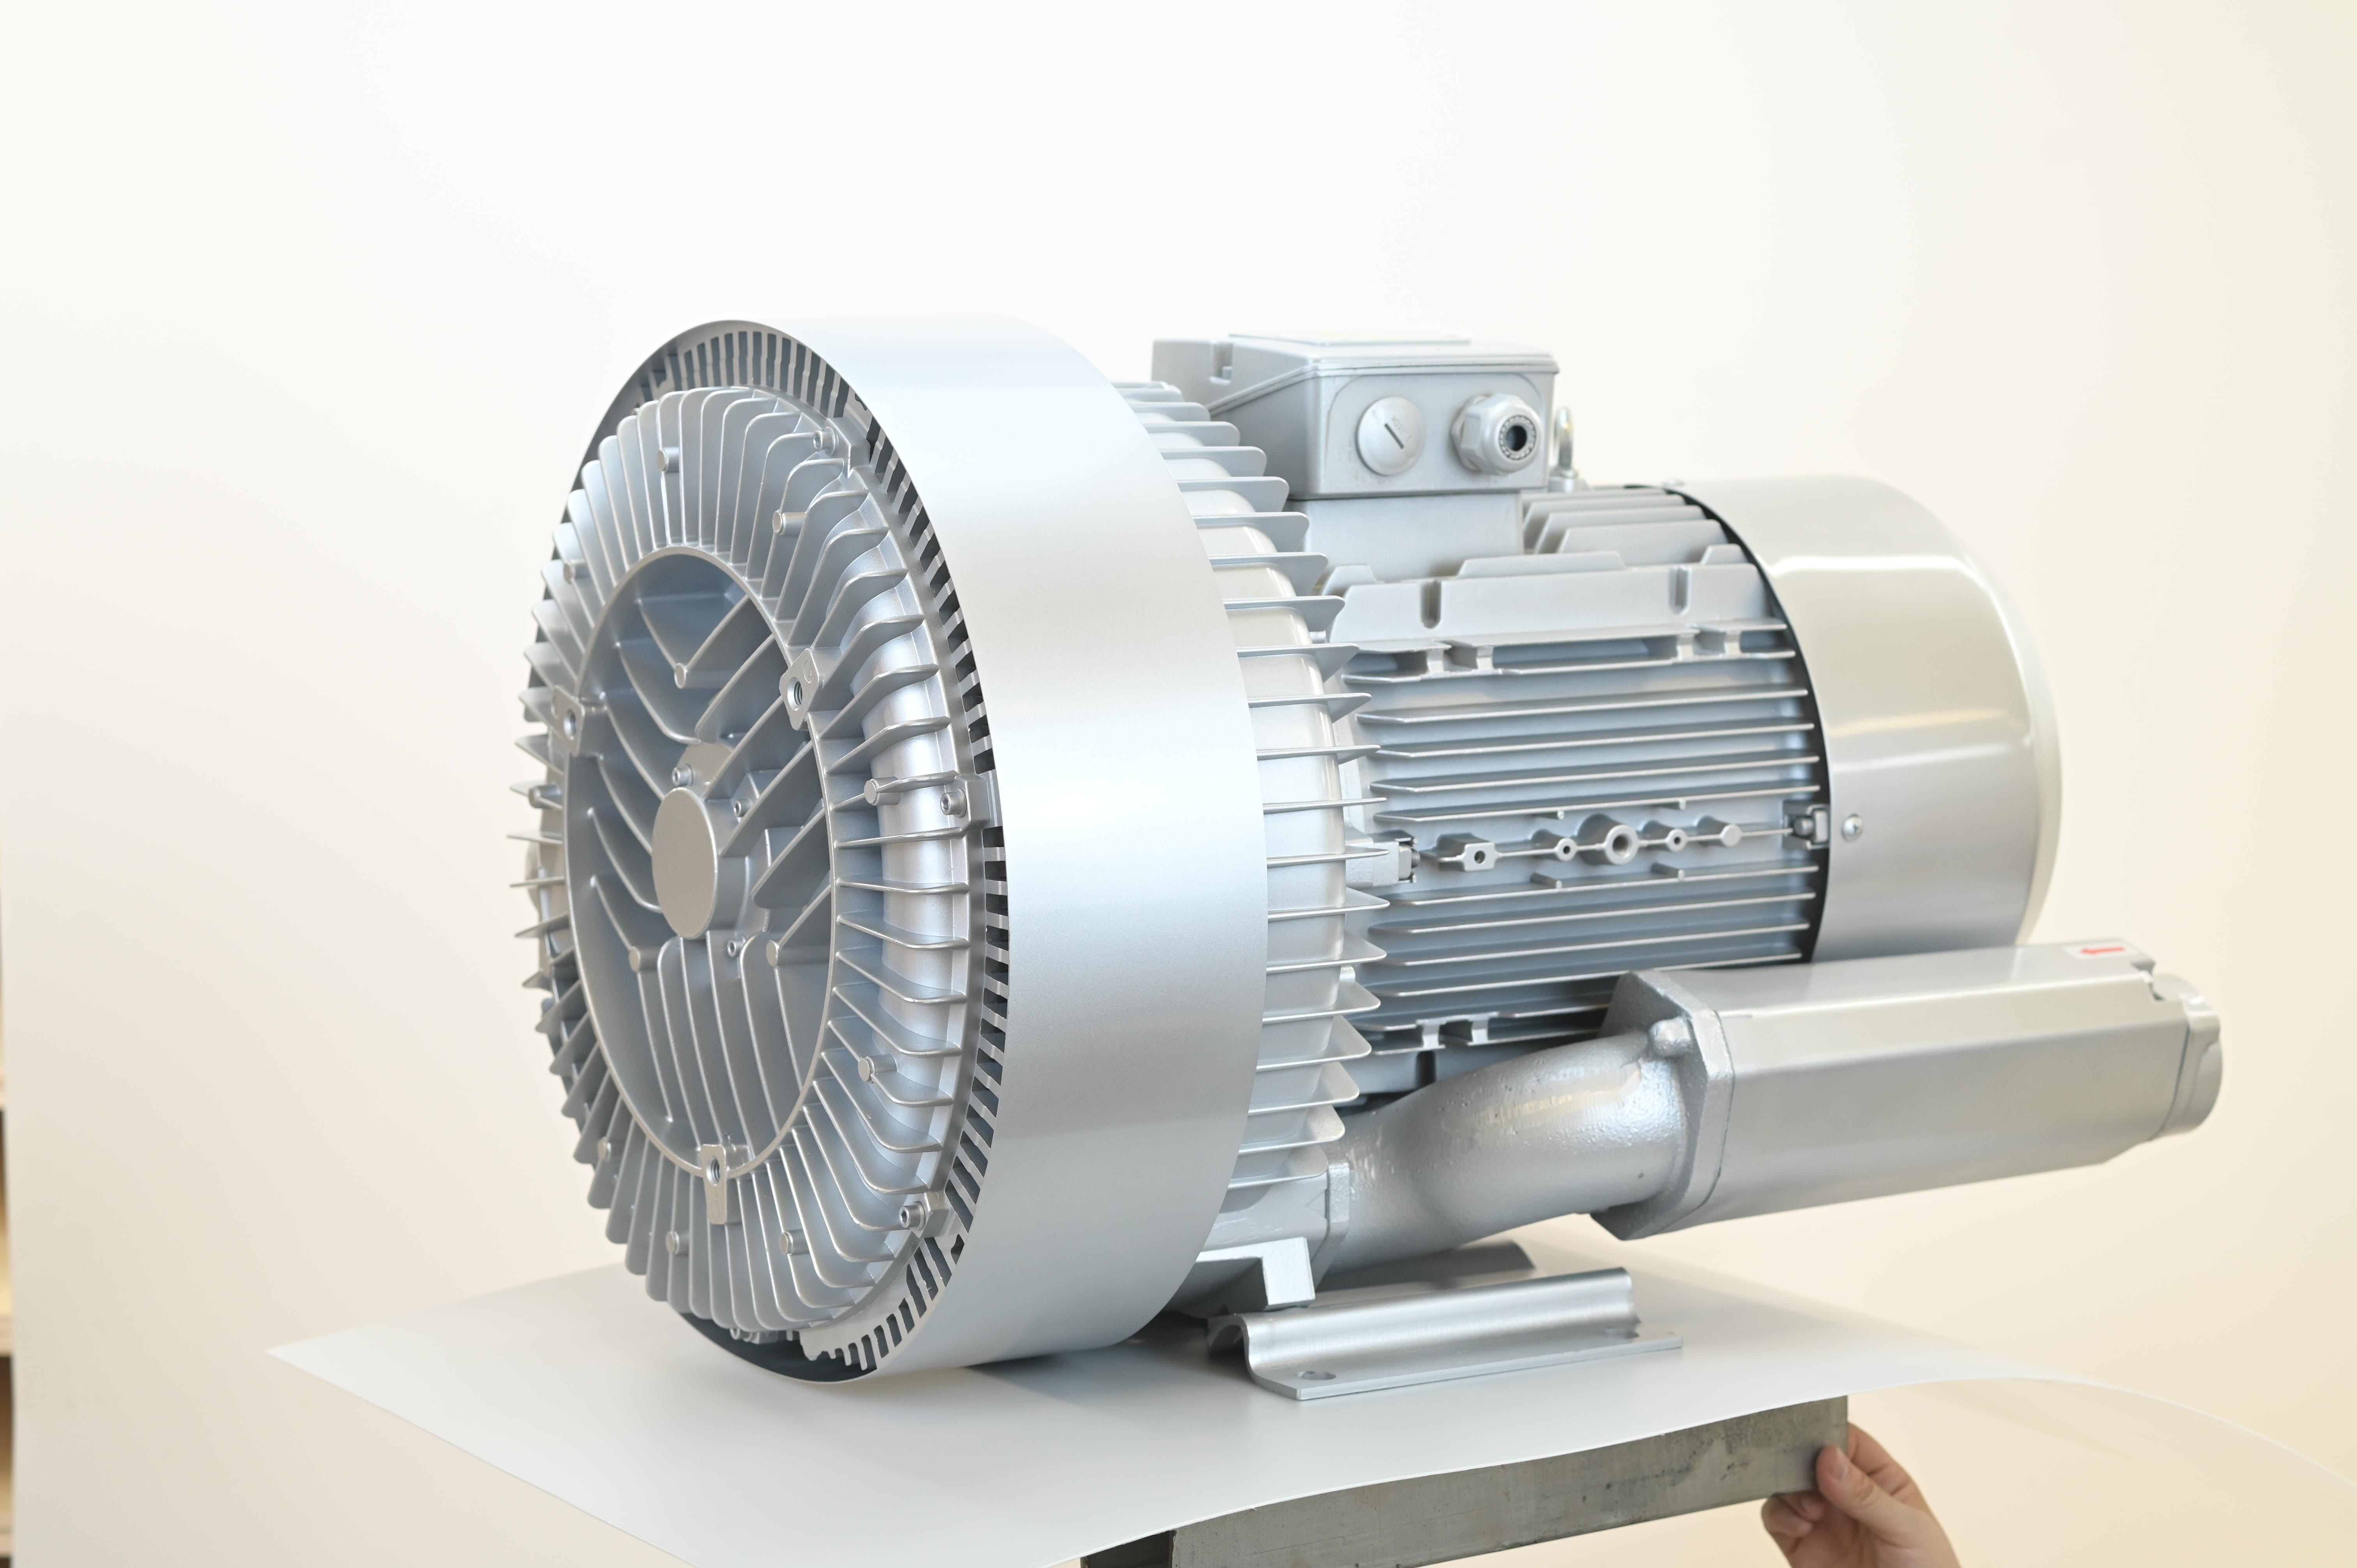
Advanced Industrial Vacuum Pump: Oil-Free, High-Efficiency Solutions

Get a Quote & Connect With Our Engineering Team

Searching for reliable industrial solutions? Let us help you find the perfect fit. Drop us a line, and our B2B technical sales team will get back to you within 12 hours (working days).
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000
Advanced Industrial Vacuum Pump Solutions for Global Industries

Advanced Industrial Vacuum Pump Solutions for Global Industries

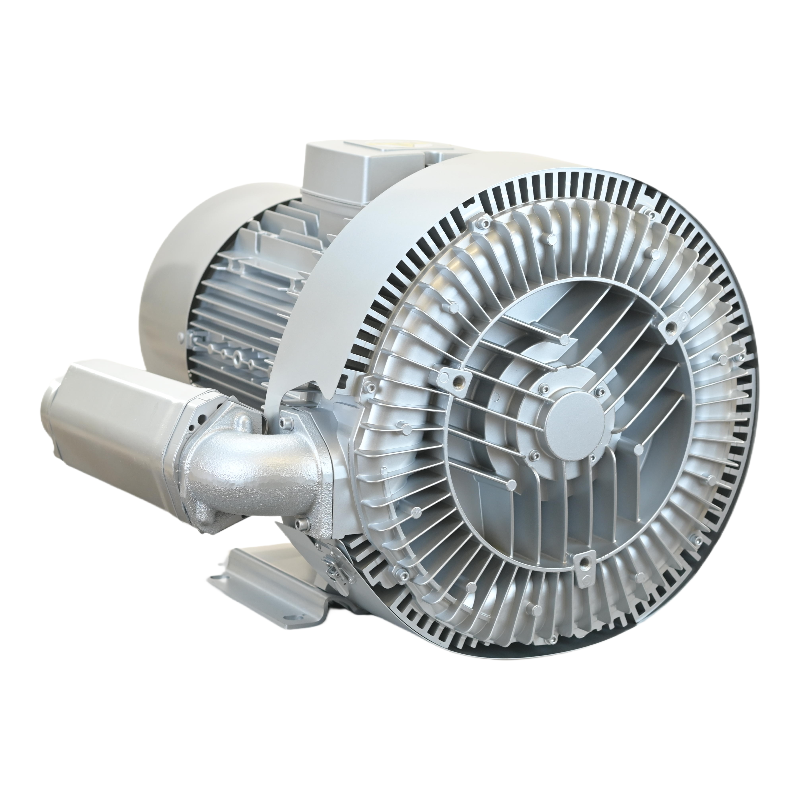
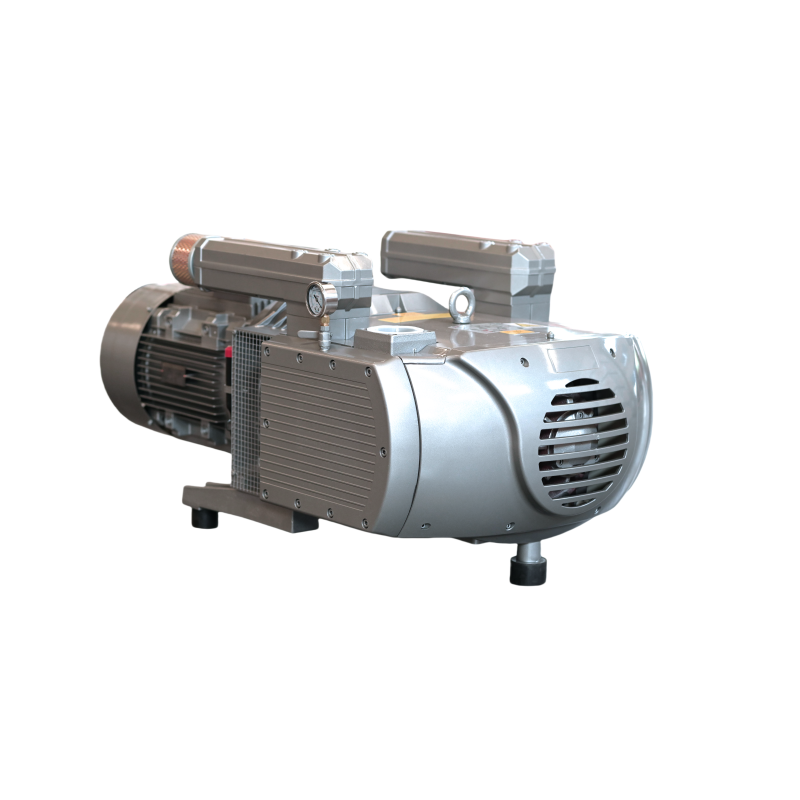
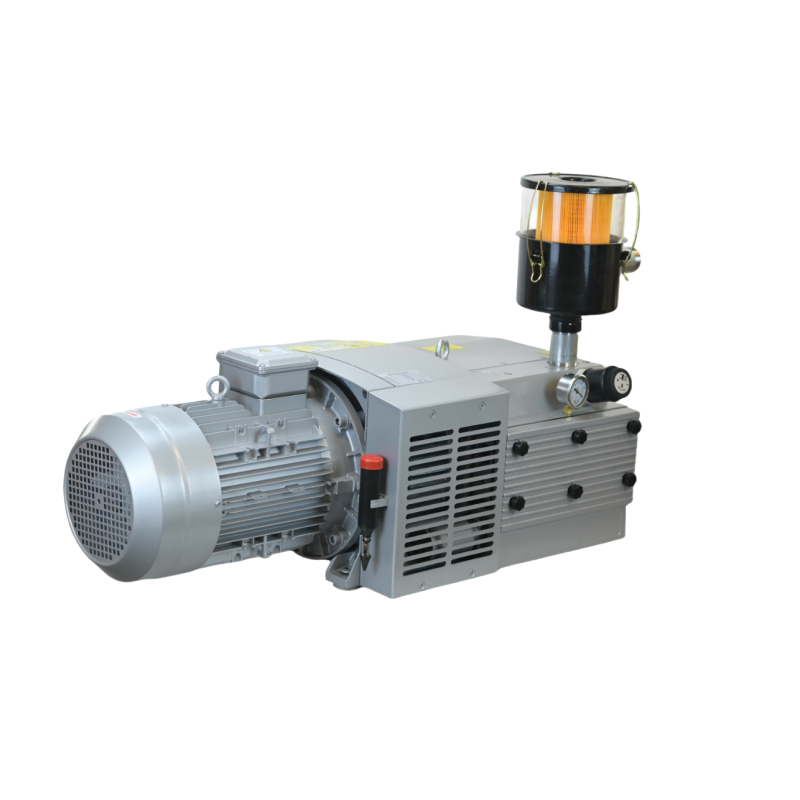
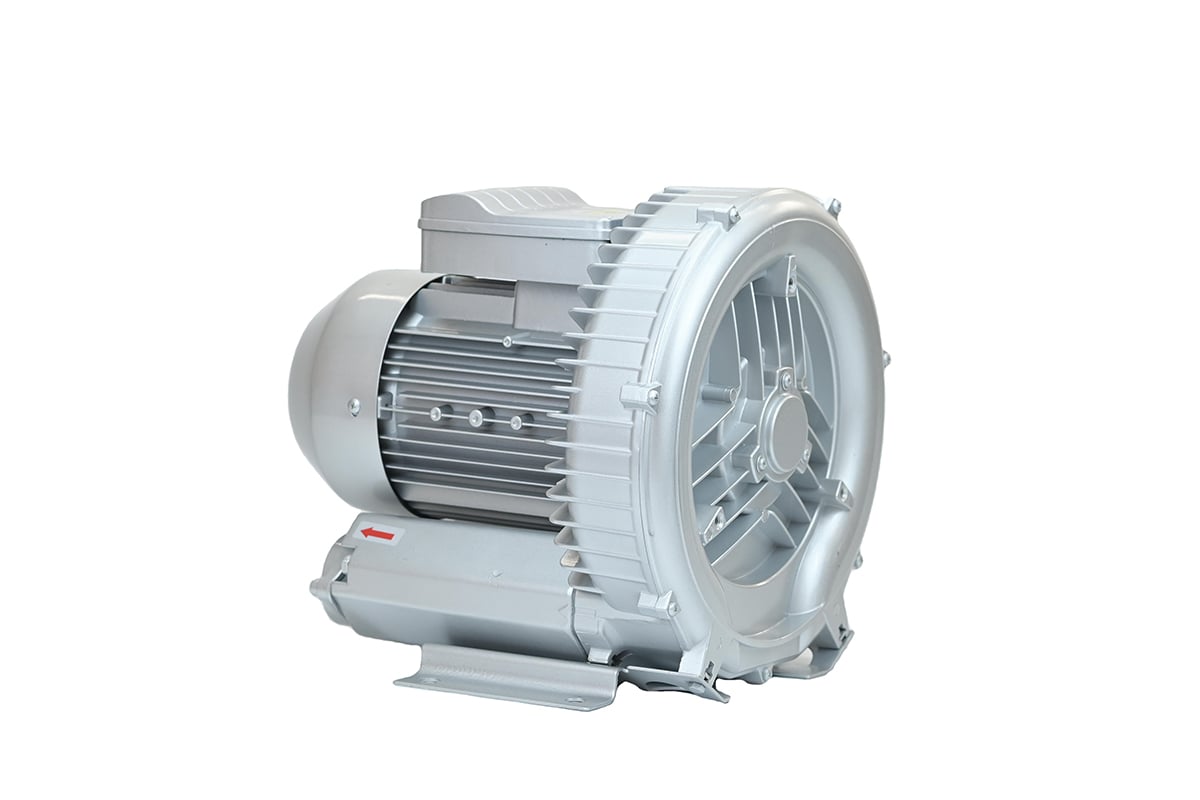
When a biopharmaceutical company in Germany needed a reliable, oil-free vacuum system for their sterile vaccine production line, off-the-shelf oil-sealed pumps posed unacceptable hydrocarbon risks. Our advanced dry rotary vane vacuum pump—featuring PTFE-coated rotors​ and IE4 premium-efficiency motors—delivered a stable ultimate vacuum of 30 Pa​ with zero oil vapor backstreaming, helping them achieve strict GMP and ISO 14644-1cleanroom compliance​ while recording an MTBF exceeding 8,500 hours​ and a failure rate of just 0.8%​ over a 12-month operational period . Since 2007, Jinan Golden Bridge Precision Machinery Co., Ltd. has engineered a diverse portfolio of advanced vacuum equipment—from 2SK two-stage water ring vacuum pumps​ for deeper vacuum in pharmaceutical distillation to SK series isothermal compression pumps​ for safely handling flammable gases—all designed to meet the rigorous demands of global industries . Unlike conventional systems that require frequent fluid changes
Get A Quote

Why Choose Our Advanced Industrial Vacuum Pumps?

Unmatched Efficiency and Performance

Our advanced industrial vacuum pumps are engineered for optimal performance, ensuring maximum efficiency in your operations. With state-of-the-art technology, these pumps deliver consistent vacuum levels, reducing energy consumption and operational costs. The robust design ensures durability and longevity, making them a reliable choice for demanding industrial applications.

Comprehensive Range of Solutions

We offer a diverse range of advanced industrial vacuum pumps tailored to various industrial needs. From dry vane vacuum pumps to oil vacuum pumps, our products cater to different applications across sectors such as manufacturing, food processing, and pharmaceuticals. This comprehensive range allows us to meet the specific requirements of our clients, ensuring they find the perfect solution for their needs.

Global Reach with Local Expertise

With a strong presence in international markets, our advanced industrial vacuum pumps are trusted by clients across Europe, North America, South America, and Australia. Our experienced foreign trade team provides exceptional online service and support, ensuring that our customers receive the assistance they need, regardless of their location. Our commitment to customer satisfaction is backed by years of industry experience and a focus on building lasting partnerships.

Related products

We appreciate the crucial part that advanced industrial vacuum pumps play with operational efficiency and productivity at Jinan Golden Bridge Precision Machinery Co., Ltd. Highest industry standards are met with precision engineering and innovative technology. Pumps, high-pressure blowers, or vacuum systems – whatever you need – we build our products to perform reliably in any application. With a commitment to R&D, we are able to keep our customers and clients with the current trends in vacuum technology. Our focus is our customers and we adapt our products to improve and meet the requirements of the industry. With advanced industrial vacuum pumps, we offer proven quality and performance.

Frequently Asked Questions about Advanced Industrial Vacuum Pumps

What types of advanced industrial vacuum pumps do you offer?

We offer a variety of advanced industrial vacuum pumps, including dry vane vacuum pumps, oil vacuum pumps, high-pressure blowers, and complete vacuum systems. Each type is designed to cater to specific industrial applications, ensuring optimal performance and efficiency.
Choosing the right vacuum pump depends on several factors, including the application type, required vacuum level, and flow rate. Our expert team is available to assist you in selecting the most suitable pump based on your specific requirements.

Related article

Vortex Vacuum Pumps: Oil-Free, Energy-Efficient Solutions for Industrial Applications

24

Nov

Vortex Vacuum Pumps: Oil-Free, Energy-Efficient Solutions for Industrial Applications

Discover oil-free, 30-50% more energy-efficient vortex vacuum pumps ideal for semiconductors, medical, and food packaging. Zero contamination, low noise, global support. Request a quote today.
View More
What Are the Energy-Saving Technologies Applied in Modern Industrial Air Compressors?

22

Dec

What Are the Energy-Saving Technologies Applied in Modern Industrial Air Compressors?

Cut compressor energy costs by up to 35%—discover VSD, heat recovery, smart controls & more. Learn proven efficiency upgrades for manufacturers. Download the tech guide now.
View More
What Factors Influence the Energy Efficiency of Air Blowers in Industrial Settings?

13

Mar

What Factors Influence the Energy Efficiency of Air Blowers in Industrial Settings?

What really drives energy waste in industrial air blowers? Discover 7 key technical & operational factors—and cut energy costs by up to 40%. Download the efficiency checklist now.
View More
Why Do Industrial Air Compressors Require Regular Air Filter Replacement?

25

Dec

Why Do Industrial Air Compressors Require Regular Air Filter Replacement?

Neglecting air filter replacement risks downtime, energy waste, and costly repairs. Learn how regular maintenance boosts efficiency & extends compressor life—download our maintenance checklist now.
View More

Customer Testimonials on Our Advanced Industrial Vacuum Pumps

John Smith
Reliable Performance in Demanding Conditions

The advanced industrial vacuum pump we purchased has exceeded our expectations. It operates efficiently and reliably, even in our demanding manufacturing environment. The support from Jinan Golden Bridge has been exceptional!

Maria Garcia
Innovative Solutions that Enhance Productivity

We have been using Jinan Golden Bridge’s vacuum pumps for over five years, and they have significantly improved our production efficiency. Their commitment to innovation is evident in their products, and we appreciate their responsive customer service.

Get a Quote & Connect With Our Engineering Team

Searching for reliable industrial solutions? Let us help you find the perfect fit. Drop us a line, and our B2B technical sales team will get back to you within 12 hours (working days).
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000
Innovative Technology for Enhanced Efficiency

Innovative Technology for Enhanced Efficiency

When a chemical plant in Germany retrofitted their distillation line, their legacy vacuum pumps consumed 42 kW/h​ regardless of load, driving up energy bills. After installing our 2SK two-stage water ring vacuum pump—featuring isothermal compression​ and permanent magnet variable speed drive (PM VSD)—they recorded a 35% reduction in power consumption​ while achieving a stable 33 mbar ultimate vacuum, verified by a third-party energy audit. Unlike conventional single-stage pumps where cavitation erodes impellers within 12 months, our dual-stage cascade design​ distributes the pressure differential evenly, extending service life to 25,000+ hours​ with minimal maintenance. Every unit is CE certified, assembled under ISO 9001​ controls, and backed by 24/7 IoT remote monitoring​ that tracks vacuum stability, motor temperature, and bearing health in real time, shifting maintenance from reactive to predictive.
Robust Design for Longevity

Robust Design for Longevity

When a mining operation in Western Australia needed vacuum pumps for mineral dewatering, their previous units failed within 14 months due to abrasive slurry ingress and 45°C ambient heat. Our 2SK two-stage water ring vacuum pump—constructed with stainless steel internals​ and wear-resistant cast iron casings—has now logged 28,000 hours​ without a single impeller replacement. Unlike oil-sealed pumps that require fluid changes every 2,000 hours and generate hazardous waste, our water ring design​ uses process liquid as both seal and coolant, eliminating lubricant costs entirely while withstanding harsh, particle-laden environments. Every unit undergoes a 72-hour stress test at 55°C​ before shipment, with SKF heavy-duty bearings​ rated for 100,000 hours​ under continuous load. Assembled under ISO 9001​ controls and CE certified, our pumps are engineered for maintenance intervals extended to 8,000 hours
+86 0531 88060599
13386448931
[email protected]

Get a Quote & Connect With Our Engineering Team

Searching for reliable industrial solutions? Let us help you find the perfect fit. Drop us a line, and our B2B technical sales team will get back to you within 12 hours (working days).
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000