Vacuum Pump for Clean Room | Oil-Free Industrial Solutions

Get a Quote & Connect With Our Engineering Team

Searching for reliable industrial solutions? Let us help you find the perfect fit. Drop us a line, and our B2B technical sales team will get back to you within 12 hours (working days).
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000
 High-Performance Vacuum Pump for Clean Room Applications

High-Performance Vacuum Pump for Clean Room Applications

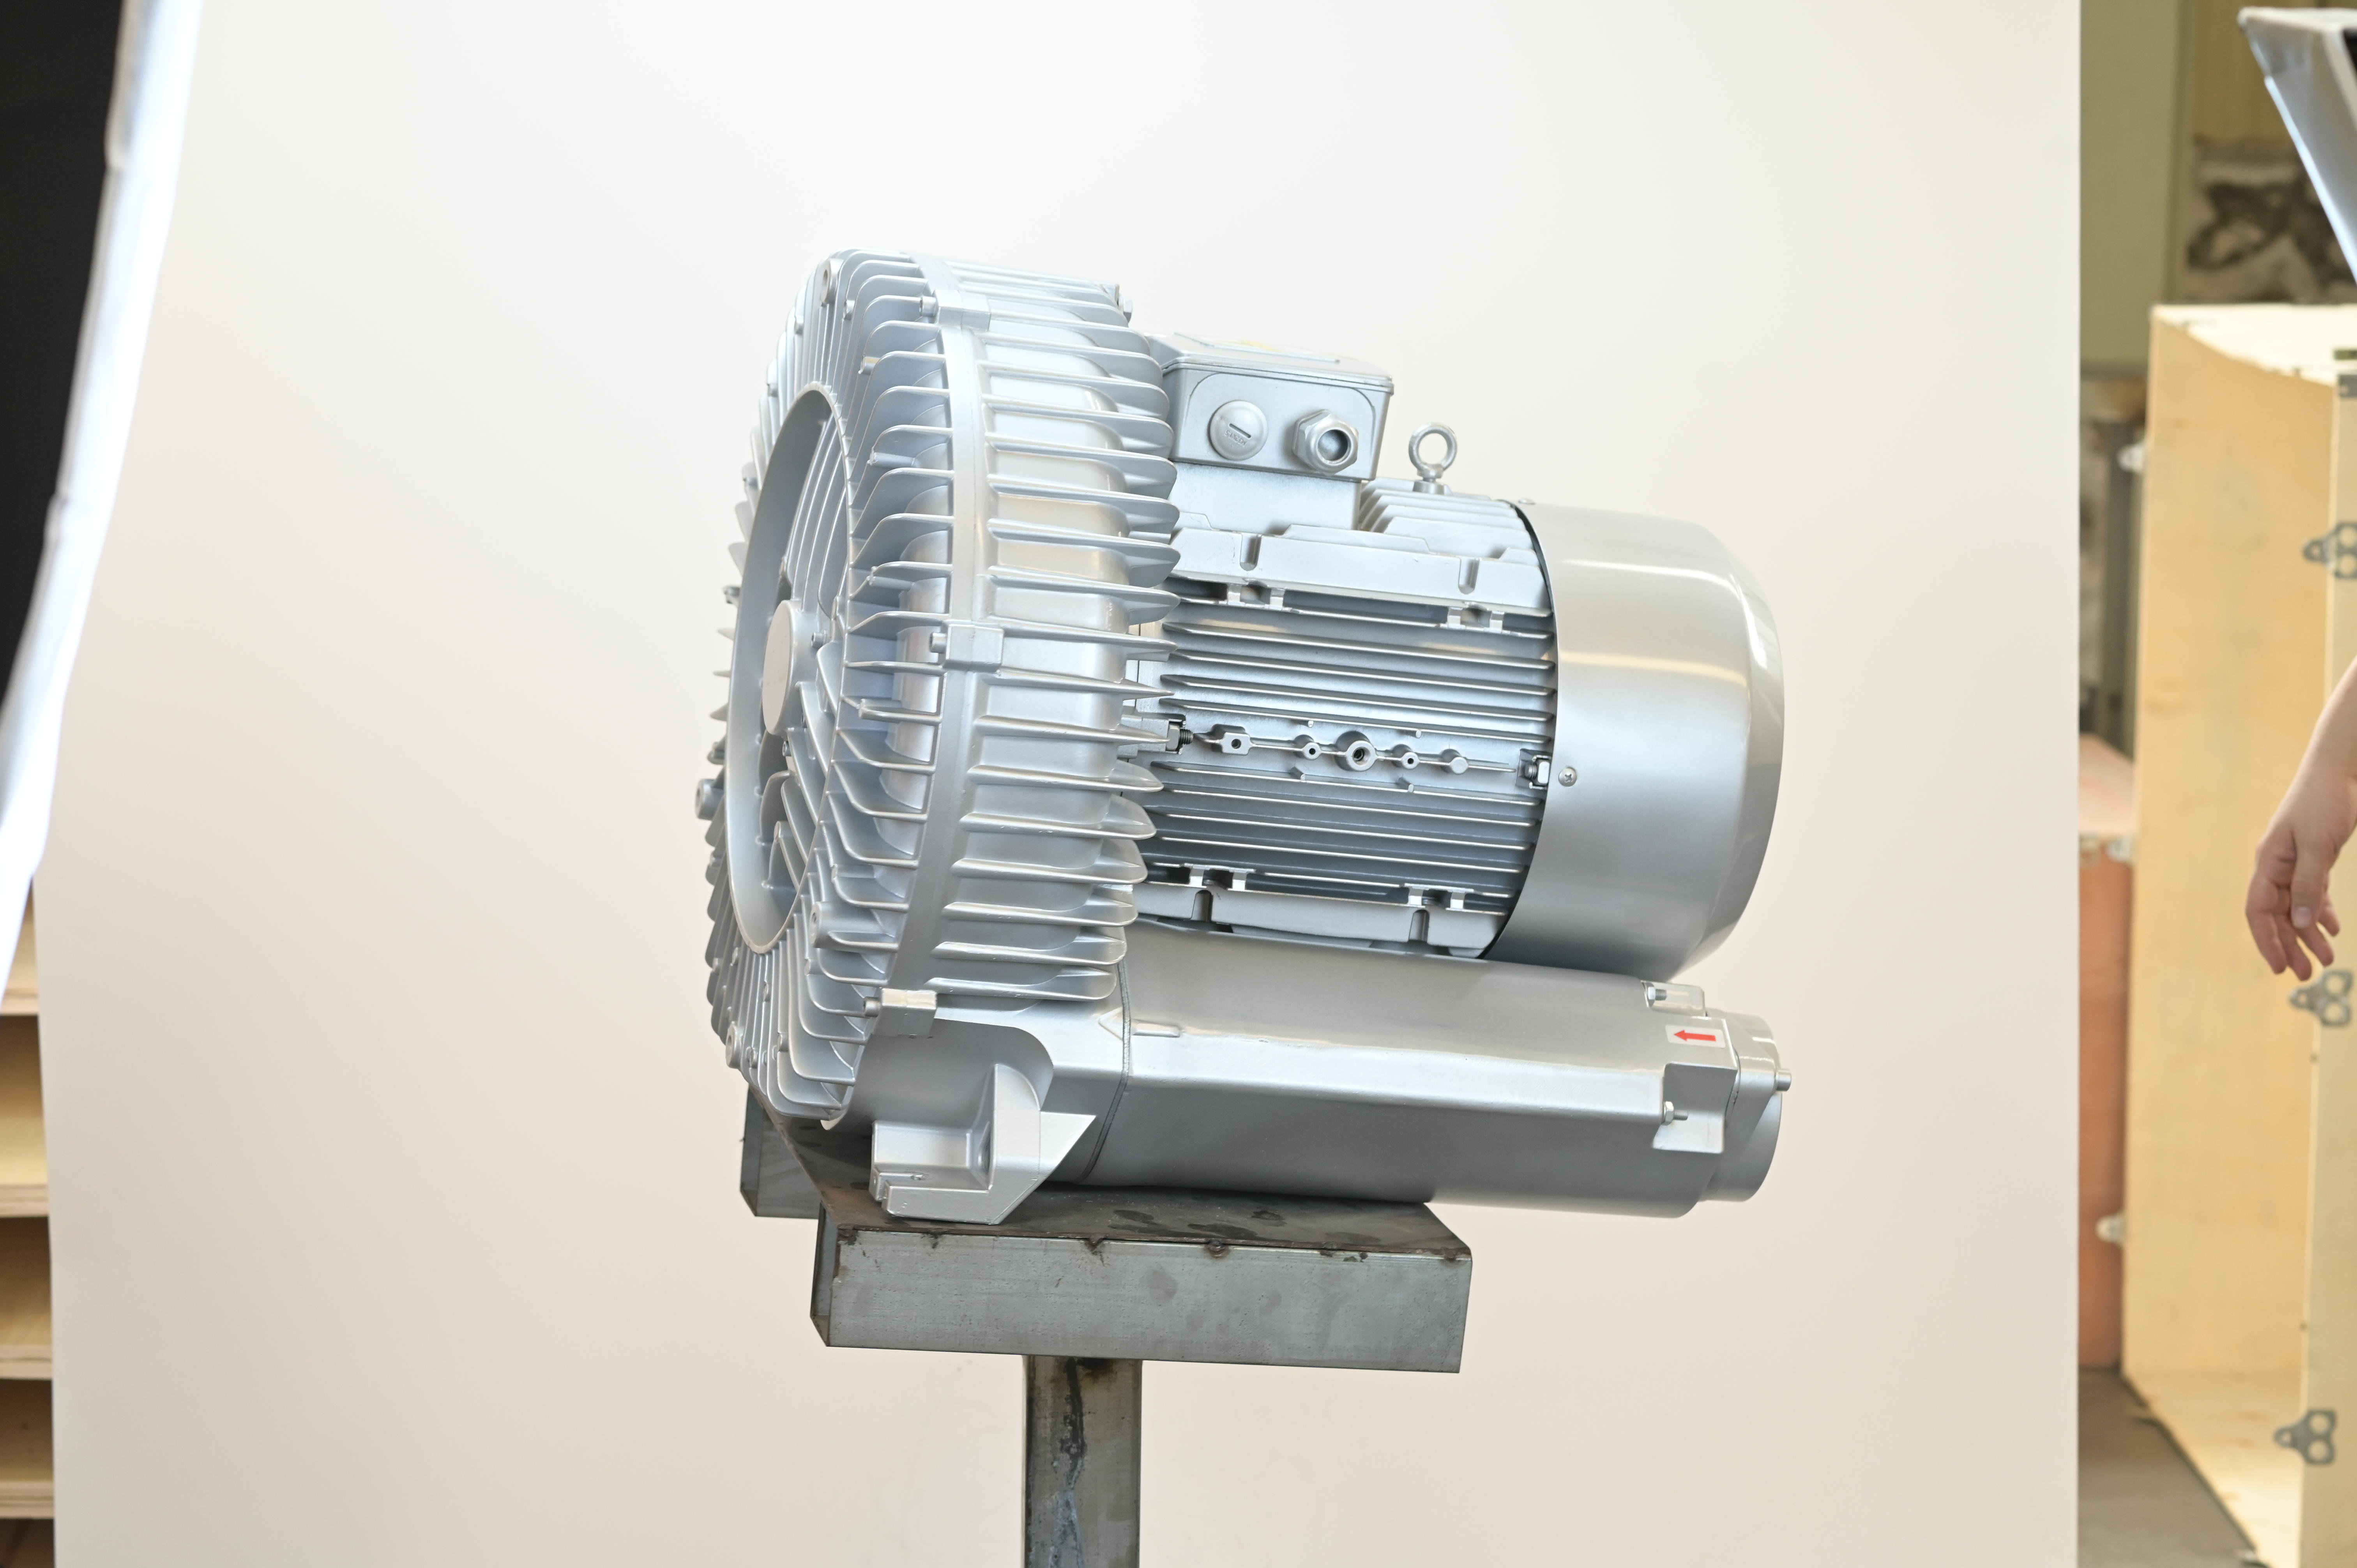
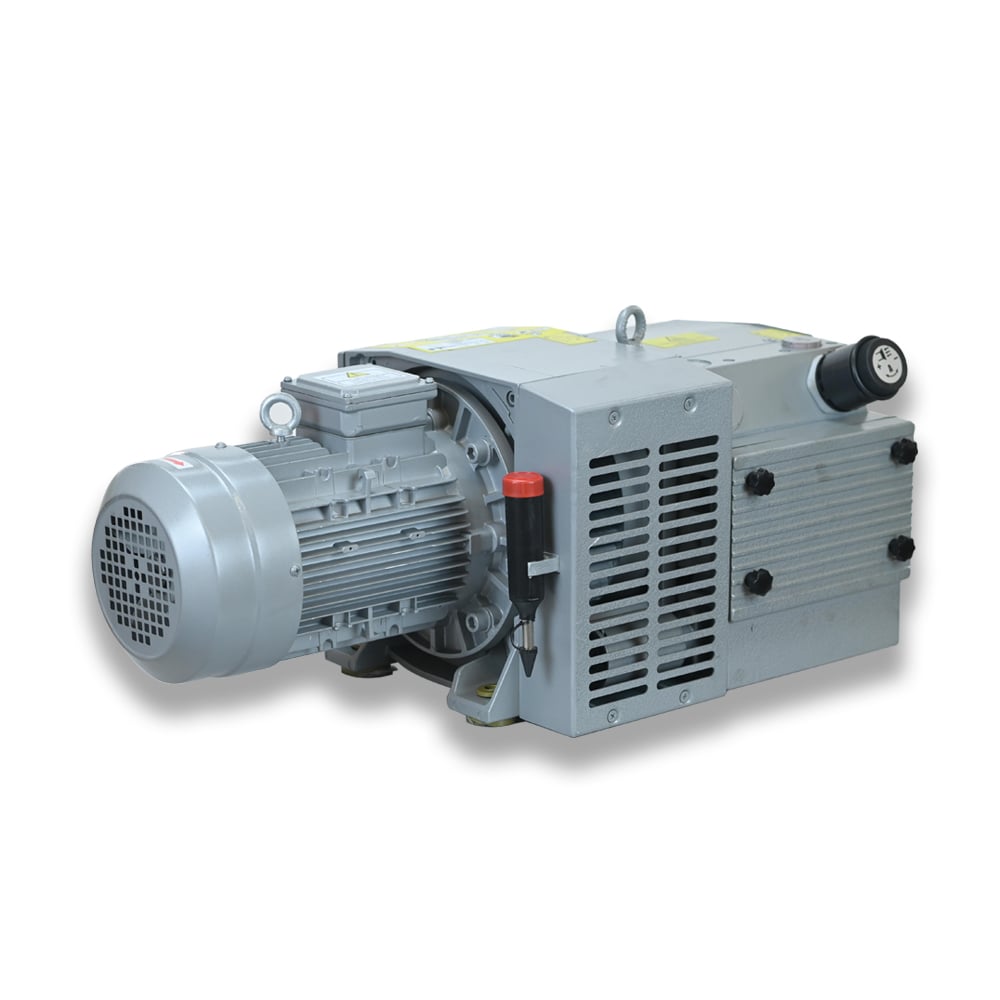
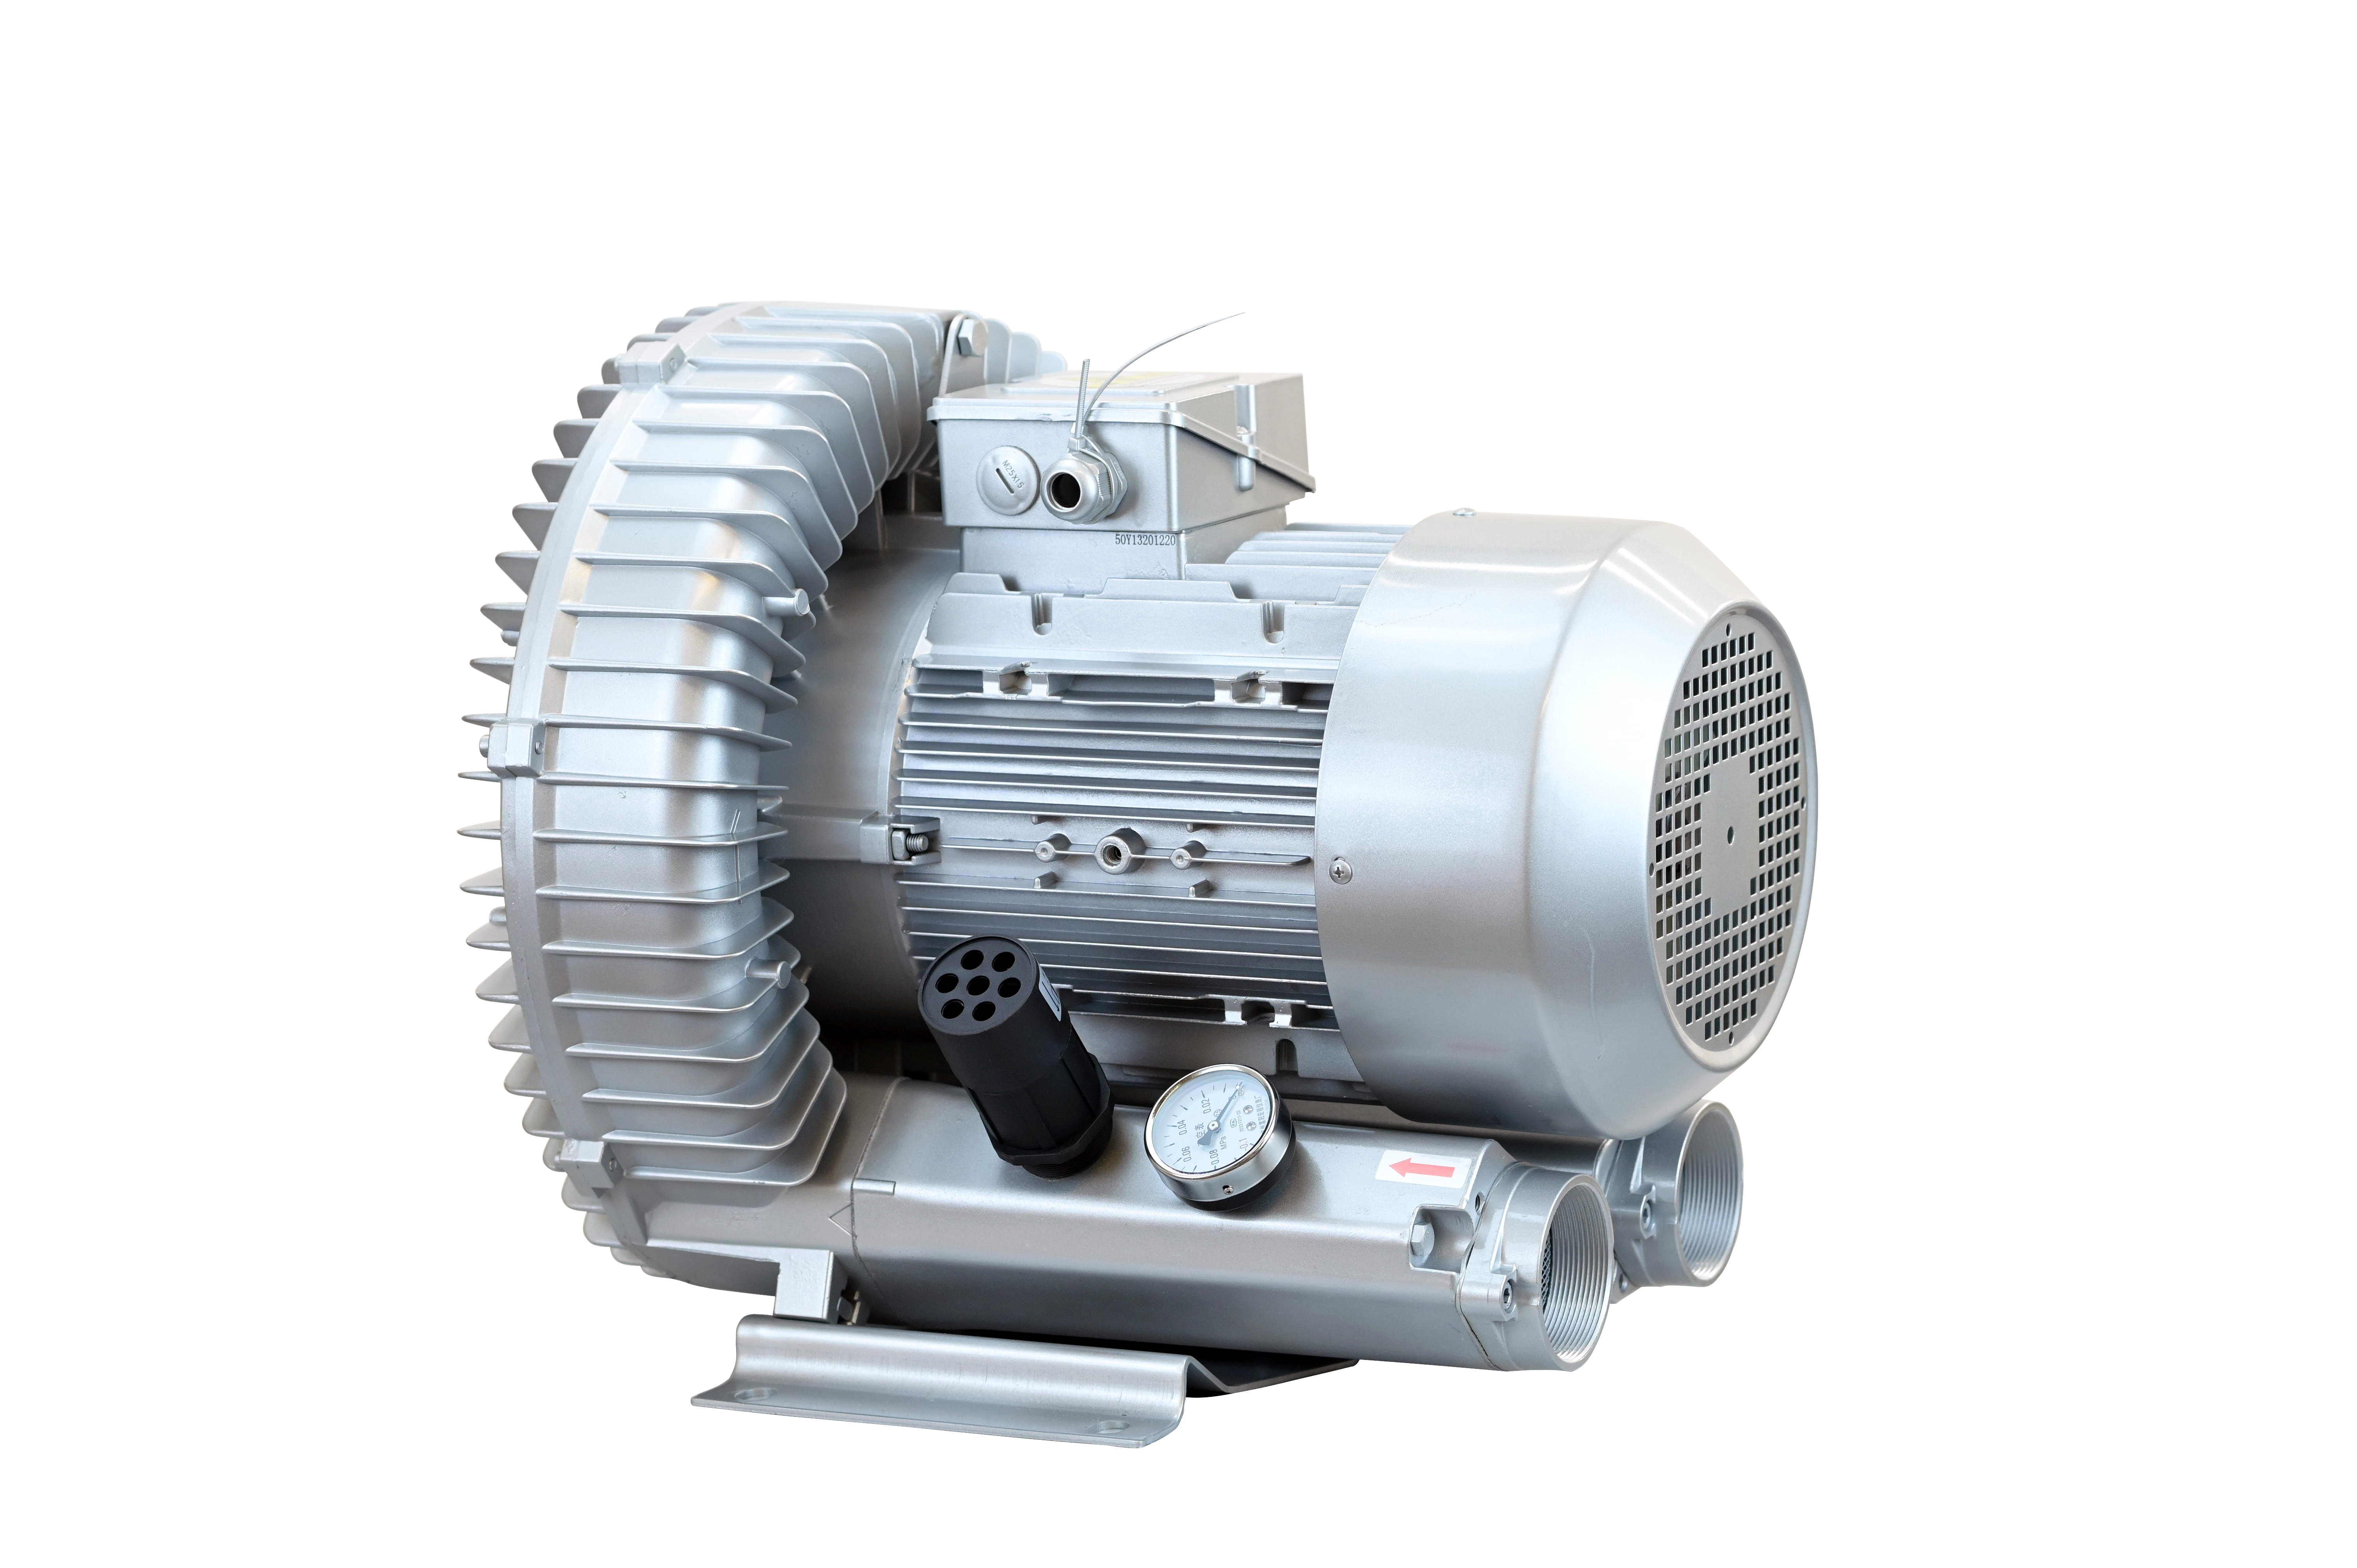
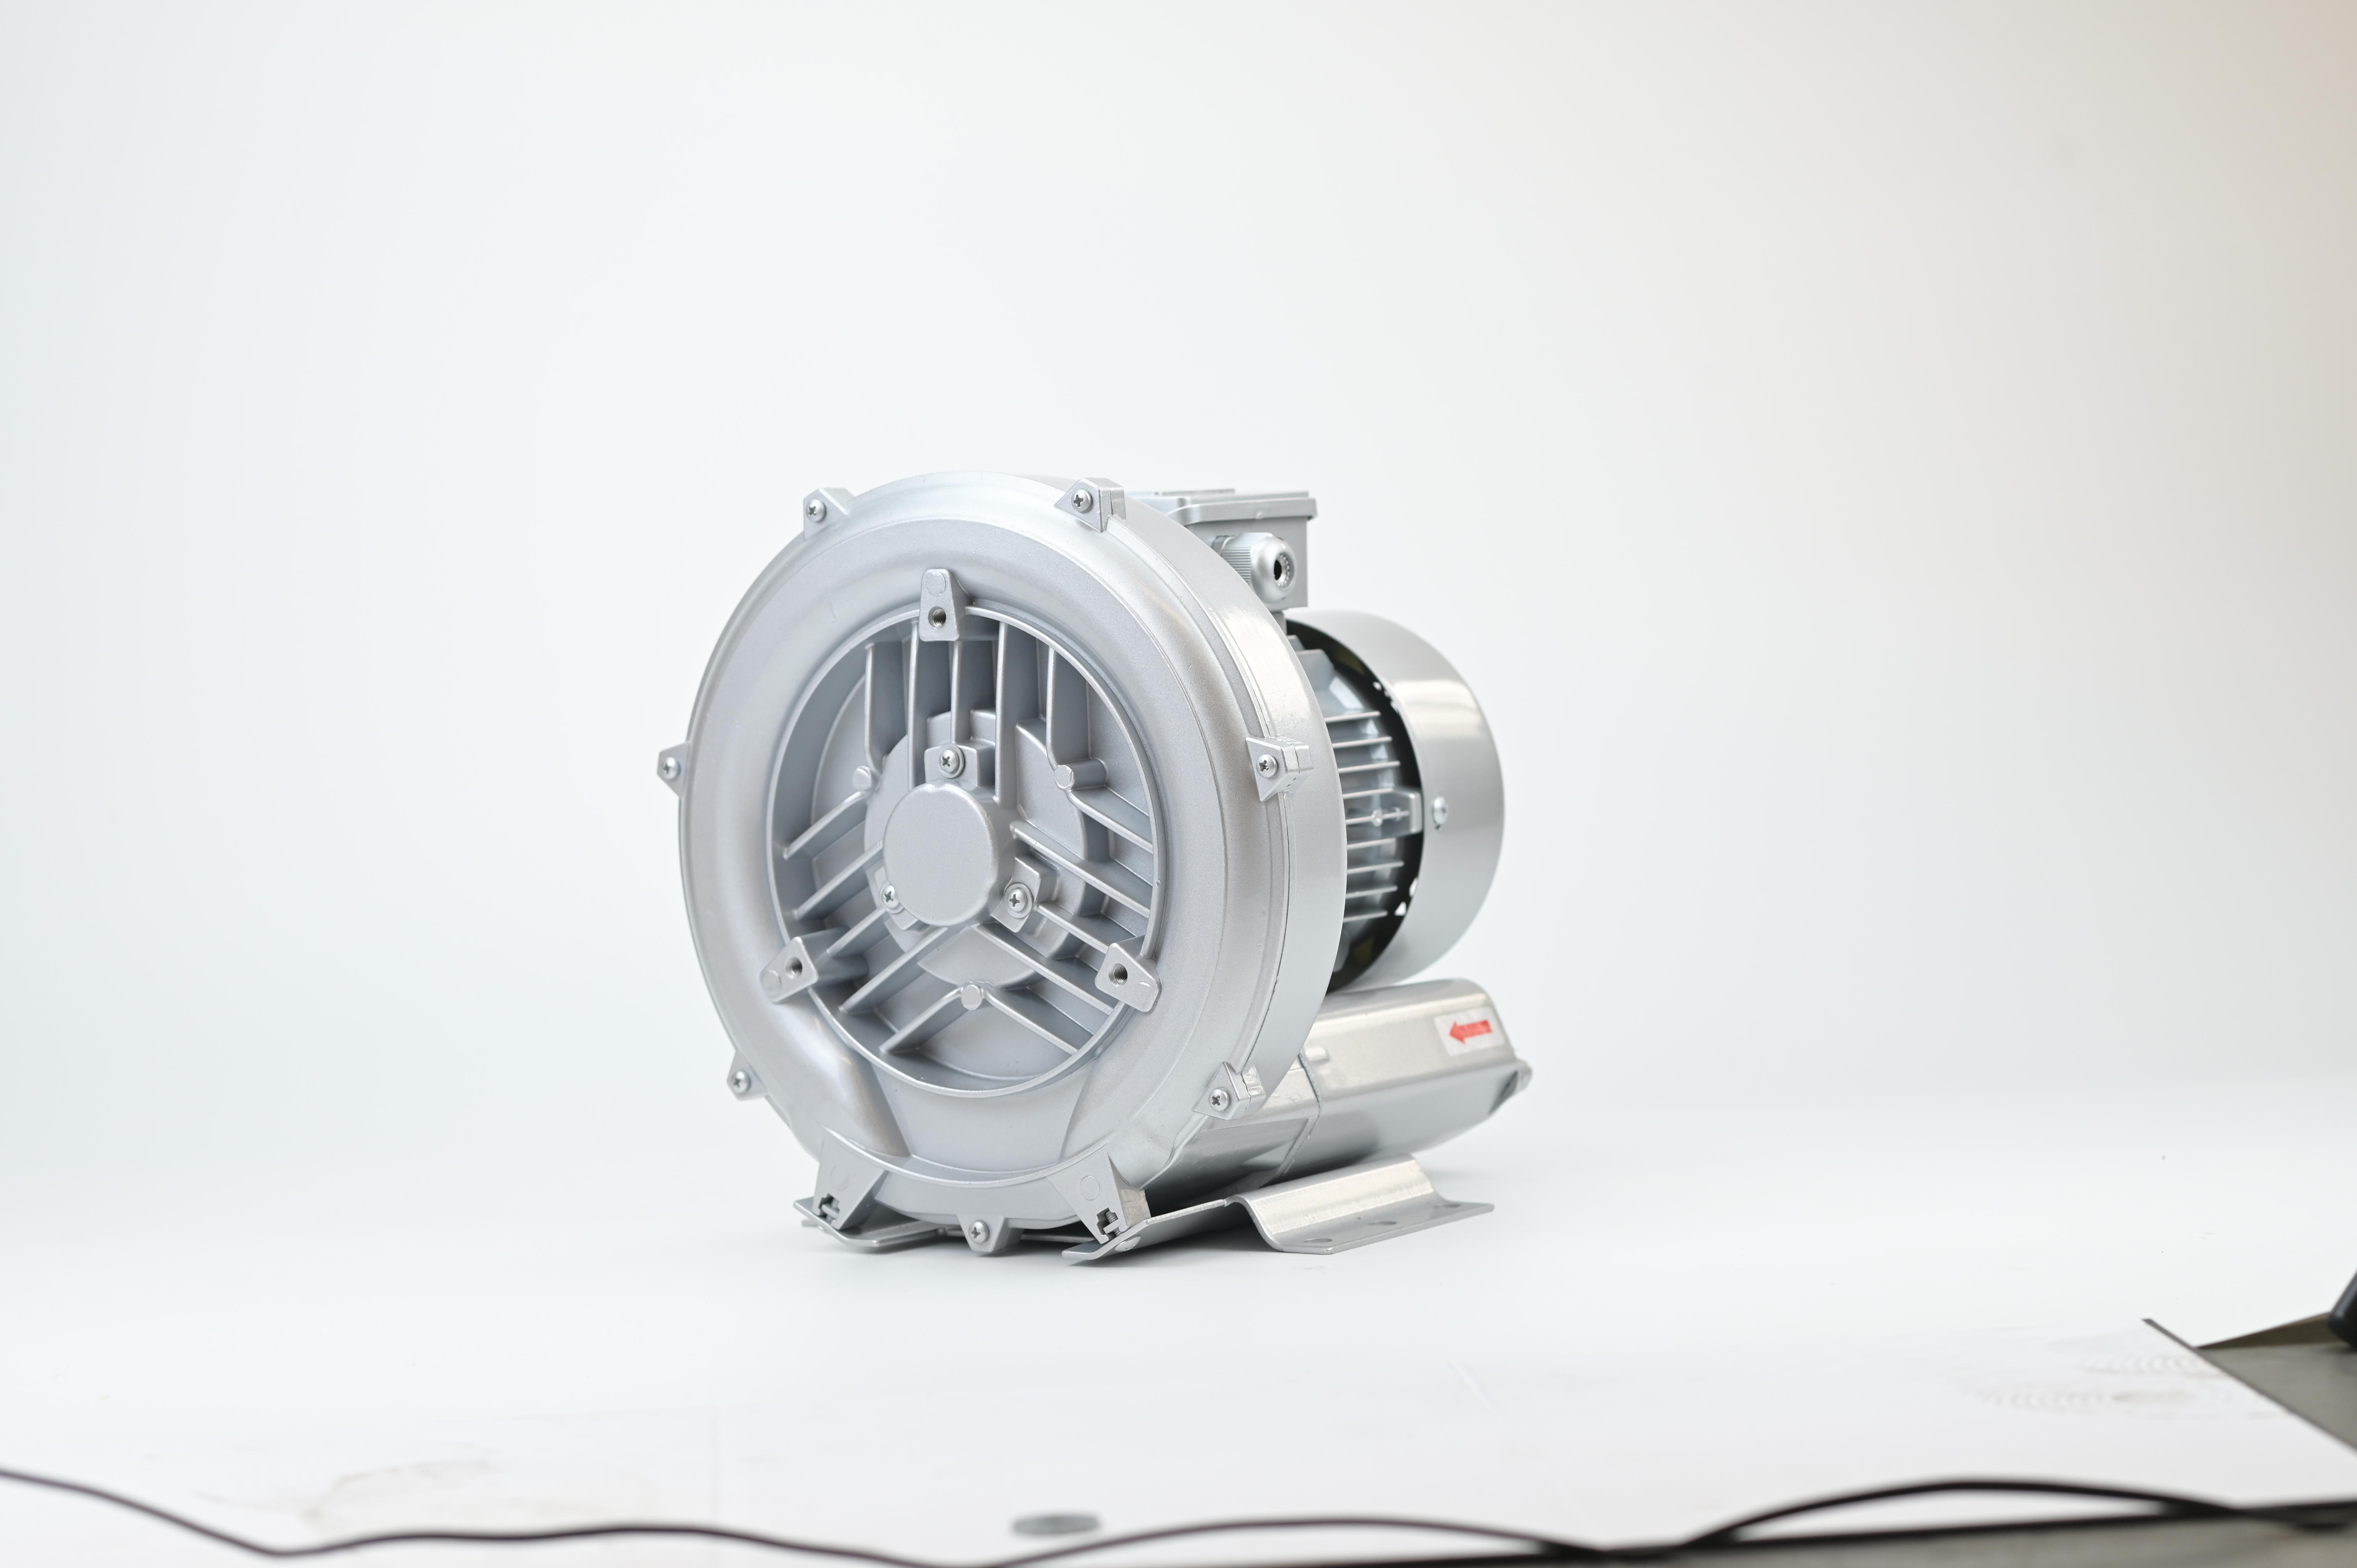
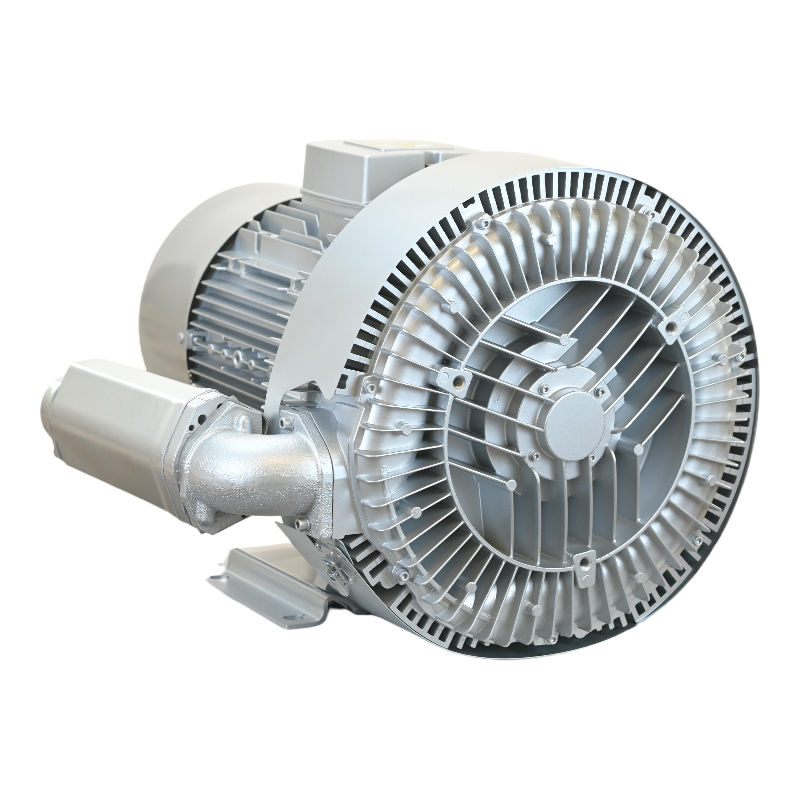
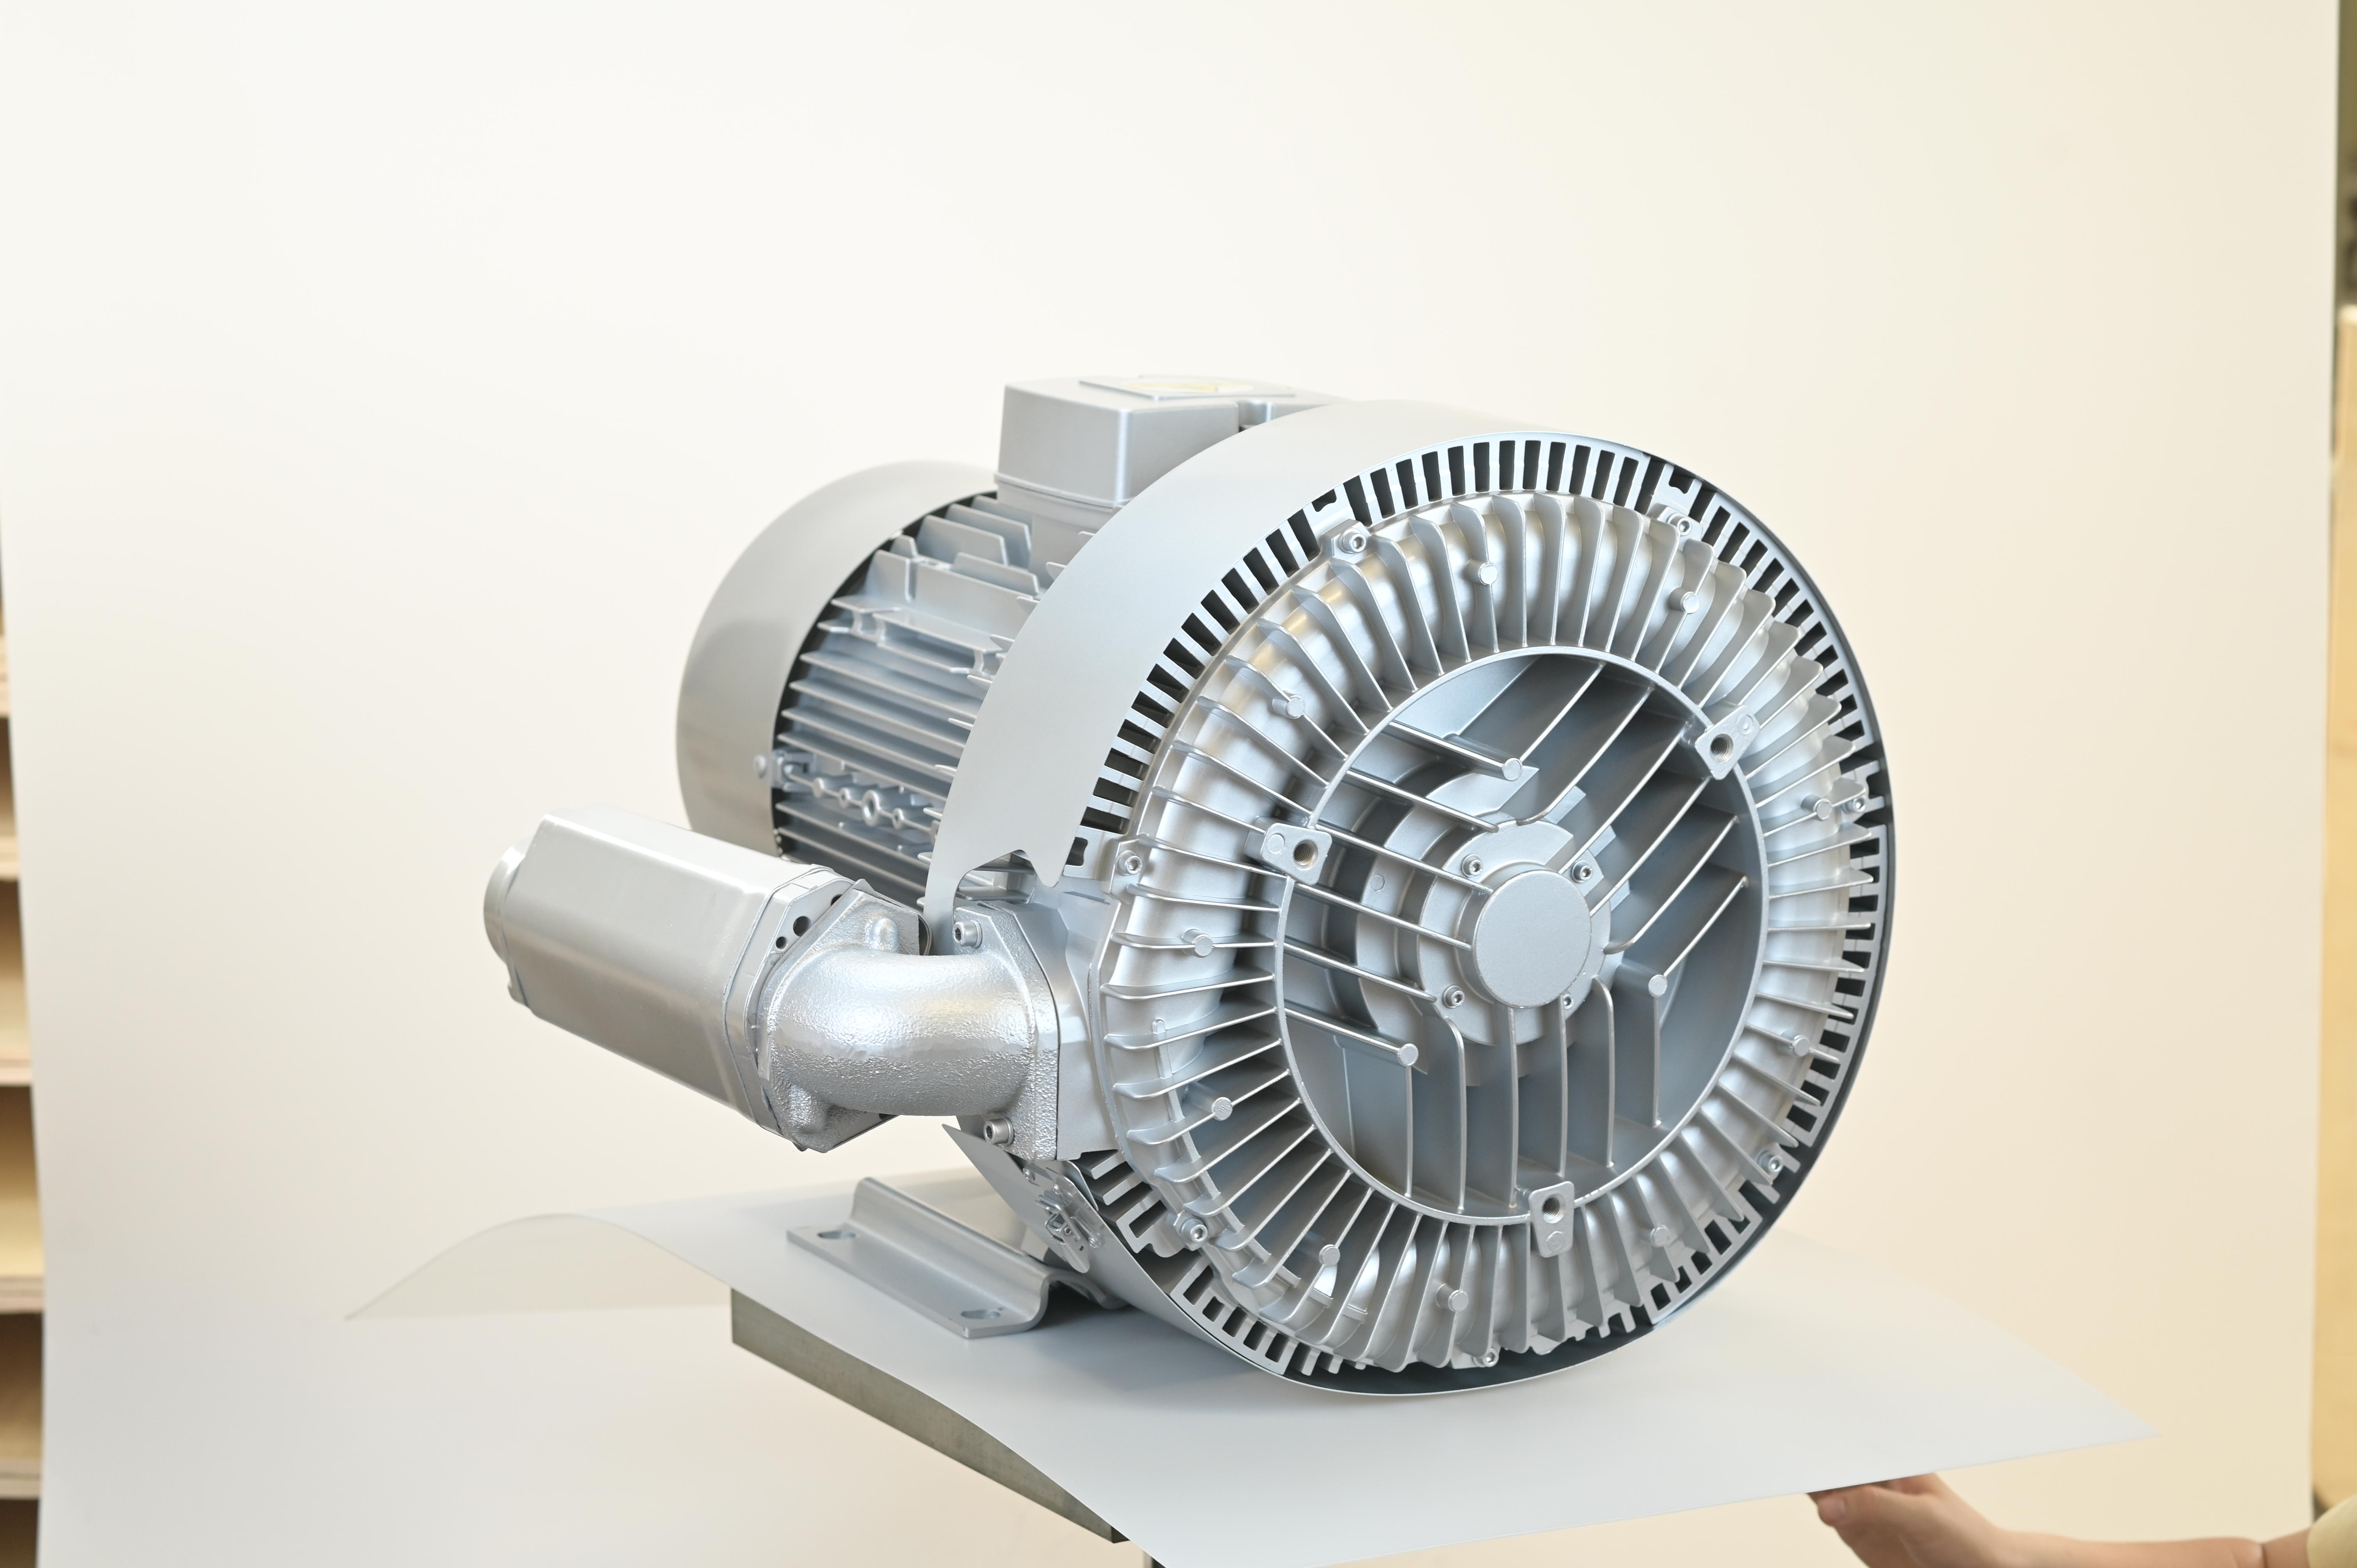
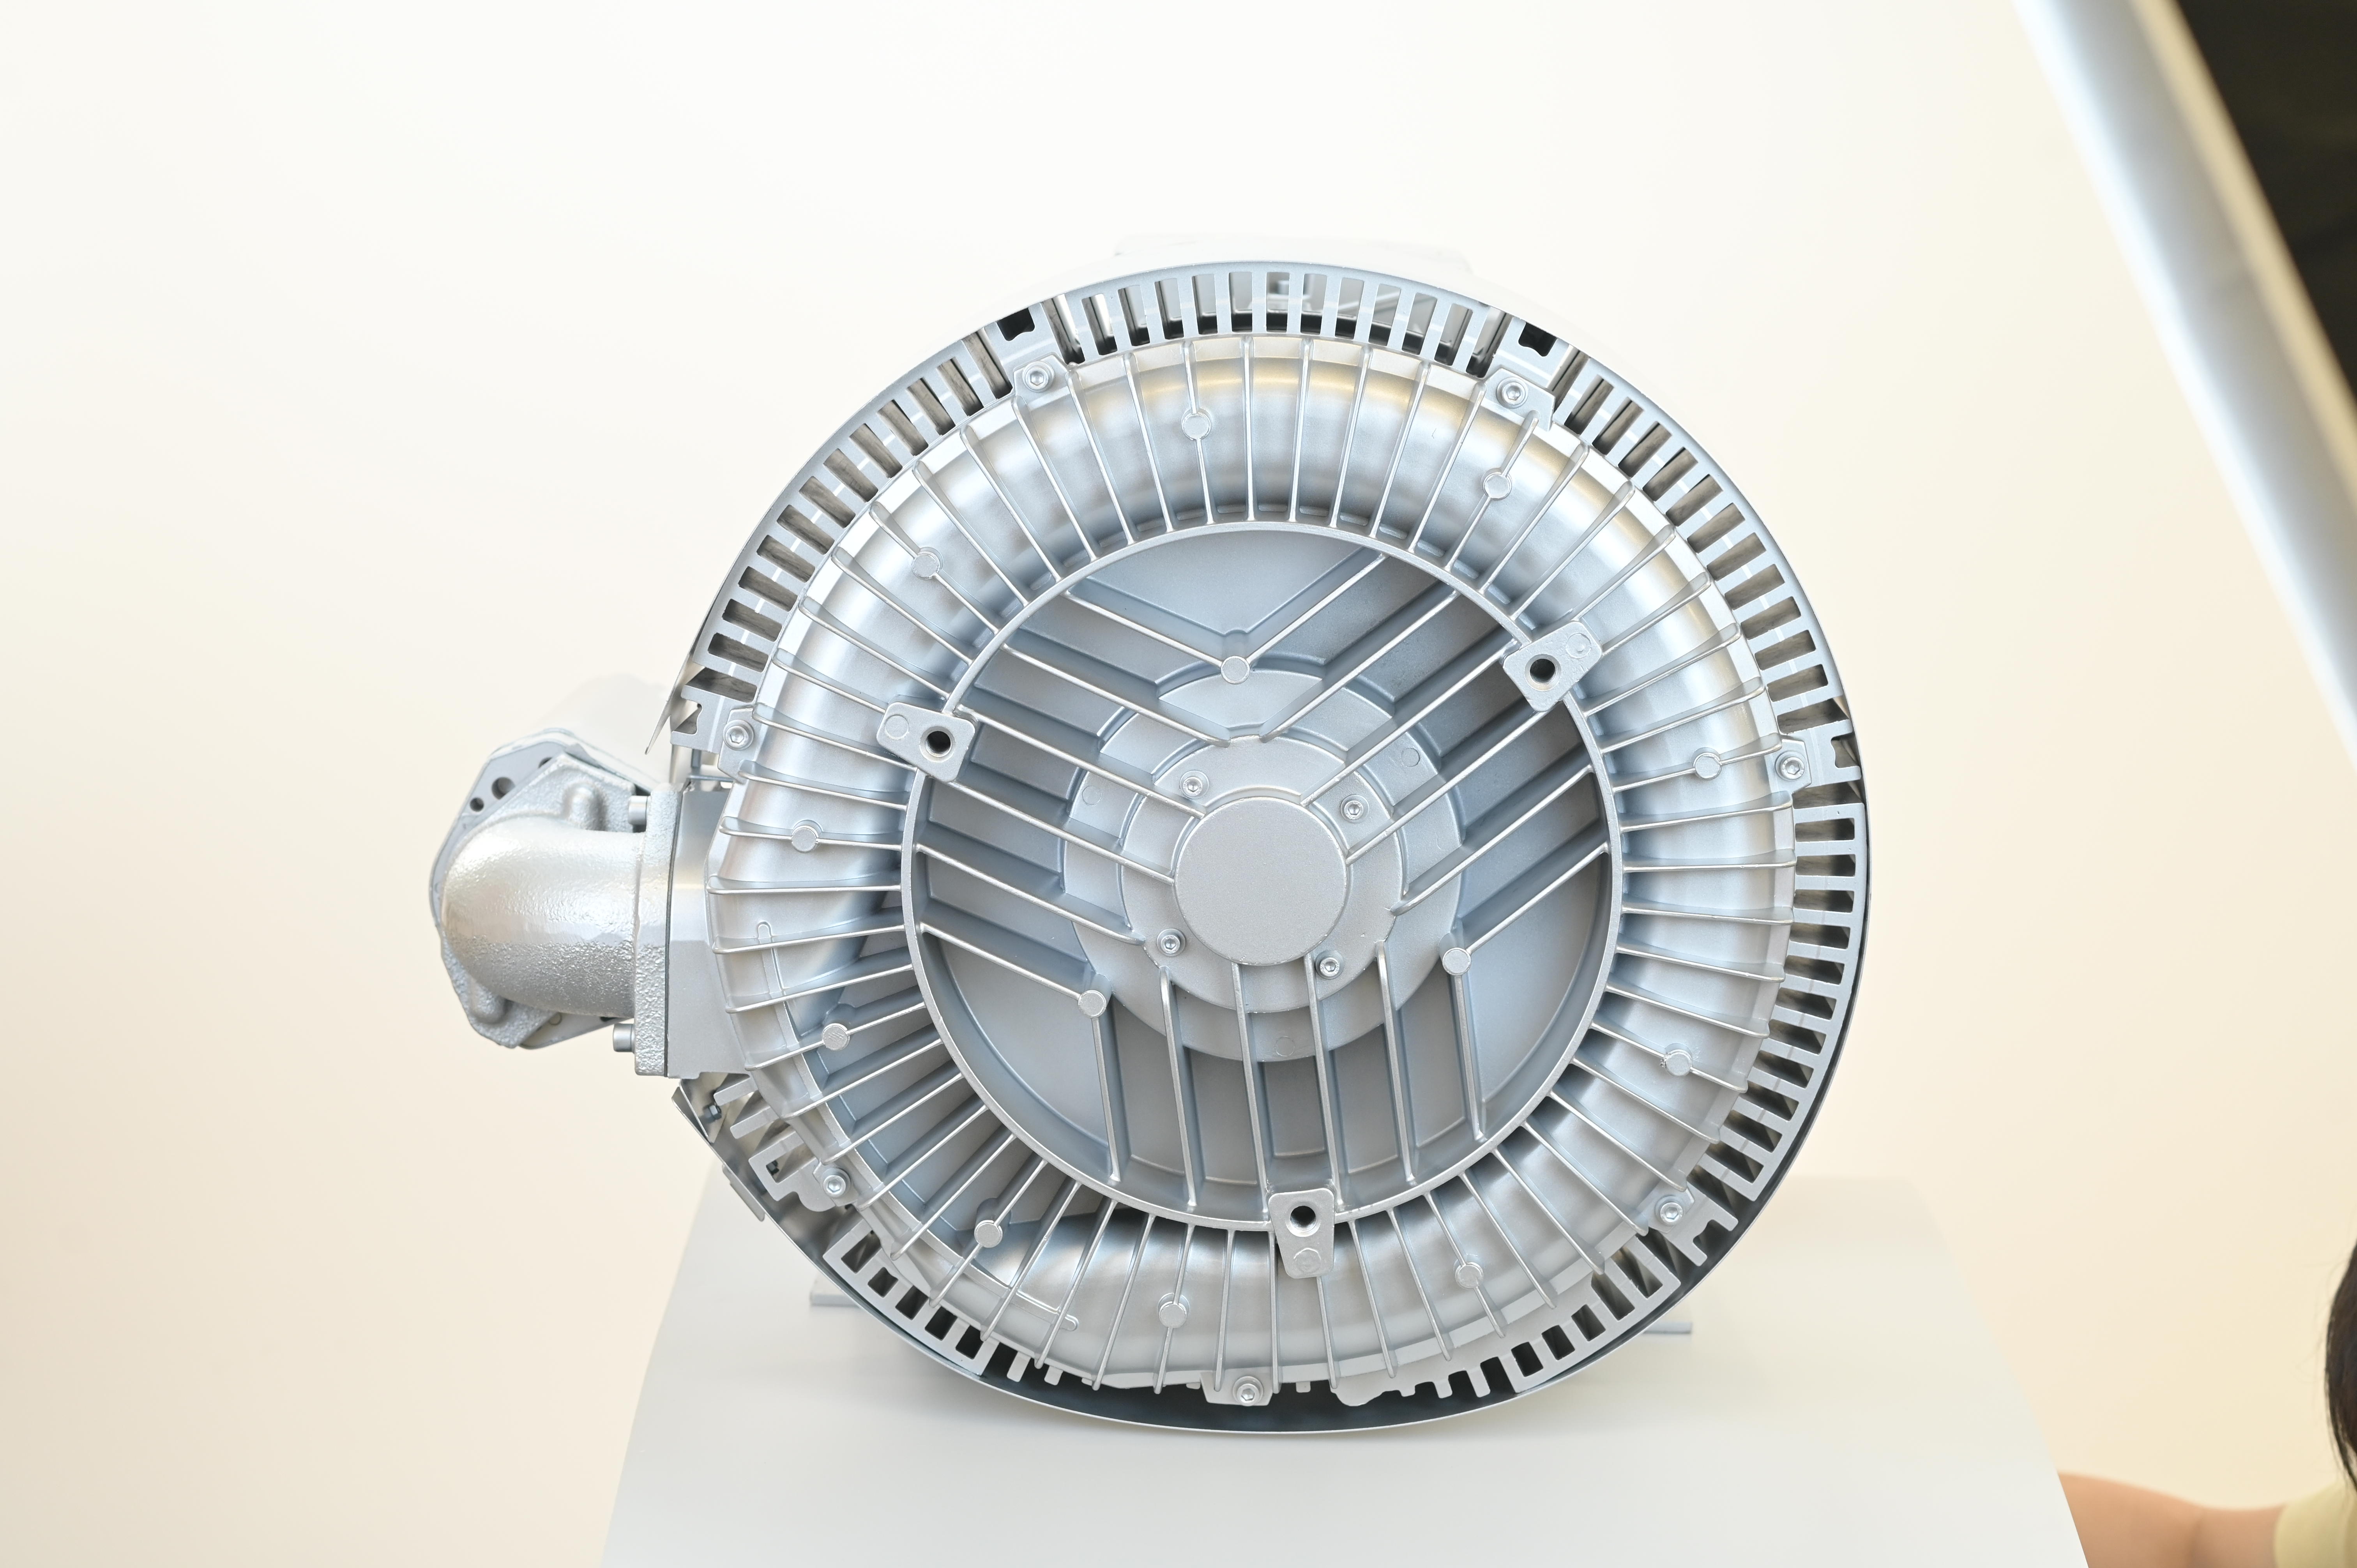
When a Swiss pharmaceutical plant needed to prevent cross-contamination in their freeze-drying line, off-the-shelf oil-sealed pumps were a non-starter due to hydrocarbon risks. Our Cleanroom Dry Vacuum Pump—featuring dry screw technology​ and PTFE-coated rotors—delivered a cleanroom-compatible vacuum with zero oil vapor backstreaming, helping them achieve EU GMP compliance.Since 2007, Jinan Golden Bridge Precision Machinery Co., Ltd. has leveraged over 15 years of expertise to engineer vacuum equipment that meets the stringent demands of semiconductor manufacturing, pharmaceuticals, and biotechnology.Unlike conventional systems, our pumps utilize advanced filtration systems​ to capture particulates, maintaining a clean atmosphere crucial for sensitive applications while reducing energy consumption through innovative, optimized designs.Every unit is CE certified, assembled under ISO 9001​ controls
Get A Quote

Why Choose Our Vacuum Pumps for Clean Rooms?

Unmatched Precision and Reliability

Our vacuum pumps are engineered to deliver unparalleled precision, ensuring that your clean room maintains the required levels of cleanliness and operational efficiency. With advanced technology and rigorous testing, our pumps provide consistent performance, minimizing downtime and enhancing productivity.

Energy Efficiency and Cost-Effectiveness

Designed with energy-saving features, our vacuum pumps help reduce operational costs while maintaining high performance. This makes them an ideal choice for clean room applications where efficiency is paramount. By using our pumps, you can achieve significant savings on energy bills without compromising on quality.

Comprehensive Support and Customization

We understand that every clean room has unique requirements. Our expert team offers tailored solutions and comprehensive support throughout your purchasing journey. From initial consultation to after-sales service, we ensure that you receive the best vacuum pump suited to your specific needs.

Related products

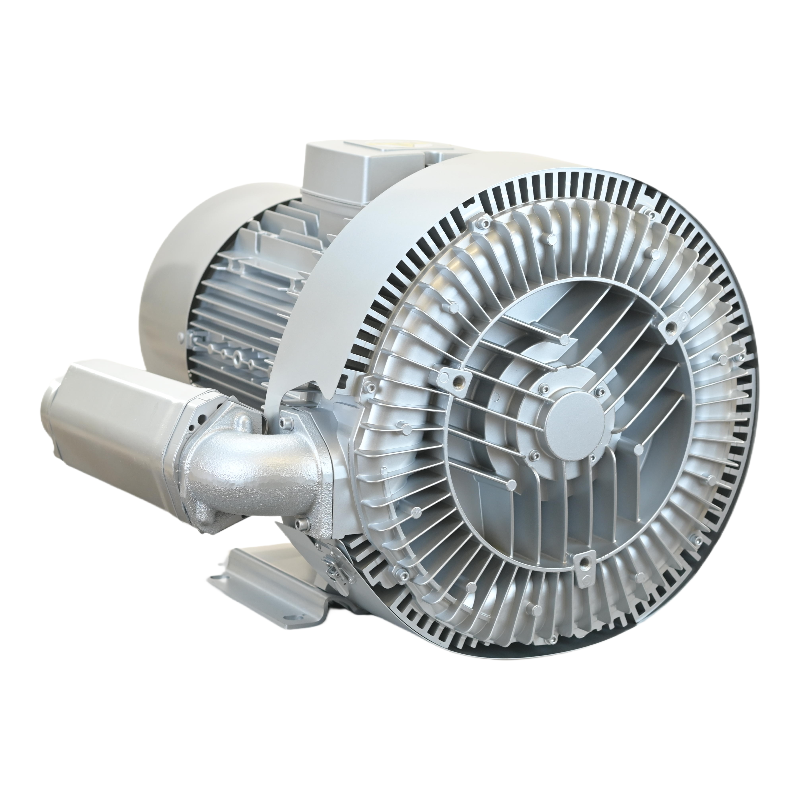
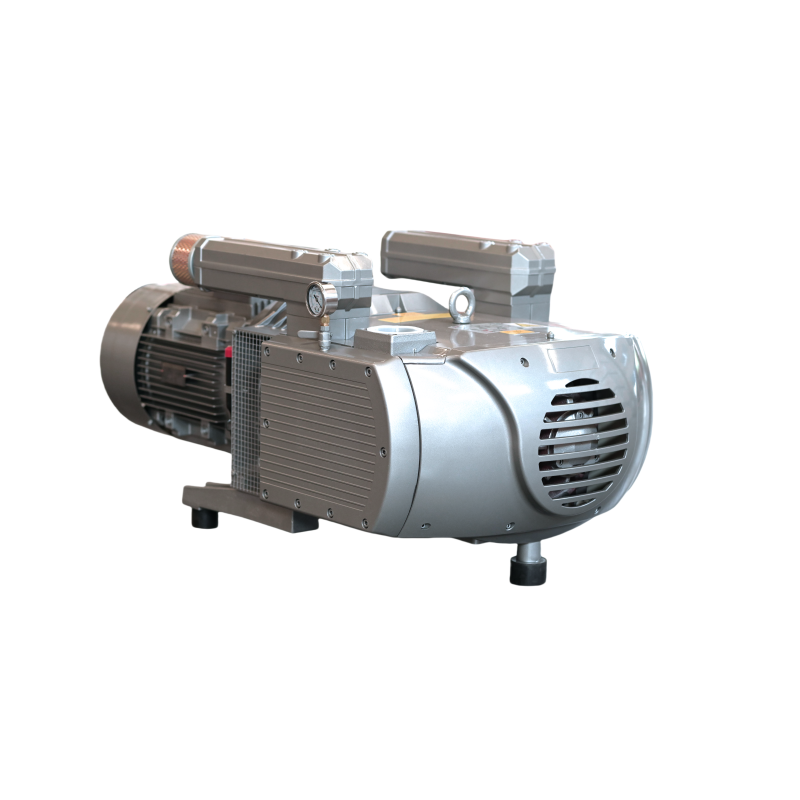
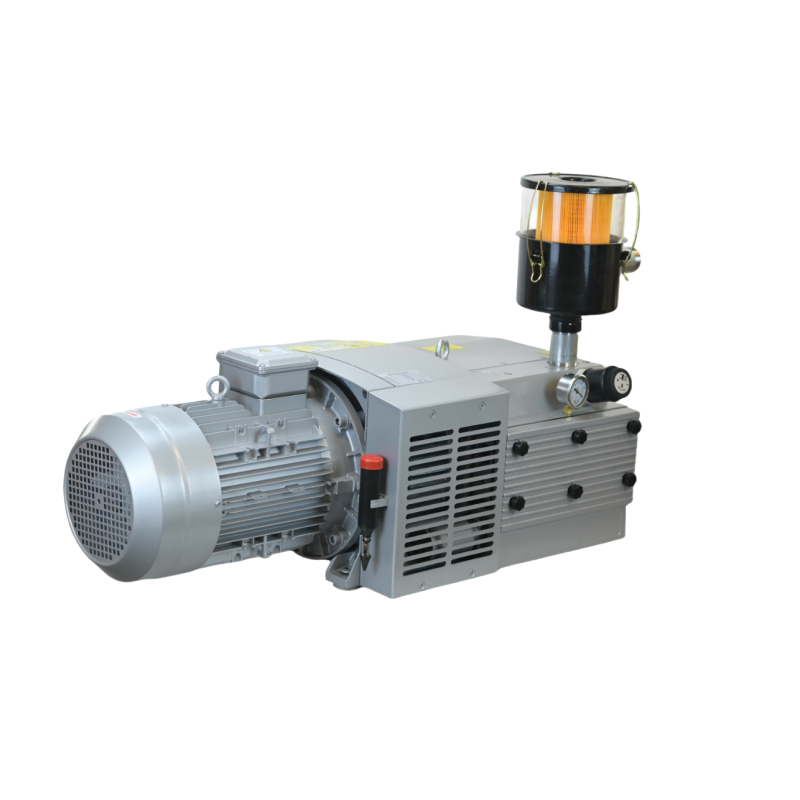
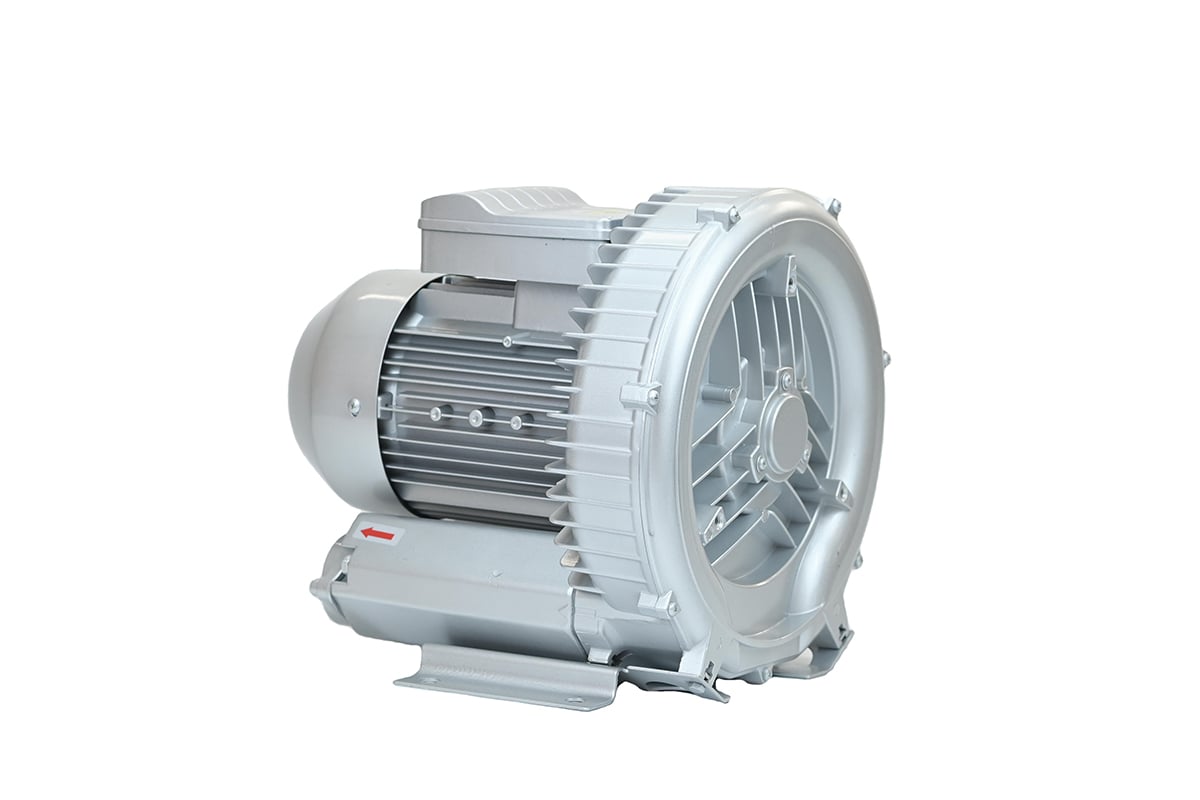
Keeping contamination at bay is critical in clean rooms. Processes and products in the rooms require high levels of integrity that brought the creation of filtration systems that reduce vibrations. Only the best vacuum pumps for clean rooms should be used. They relieve pressure and get rid of contaminations. Our customers in the clean room vacuum pumps industry rave about our dry vane and oil vacuum pumps. They are unmatched in the deep levels of vacuum that they can achieve while also producing little to no particles. They are essential in the pharmaceutical and semiconductor industry. Even the smallest particle contaminate can lead to irreplaceable losses. Ensure the competence of your clean room with our vacuum pumps.

Frequently Asked Questions about Vacuum Pumps for Clean Rooms

What types of vacuum pumps are suitable for clean room applications?

Our range includes dry vane vacuum pumps and oil vacuum pumps, both designed to meet the stringent requirements of clean room environments.
Factors such as the required vacuum level, volume flow rate, and specific application needs should be considered. Our team can assist in selecting the best option for your requirements.

Related article

Vortex Vacuum Pumps: Oil-Free, Energy-Efficient Solutions for Industrial Applications

24

Nov

Vortex Vacuum Pumps: Oil-Free, Energy-Efficient Solutions for Industrial Applications

Discover oil-free, 30-50% more energy-efficient vortex vacuum pumps ideal for semiconductors, medical, and food packaging. Zero contamination, low noise, global support. Request a quote today.
View More
What Are the Energy-Saving Technologies Applied in Modern Industrial Air Compressors?

22

Dec

What Are the Energy-Saving Technologies Applied in Modern Industrial Air Compressors?

Cut compressor energy costs by up to 35%—discover VSD, heat recovery, smart controls & more. Learn proven efficiency upgrades for manufacturers. Download the tech guide now.
View More
What Factors Influence the Energy Efficiency of Air Blowers in Industrial Settings?

13

Mar

What Factors Influence the Energy Efficiency of Air Blowers in Industrial Settings?

What really drives energy waste in industrial air blowers? Discover 7 key technical & operational factors—and cut energy costs by up to 40%. Download the efficiency checklist now.
View More
Why Do Industrial Air Compressors Require Regular Air Filter Replacement?

25

Dec

Why Do Industrial Air Compressors Require Regular Air Filter Replacement?

Neglecting air filter replacement risks downtime, energy waste, and costly repairs. Learn how regular maintenance boosts efficiency & extends compressor life—download our maintenance checklist now.
View More

Customer Testimonials on Our Vacuum Pumps

John Smith
Reliable Performance in Critical Environments

We have been using Jinan Golden Bridge’s vacuum pumps in our semiconductor clean room for over five years. Their reliability and performance have been outstanding, significantly reducing our downtime.

Sarah Johnson
Exceptional Customer Support

The team at Jinan Golden Bridge provided us with tailored solutions for our clean room needs. Their expertise and support were invaluable, making the entire process seamless.

Get a Quote & Connect With Our Engineering Team

Searching for reliable industrial solutions? Let us help you find the perfect fit. Drop us a line, and our B2B technical sales team will get back to you within 12 hours (working days).
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000
Advanced Filtration Technology

Advanced Filtration Technology

When a semiconductor fab in Malaysia needed to maintain a Class 10 cleanroom​ vacuum without hydrocarbon contamination, our Cleanroom Dry Vacuum Pump—featuring multi-stage HEPA filtration​ and PTFE-coated rotors—captured 99.97% of particulates ≥0.3 µm​ while delivering zero oil vapor backstreaming, verified by TÜV-certified ISO 8573-1 Class 0​ purity. Unlike conventional oil-sealed pumps where degraded oil circulates contaminants back into the chamber, our dry screw technology​ with state-of-the-art filtration​ physically blocks particulate migration, preventing the $2.3M average loss​ from a single contaminated wafer batch. Every unit is CE certified, assembled under ISO 9001​ controls, and backed by 24/7 IoT monitoring​ that tracks filter differential pressure in real time, alerting your team before efficiency drops.
Low Noise and Vibration Design

Low Noise and Vibration Design

When a Swiss pharmaceutical lab noticed microscopic v failures in their freeze-dried vials, their root-cause analysis pointed to subtle pressure fluctuations​ from high by high-vibration pumps—each vibration pulse transmitted through the floor was enough to disrupt the delicate filling process. Our Cleanroom Dry Vacuum Pump—featuring active magnetic levitation bearings​ and a composite acoustic enclosure—operates at just 58 dB(A)​ with vibration levels below 1.0 mm/s, eliminating floor-transmitted pulses entirely. Unlike conventional belt-drive pumps that generate >75 dB(A)​ and require bulky anti-vibration mounts, our direct-drive design​ with precision-balanced rotors​ ensures smooth, whisper-quiet operation that won't compromise nearby sensitive instruments. Every unit is CE certified, assembled under ISO 9001​ controls, and tested to ISO 21360-1​ standards, with 24/7 IoT monitoring​ tracking vibration spectra in real time to predict bearing wear before it affects your process.
+86 0531 88060599
13386448931
[email protected]

Get a Quote & Connect With Our Engineering Team

Searching for reliable industrial solutions? Let us help you find the perfect fit. Drop us a line, and our B2B technical sales team will get back to you within 12 hours (working days).
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000