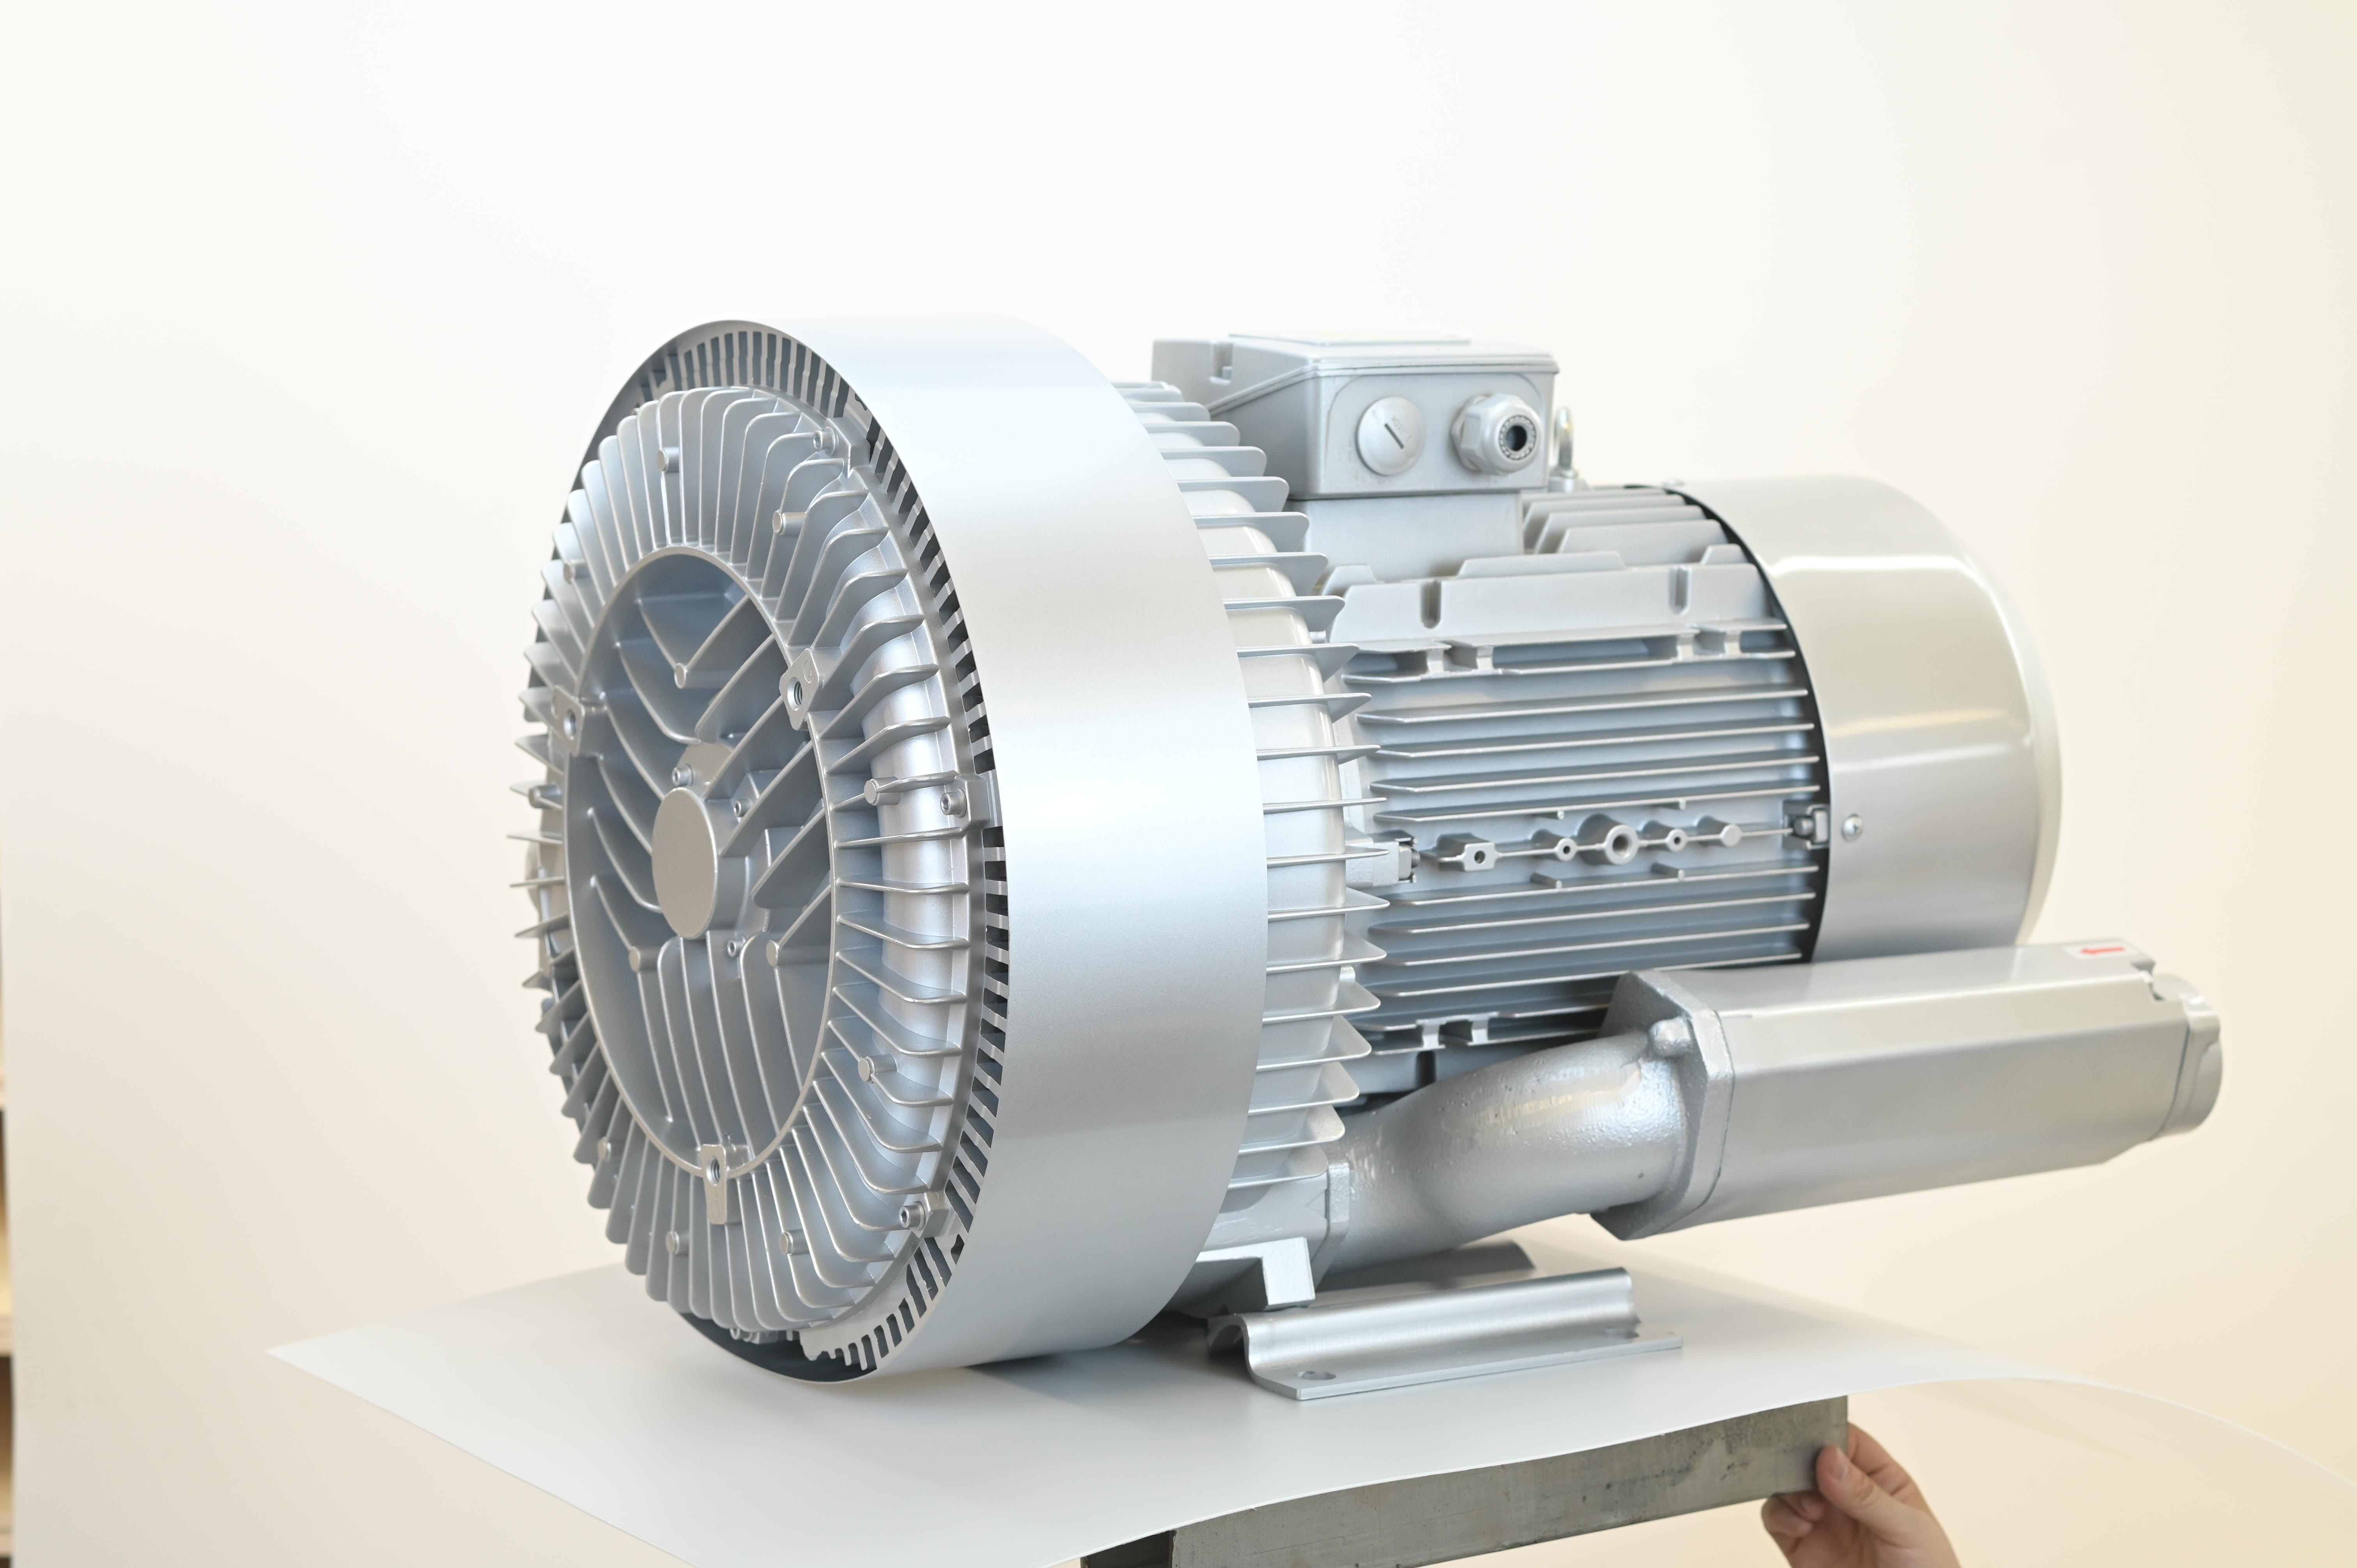
Industrial Vacuum Pump for Food: Oil-Free, FDA-Compliant Solutions

Get a Quote & Connect With Our Engineering Team

Searching for reliable industrial solutions? Let us help you find the perfect fit. Drop us a line, and our B2B technical sales team will get back to you within 12 hours (working days).
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000
Industrial Vacuum Pump for Food: Precision and Reliability

Industrial Vacuum Pump for Food: Precision and Reliability

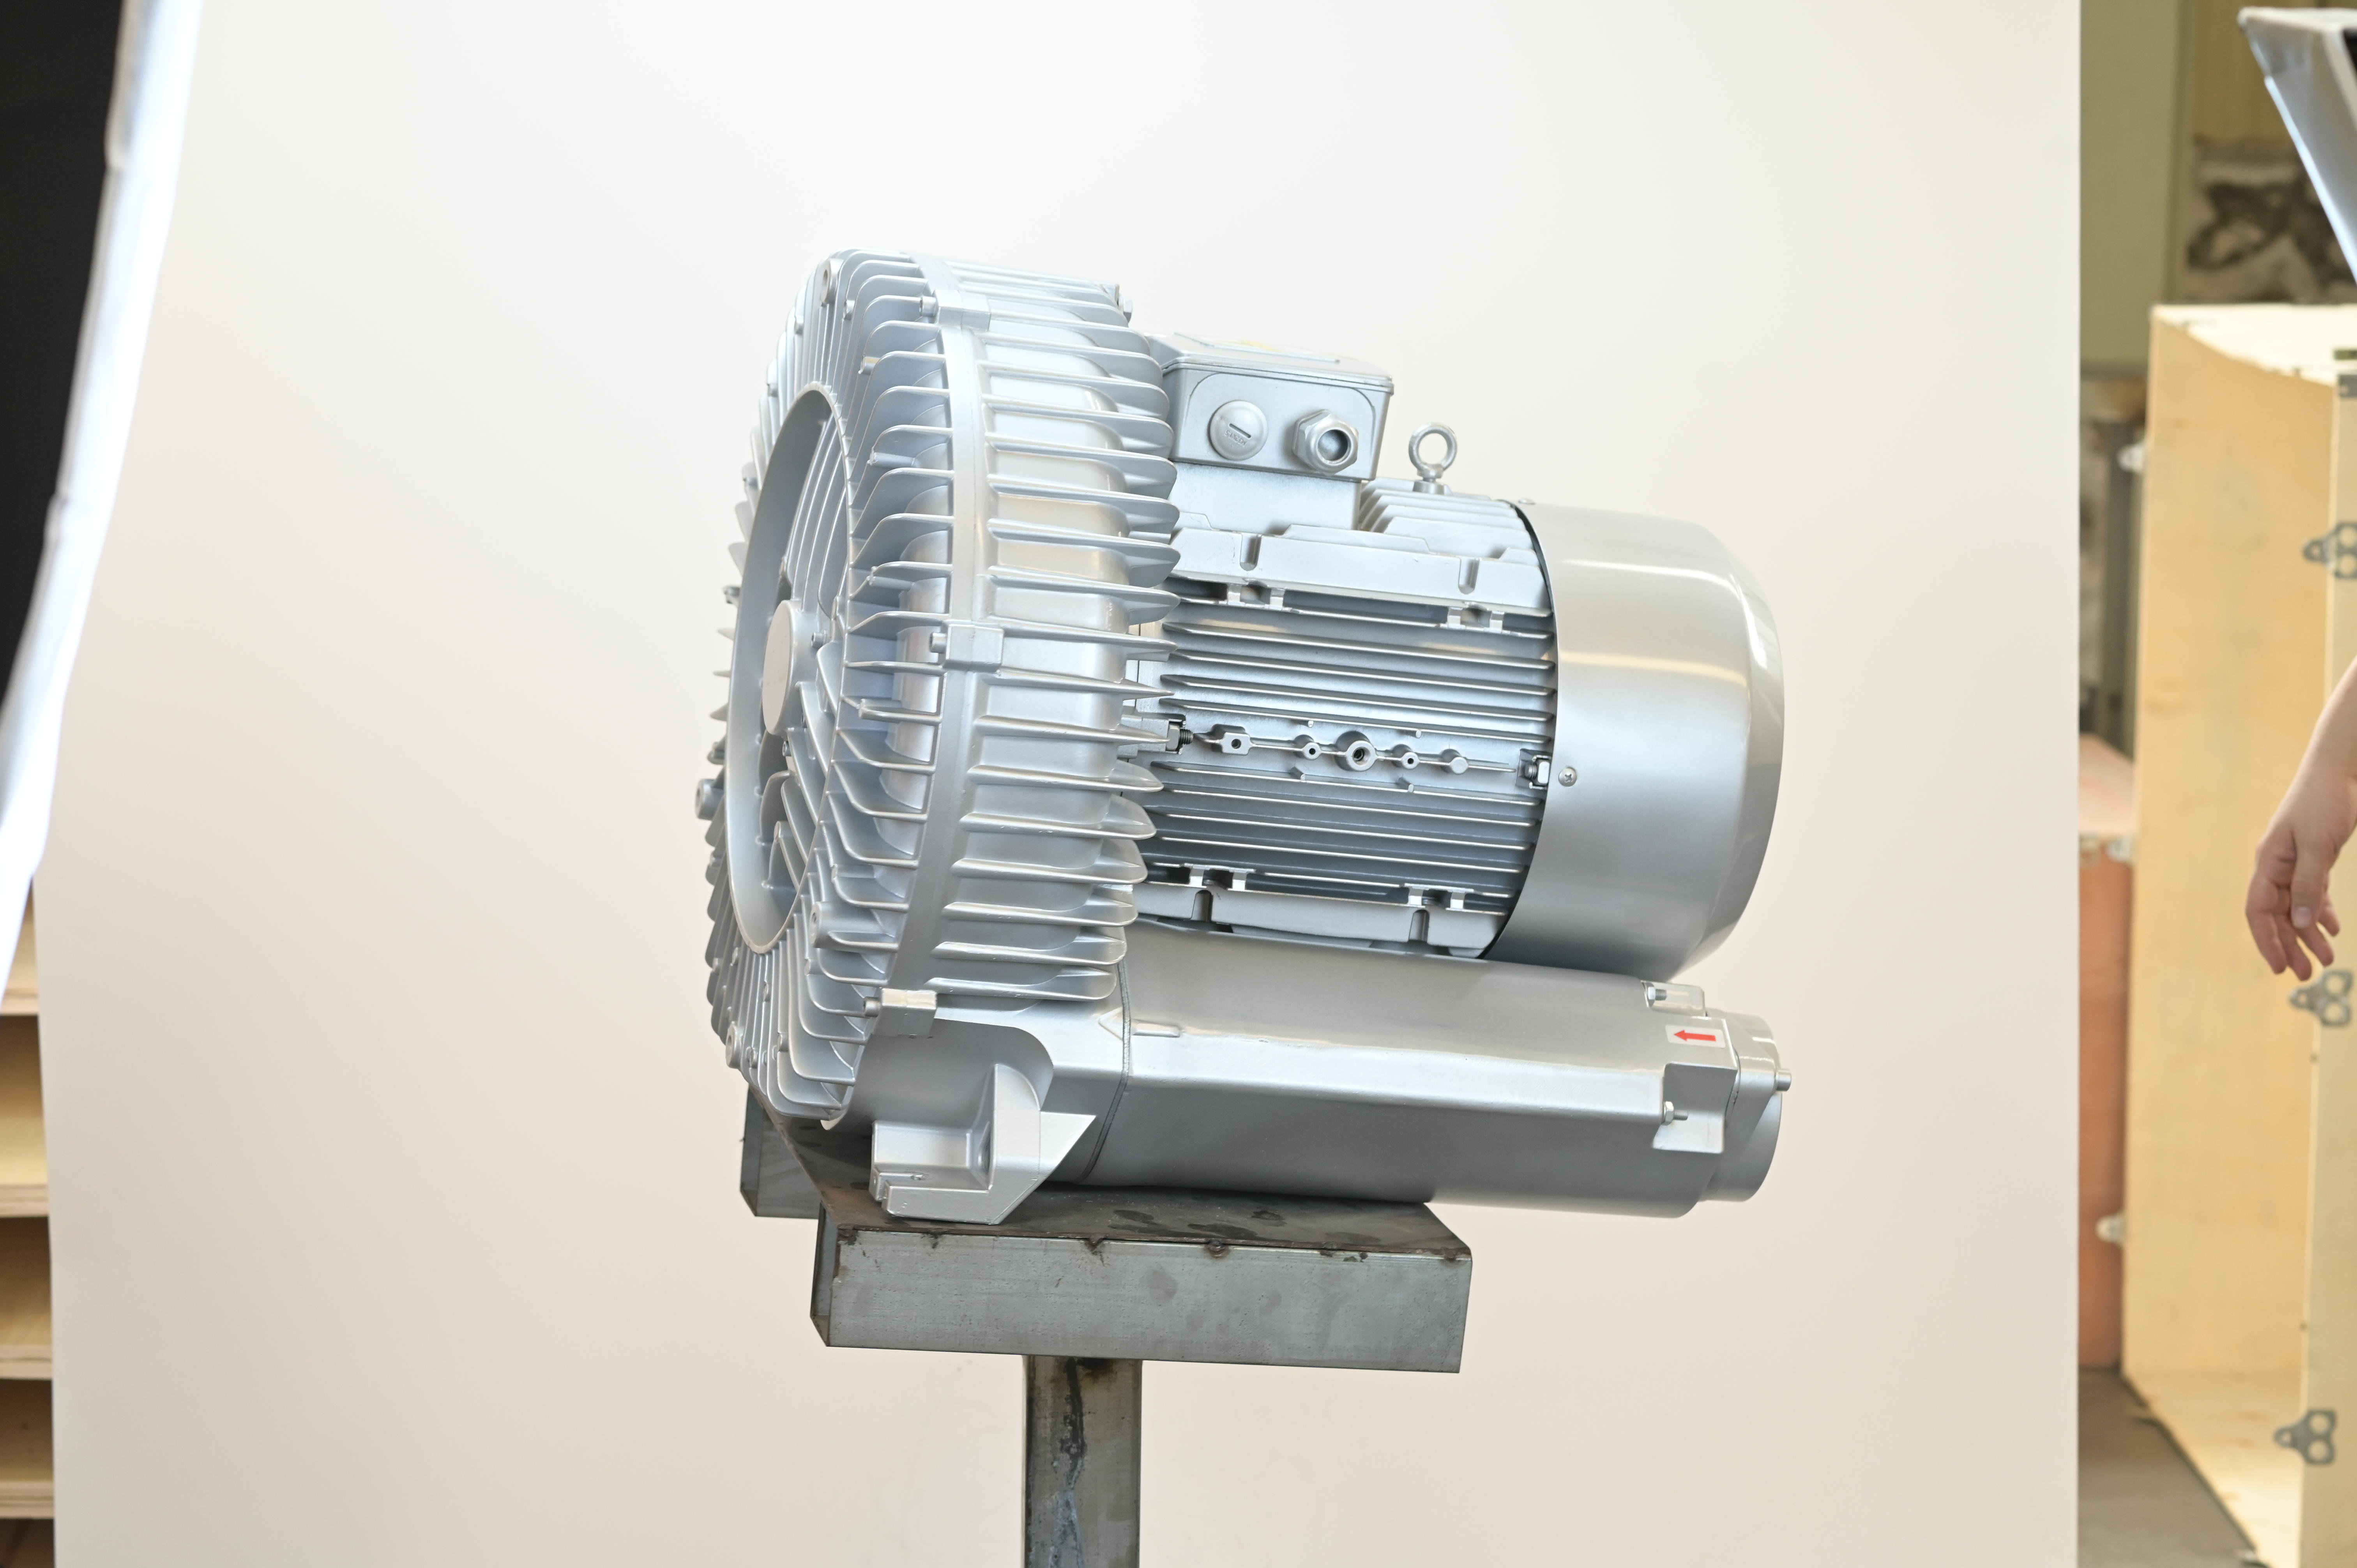
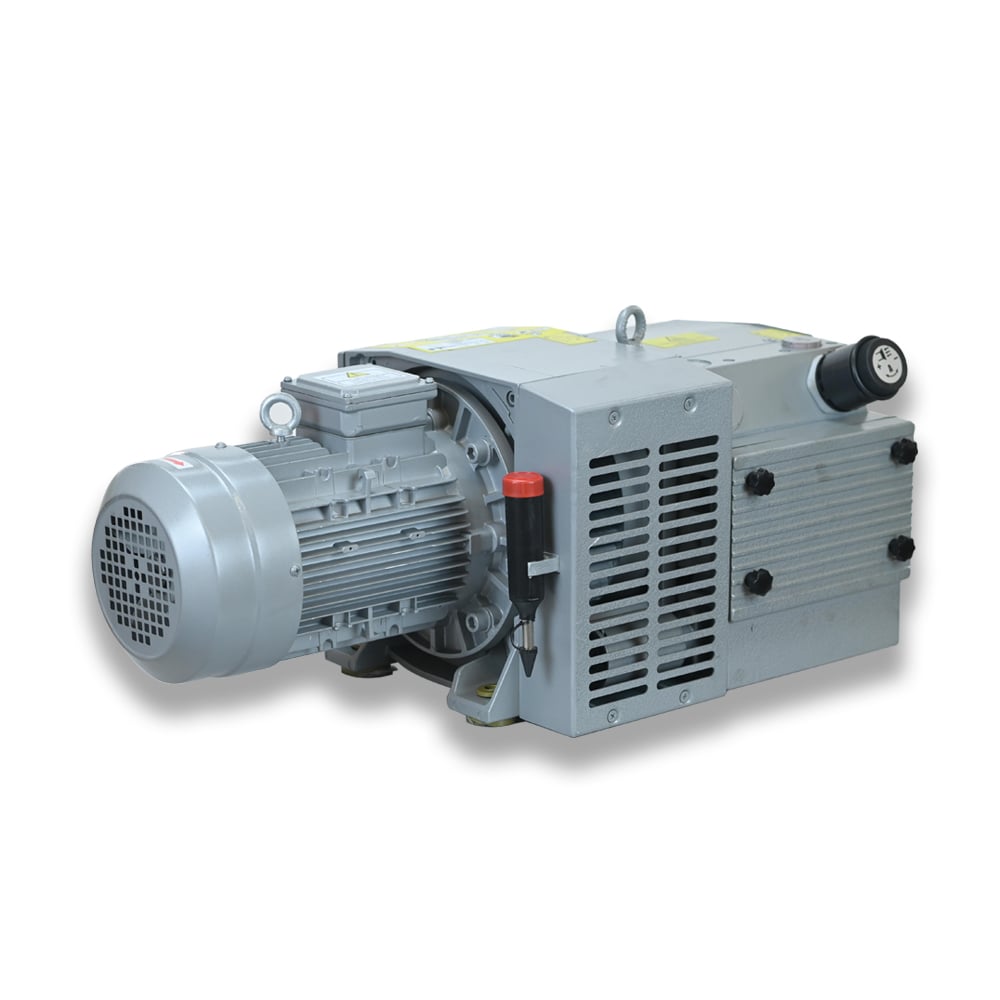
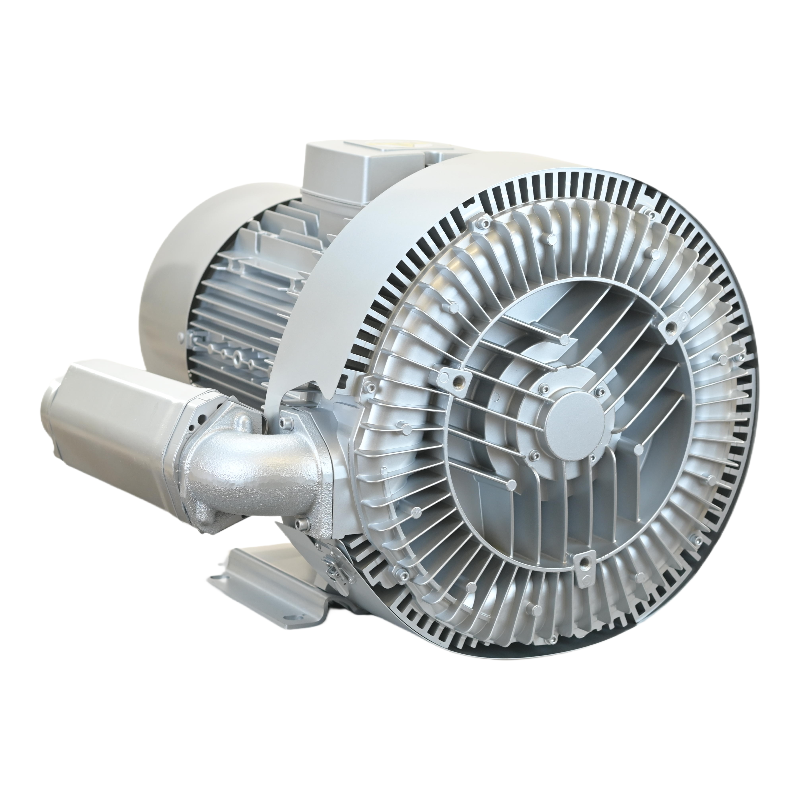
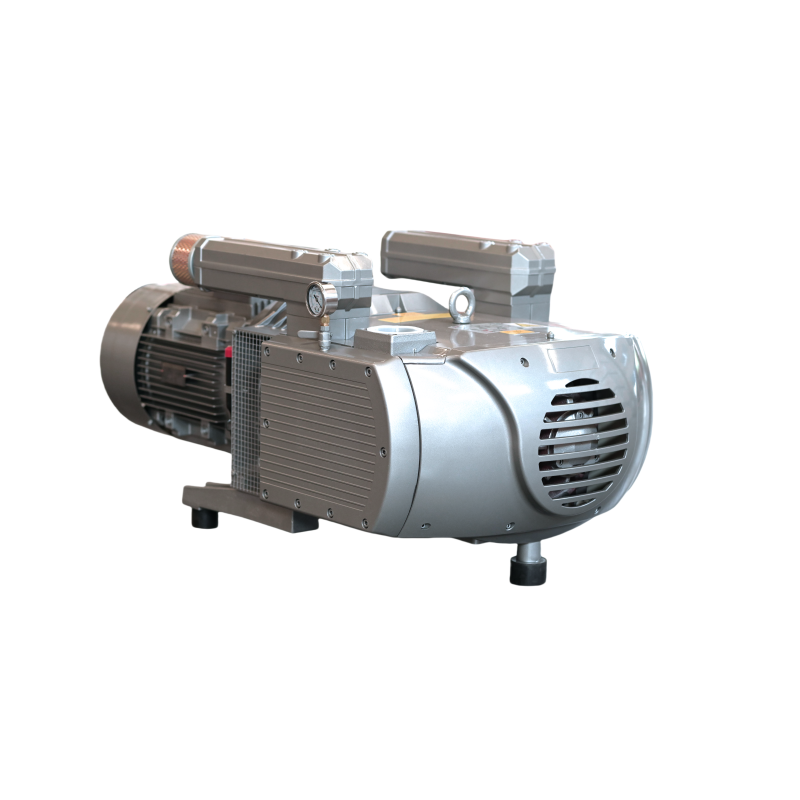
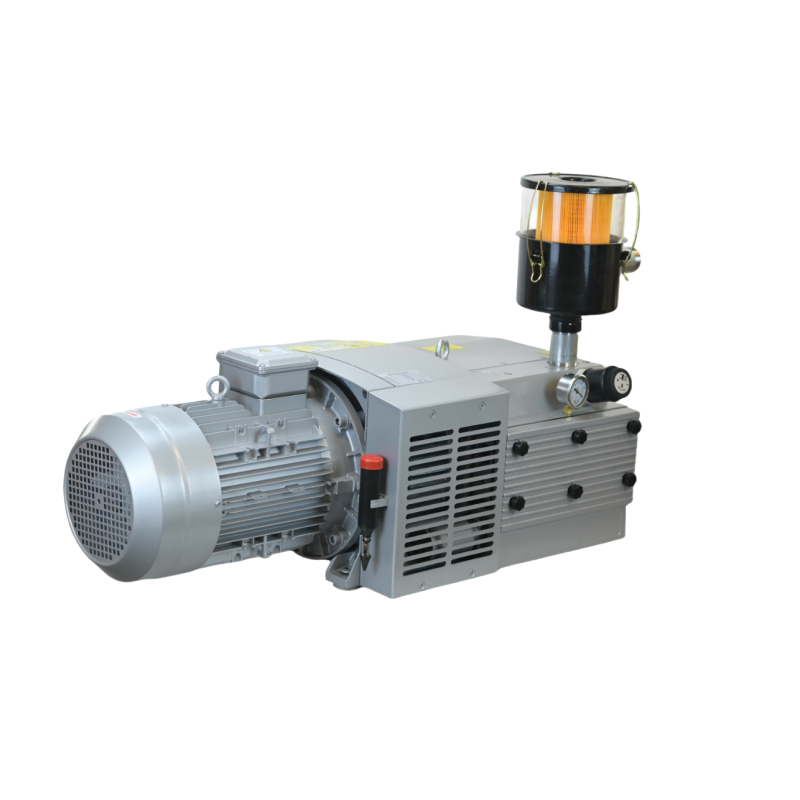
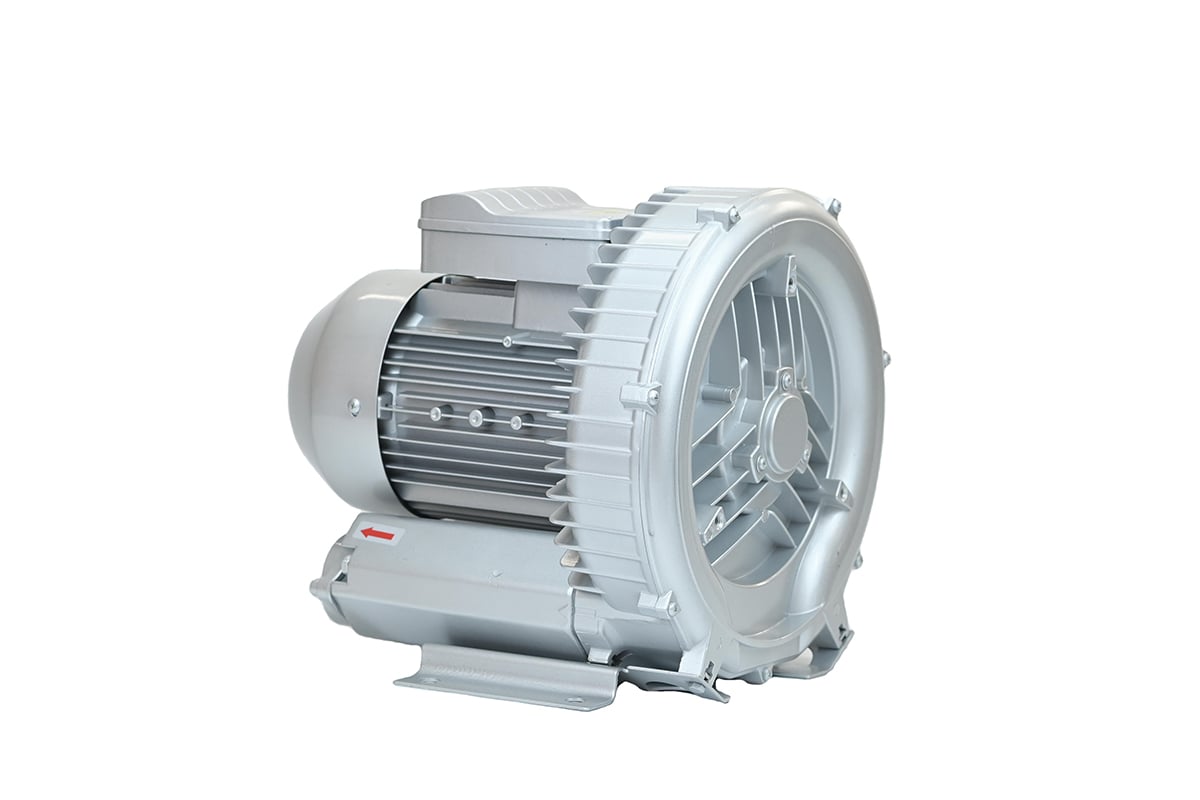
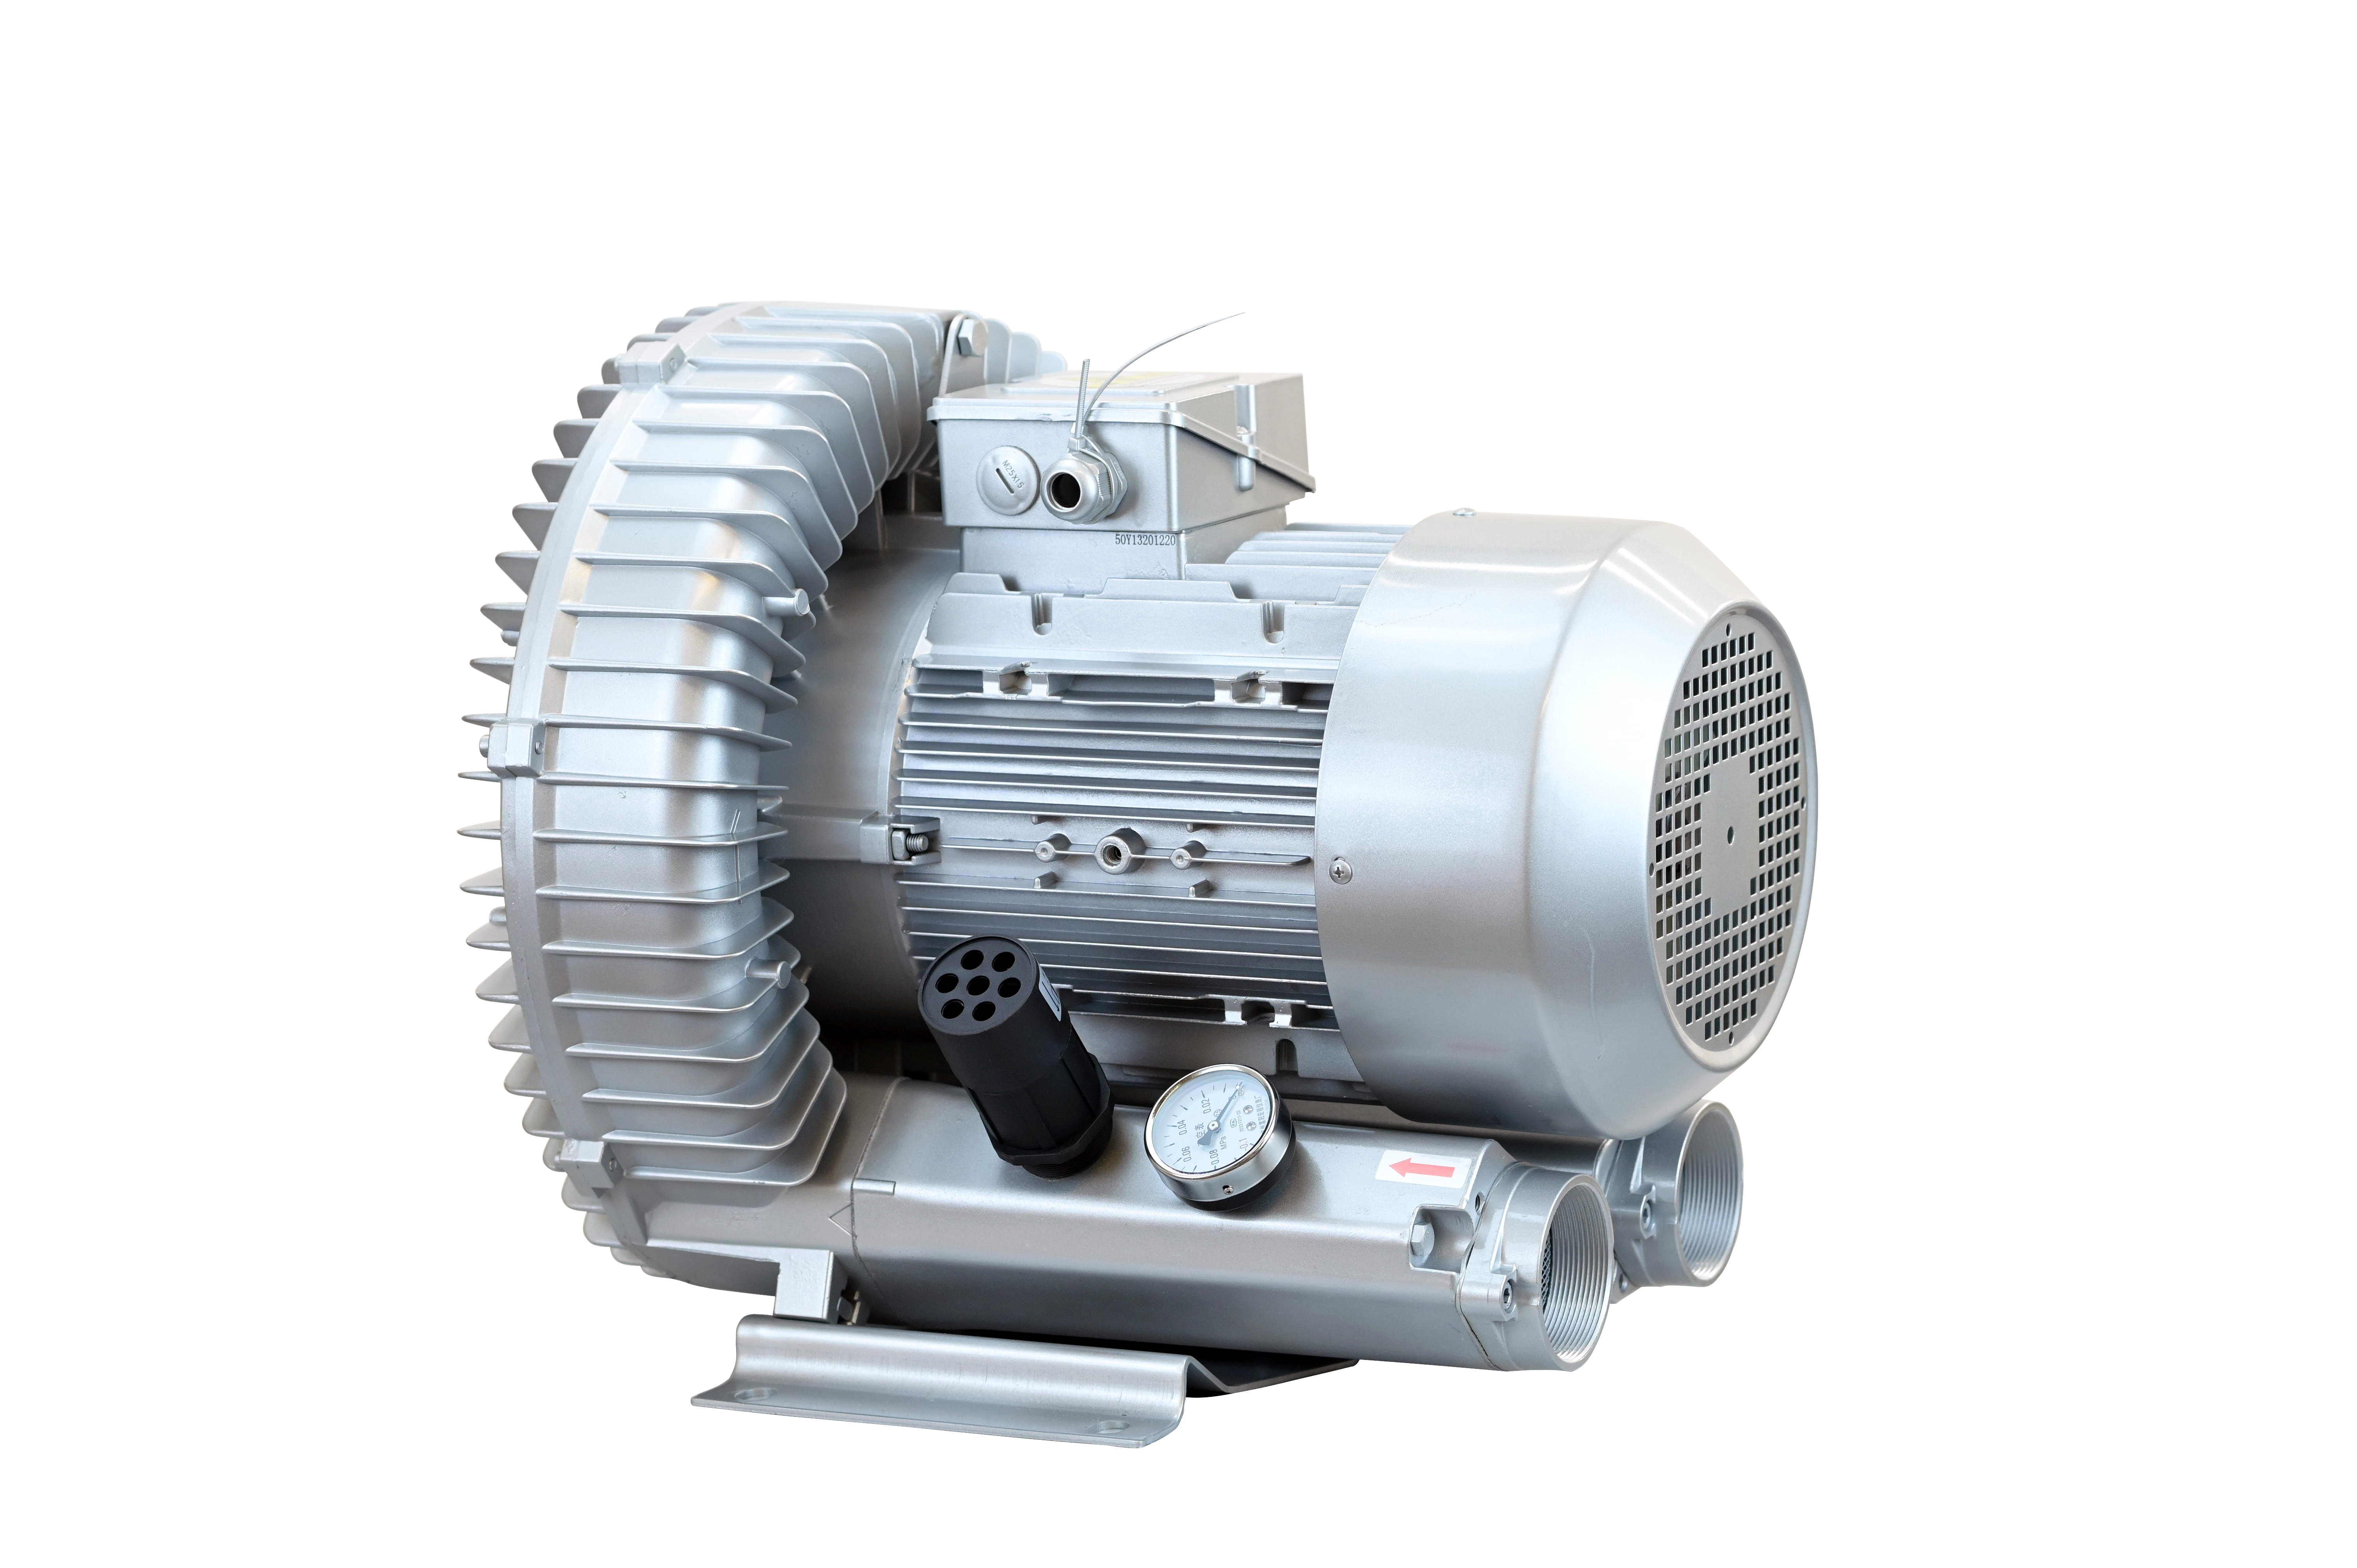
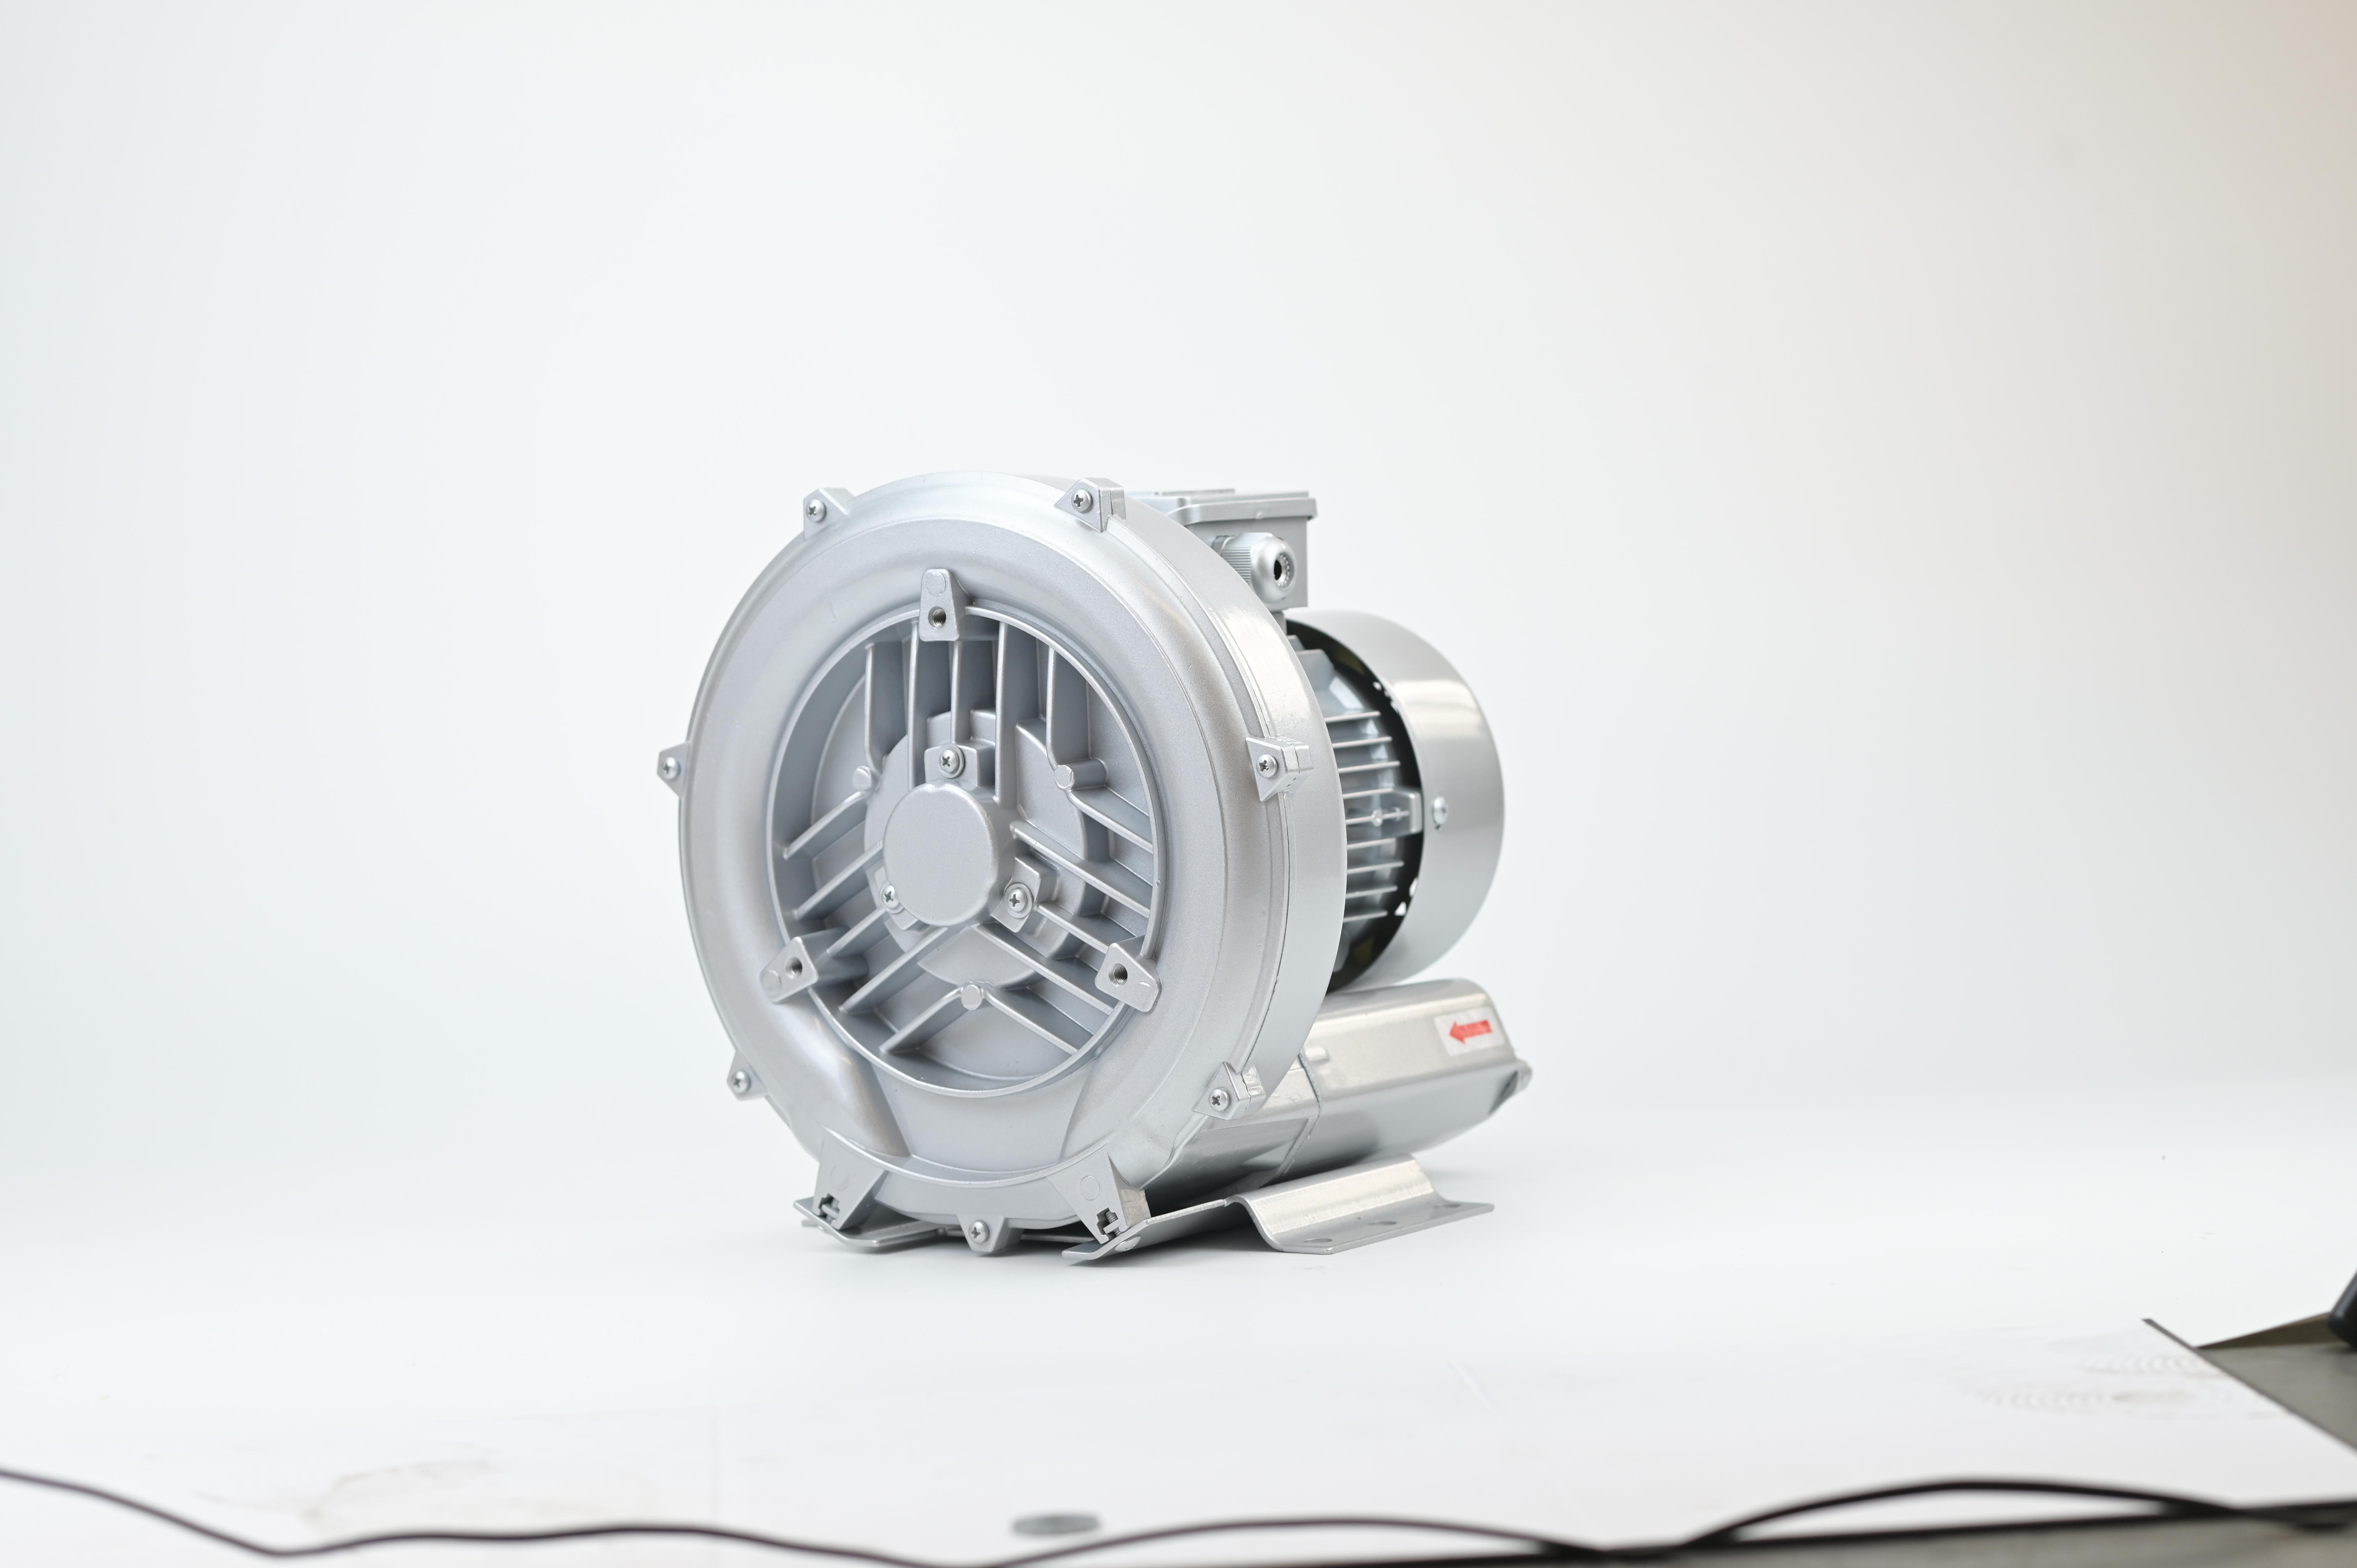
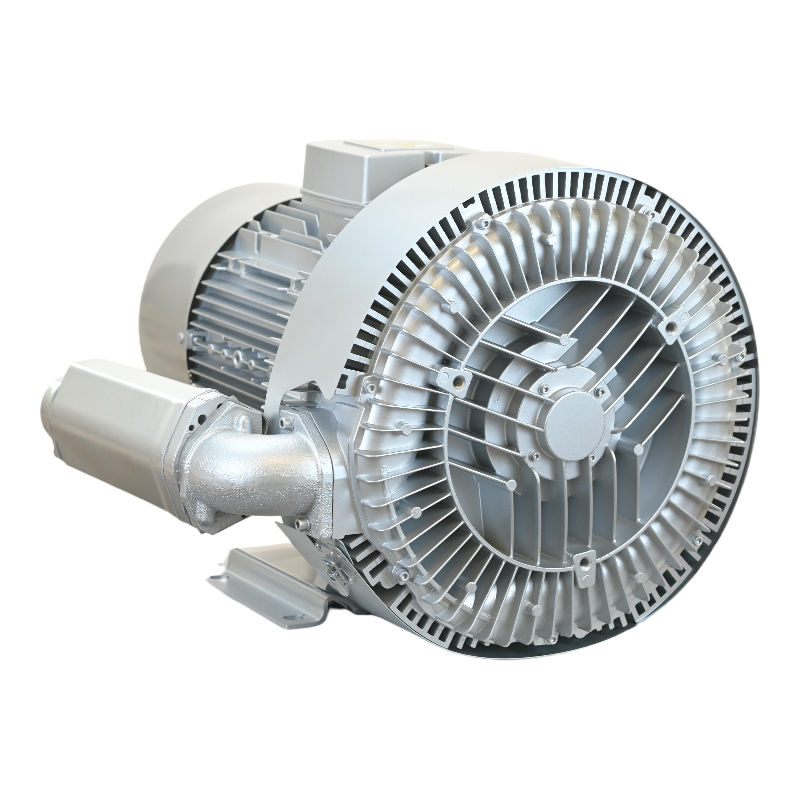
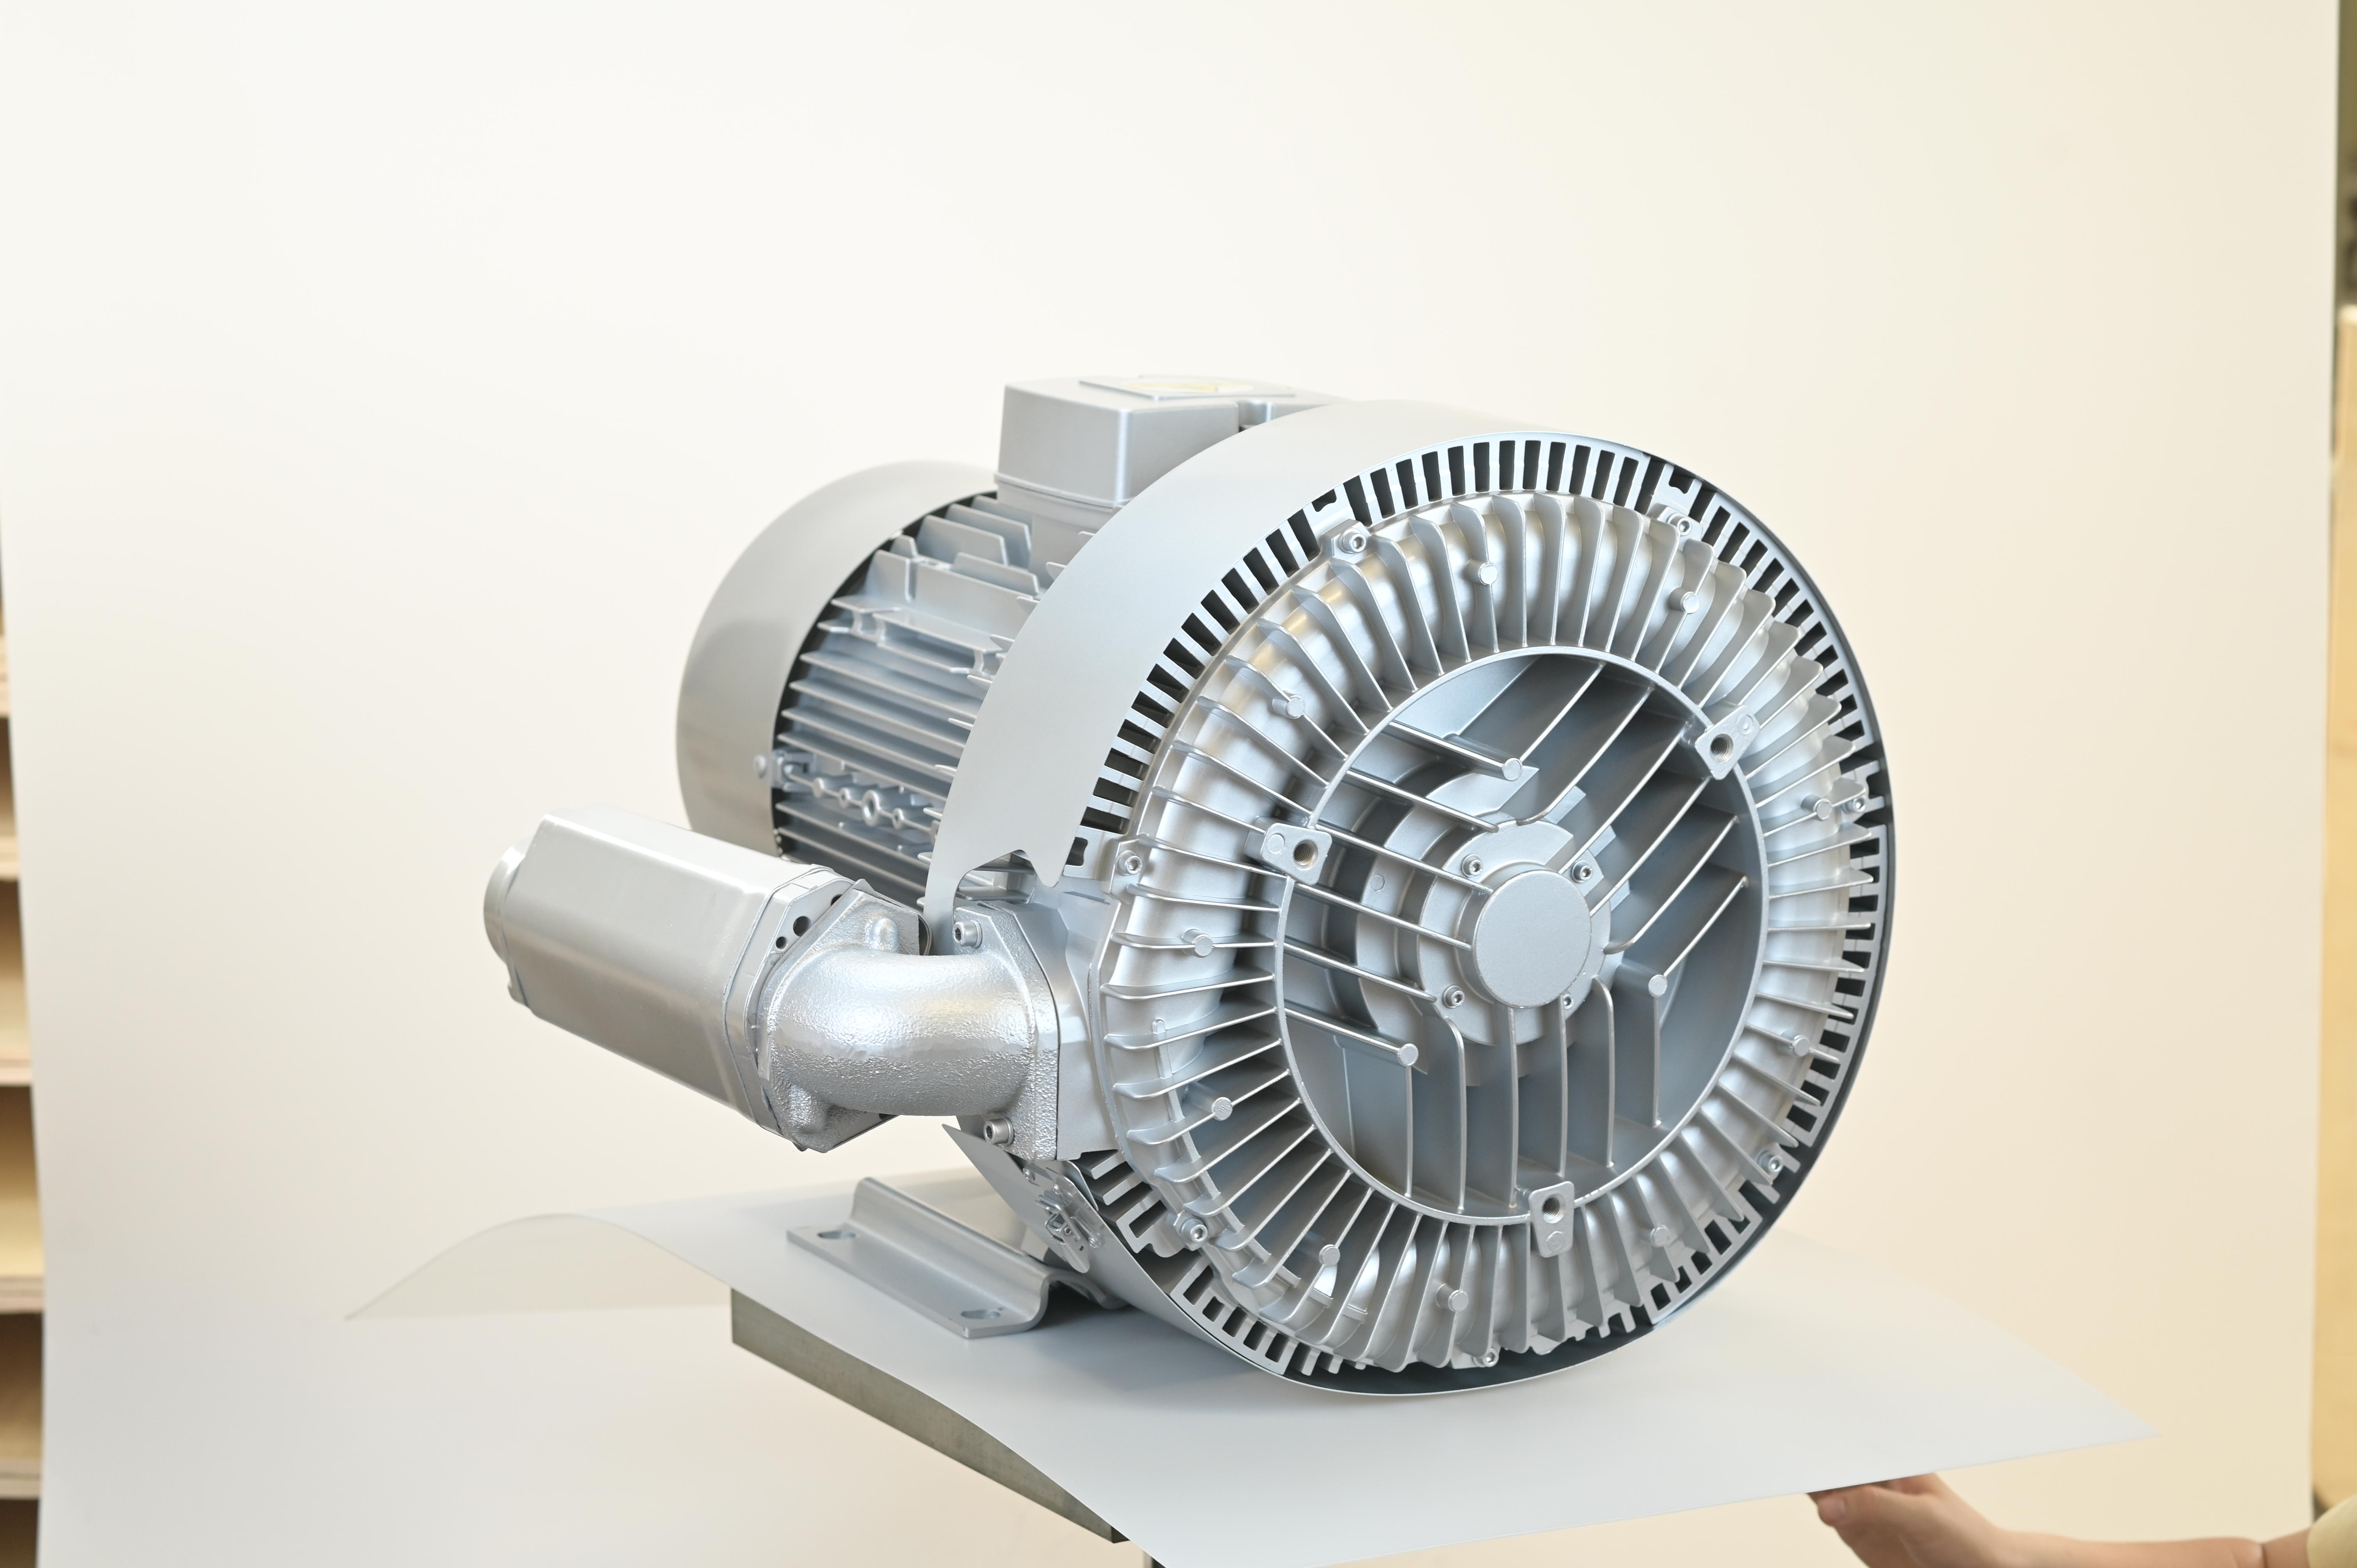
When a dairy processor in New Zealand needed to eliminate oil mist contamination in their cheese vacuum packaging line, our oil-free rotary vane vacuum pump—featuring food-grade PTFE-coated rotors​ and stainless-steel internals—delivered a stable 33 mbar ultimate vacuum​ with zero oil vapor backstreaming, helping them pass their EU GMP audit​ on the first attempt. Since 2007, Jinan Golden Bridge Precision Machinery Co., Ltd. has engineered food-grade vacuum pumps with hygienic, easy-to-clean surfaces​ and robust construction​ to minimize contamination risks in demanding environments. Unlike conventional oil-sealed units that risk hydrocarbon migration, our oil-free and water ring series​ (capable of handling moist air and steam) eliminate lubricant exposure entirely, extending maintenance intervals while ensuring the purity and quality of food products. Every unit is CE certified, assembled under ISO 9001​ controls, and backed by a global service network across Europe, North America
Get A Quote

Why Choose Our Industrial Vacuum Pumps for Food?

Hygienic Design for Food Safety

Our industrial vacuum pumps are engineered with food-grade materials and a hygienic design, ensuring compliance with stringent food safety standards. By minimizing contamination risks, our pumps help maintain the purity and quality of food products, making them essential for food processing facilities. The easy-to-clean surfaces and robust construction further enhance their suitability for the food industry.

High Efficiency and Performance

Equipped with cutting-edge technology, our industrial vacuum pumps deliver exceptional performance and energy efficiency. They operate quietly and effectively, reducing downtime and maintenance costs. With a range of models available, we can cater to various food production needs, ensuring optimal vacuum levels for packaging, drying, and other applications.

Global Certifications and Reliability

Our vacuum pumps are certified with CE and numerous patents, reflecting our commitment to quality and innovation. Trusted by clients across Europe, North America, and beyond, our products have a proven track record of reliability and performance in demanding food processing environments. We prioritize customer satisfaction and continuously seek feedback to enhance our offerings.

Related products

Construction of any sort of vacuum pumps is an important aspect of any industry. In the food business, vacuum pumps are vital during the production, packaging and processes of the food. At Jinan Golden Bridge Precision Machinery Co., Ltd., we appreciate the struggles of food manufacturers’, and we stress the importance of hygiene, efficiency, and reliability. Our food industry vacuum pumps are manufactured using certain technology to ensure our pumps perform to the best of their ability. Our pumps are designed for food processing, and we manufacture everything from high pressure food processing pumps to oil vacuum food industry pumps. We conform to the international standards to help ensure our customers get the best vacuum pumps that are food industry compliant. Our vacuum pumps help food manufacturers achieve their goal while putting less stress on them and their employees.

Frequently Asked Questions about Industrial Vacuum Pumps for Food

What are the key features of your industrial vacuum pumps for food?

Our industrial vacuum pumps for food are designed with food-grade materials, high efficiency, low noise operation, and easy maintenance features to ensure food safety and optimal performance.
Consider factors such as the type of food product, required vacuum level, and production volume. Our team can assist you in selecting the best model for your specific application.

Related article

Vortex Vacuum Pumps: Oil-Free, Energy-Efficient Solutions for Industrial Applications

24

Nov

Vortex Vacuum Pumps: Oil-Free, Energy-Efficient Solutions for Industrial Applications

Discover oil-free, 30-50% more energy-efficient vortex vacuum pumps ideal for semiconductors, medical, and food packaging. Zero contamination, low noise, global support. Request a quote today.
View More
What Are the Energy-Saving Technologies Applied in Modern Industrial Air Compressors?

22

Dec

What Are the Energy-Saving Technologies Applied in Modern Industrial Air Compressors?

Cut compressor energy costs by up to 35%—discover VSD, heat recovery, smart controls & more. Learn proven efficiency upgrades for manufacturers. Download the tech guide now.
View More
What Factors Influence the Energy Efficiency of Air Blowers in Industrial Settings?

13

Mar

What Factors Influence the Energy Efficiency of Air Blowers in Industrial Settings?

What really drives energy waste in industrial air blowers? Discover 7 key technical & operational factors—and cut energy costs by up to 40%. Download the efficiency checklist now.
View More
Why Do Industrial Air Compressors Require Regular Air Filter Replacement?

25

Dec

Why Do Industrial Air Compressors Require Regular Air Filter Replacement?

Neglecting air filter replacement risks downtime, energy waste, and costly repairs. Learn how regular maintenance boosts efficiency & extends compressor life—download our maintenance checklist now.
View More

Customer Testimonials about Our Industrial Vacuum Pumps for Food

John Smith
Reliable Performance in Our Food Factory

The industrial vacuum pumps from Jinan Golden Bridge have transformed our packaging process. Their reliability and efficiency have significantly reduced our downtime, and we are very satisfied with the results.

Emily Johnson
High-Quality and Safe Solutions

We appreciate the attention to hygiene and safety in the design of these vacuum pumps. They have become an integral part of our food processing line, ensuring the quality of our products.

Get a Quote & Connect With Our Engineering Team

Searching for reliable industrial solutions? Let us help you find the perfect fit. Drop us a line, and our B2B technical sales team will get back to you within 12 hours (working days).
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000
Cutting-Edge Technology for Enhanced Efficiency

Cutting-Edge Technology for Enhanced Efficiency

When a meat processing plant in Germany needed to cut energy costs without compromising the 99.9% vacuum consistency​ required for their modified atmosphere packaging (MAP) line, our oil-free rotary vane vacuum pump—featuring permanent magnet variable speed drive (PM VSD)​ and IE4 premium-efficiency motors—automatically adjusted motor speed 240 times per second​ to match real-time gas load, eliminating idle waste and cutting energy consumption by 35%​ while maintaining 33 mbar ultimate vacuum. Unlike conventional fixed-speed pumps that consume full power regardless of demand, our direct-drive design​ with highly wear-resistant graphite vanes​ and food-grade PTFE-coated internals​ eliminates oil disposal entirely, preventing 200+ liters of hazardous waste annually​ and supporting EU GMP compliance. Every unit is CE certified, assembled under ISO 9001​ controls, and tested to ISO 21360-1​ standards, with compliance to EU EcoDesign 2021​ regulations.
Robust Construction for Longevity

Robust Construction for Longevity

When a dairy processor in New Zealand needed to eliminate oil mist contamination in their cheese vacuum packaging line, our oil-free rotary vane vacuum pump—featuring food-grade PTFE-coated rotors​ and stainless-steel internals—delivered a stable 33 mbar ultimate vacuum​ with zero oil vapor backstreaming, helping them pass their EU GMP audit​ on the first attempt. Unlike conventional oil-sealed units that require fluid changes every 2,000 hours and risk hydrocarbon migration into food products, our highly wear-resistant graphite vanes​ and corrosion-proof construction​ extend maintenance intervals to 25,000 hours—slashing annual service costs by 68%. Every unit is CE certified, assembled under ISO 9001​ controls, and backed by a global service network across Europe, North America, and Australia​ offering 24/7 remote monitoring​ and 48-hour critical parts delivery.
+86 0531 88060599
13386448931
[email protected]

Get a Quote & Connect With Our Engineering Team

Searching for reliable industrial solutions? Let us help you find the perfect fit. Drop us a line, and our B2B technical sales team will get back to you within 12 hours (working days).
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000